Camellia seed powder conveying is a critical process in the processing industry, particularly for enterprises involved in the extraction and utilization of camellia seed oil. The efficient and stable transportation of camellia seed powder directly impacts production efficiency, product quality, and operational safety. This article aims to explore the fundamental principles of camellia seed powder conveying and analyze the key characteristics of different working scenes, providing a comprehensive understanding for relevant professionals.
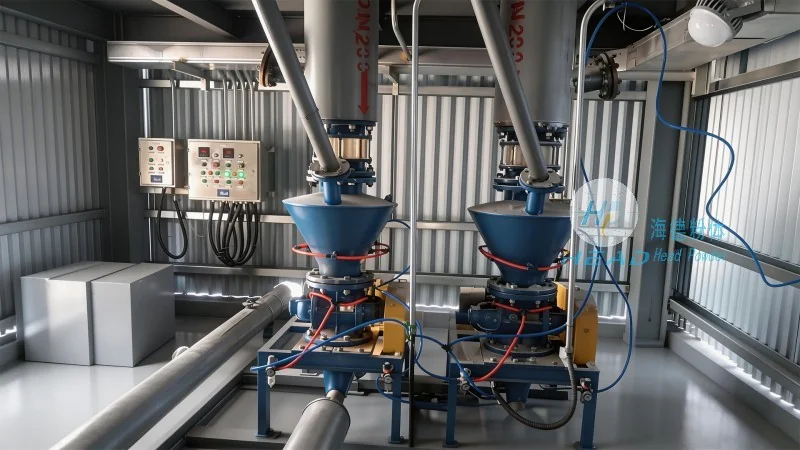
Principles of Camellia Seed Powder Conveying
The core principle of camellia seed powder conveying is to transport the fine powder material from the source to the target location through mechanical or pneumatic means. For camellia seed powder, which is typically fine and has certain fluidity characteristics, the selection of conveying equipment and system design is crucial. Common conveying methods include pneumatic conveying (such as pressure and vacuum systems) and mechanical conveying (such as screw conveyors, belt conveyors, and bucket elevators). The choice of method depends on factors like the particle size distribution, moisture content, and the required conveying distance and capacity. Pneumatic conveying is often preferred for fine powders due to its ability to handle dust and maintain a clean environment, while mechanical conveying is suitable for larger particles or when a closed system is not feasible.
Key Working Scene Characteristics
The working scene characteristics of camellia seed powder conveying vary significantly based on the production environment and operational requirements. In the processing plant of Shandong HeadPowder Engineering Co., Ltd., for instance, the conveying system is designed to handle large volumes of camellia seed powder from raw material storage to the oil extraction unit. The key characteristics in this scenario include high conveying capacity, stable flow control, and minimal material loss. The system is equipped with advanced sensors and control systems to monitor the powder flow and adjust the conveying parameters in real-time, ensuring consistent performance under varying production loads.
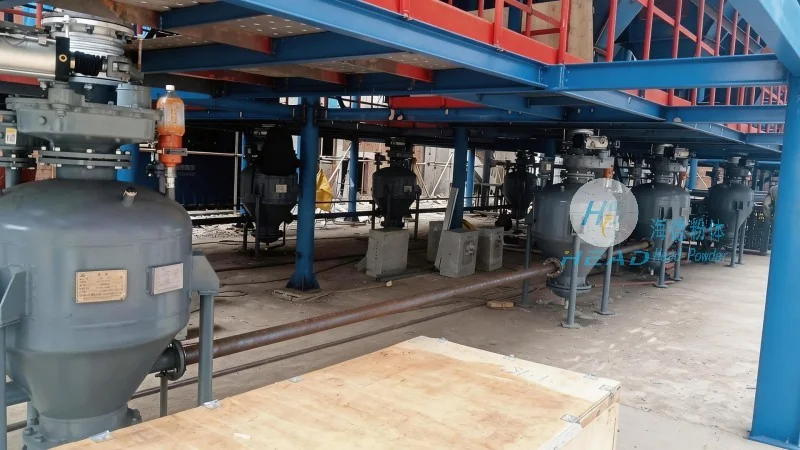
Application in Different Production Stages
Camellia seed powder conveying is applied across multiple stages of the processing line. In the raw material handling stage, the powder is conveyed from storage silos to the grinding or pre-treatment equipment. The conveying system must be able to handle the bulk material and maintain a uniform flow to prevent clogging or uneven processing. During the oil extraction stage, the powder is conveyed to the extraction tanks or centrifuges, where the oil is separated from the solid residue. The conveying method in this stage often involves low-pressure pneumatic systems to avoid damaging the oil particles or introducing air bubbles that could affect the extraction efficiency. In the final product packaging stage, the powder is conveyed to the packaging machines, requiring precise control of the flow rate to ensure accurate filling and avoid spillage.
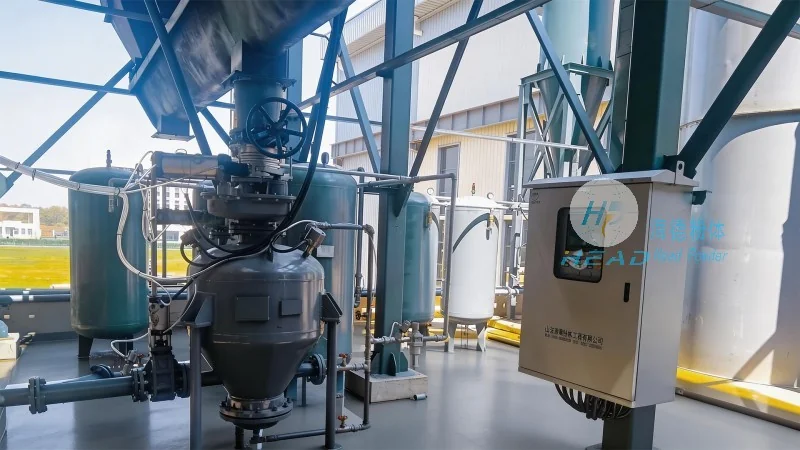
Advantages and Challenges in Conveying Camellia Seed Powder
Conveying camellia seed powder offers several advantages, including the ability to maintain a closed system, reducing dust pollution and improving workplace safety. It also allows for better control over the material's temperature and moisture content, which are critical factors in oil extraction processes. However, the process also presents challenges, such as the tendency of fine powders to agglomerate or form blockages in the conveying system. This can lead to reduced efficiency and increased maintenance costs. Additionally, the high dust content of camellia seed powder requires effective dust collection and filtration systems to comply with environmental regulations and protect equipment from corrosion.
Case Study: Conveying System at Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of powder processing equipment, has implemented a state-of-the-art camellia seed powder conveying system in its production facility. The system integrates a combination of pneumatic and mechanical conveying components, tailored to the specific needs of the company's production line. The system features a large-capacity storage silo, equipped with a rotary valve for controlled discharge, followed by a pressure pneumatic conveying line that transports the powder to the oil extraction unit. The conveying line is equipped with pressure sensors and flow meters to monitor the system's performance and adjust the air pressure and flow rate as needed. The company has reported significant improvements in production efficiency and product quality after implementing this system, with reduced downtime and lower material loss.




