Understanding the principles and application scenarios of potassium carbonate powder handling and transportation is crucial for industries that rely on this chemical compound. Potassium carbonate, a white crystalline powder, is widely used in various sectors including glass manufacturing, food processing, and chemical production. Efficient and safe transportation of this powder is essential to maintain product quality and operational efficiency.
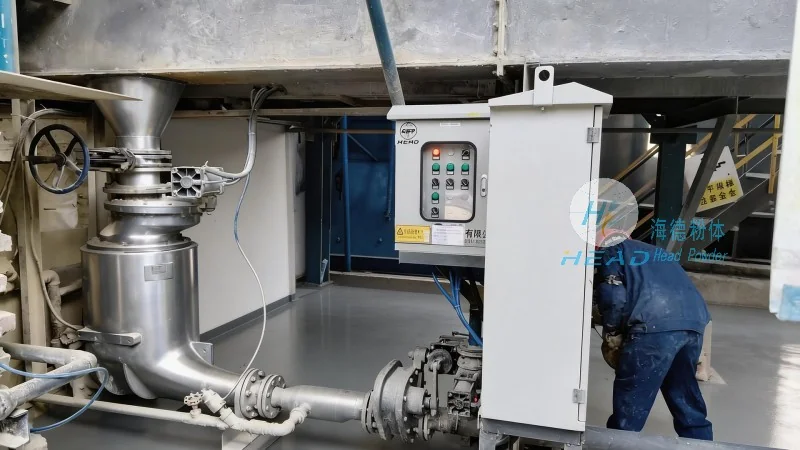
Company Introduction: HeadPowder
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading provider of specialized equipment and solutions for powder handling and transportation. With a strong presence in China, particularly in Shandong, the company has established itself as a trusted partner for businesses seeking reliable and effective solutions for handling potassium carbonate and other fine powders. HeadPowder's expertise lies in designing and manufacturing systems that ensure safe, efficient, and cost-effective powder transport, catering to the diverse needs of industrial applications.
The Principles of Potassium Carbonate Powder Transportation
The transportation of potassium carbonate powder involves several key principles aimed at ensuring product integrity and operational safety. One of the primary principles is the use of enclosed systems to prevent dust dispersion and contamination. This is achieved through the implementation of dust-tight pipelines, rotary valves, and pneumatic conveying systems that minimize the risk of airborne particles. Additionally, the design of the transportation system considers the material's physical properties, such as its flowability and tendency to agglomerate, to optimize the conveying process. Proper ventilation and filtration systems are also integral to maintaining a clean and safe working environment, especially in facilities where the powder is handled in large quantities.
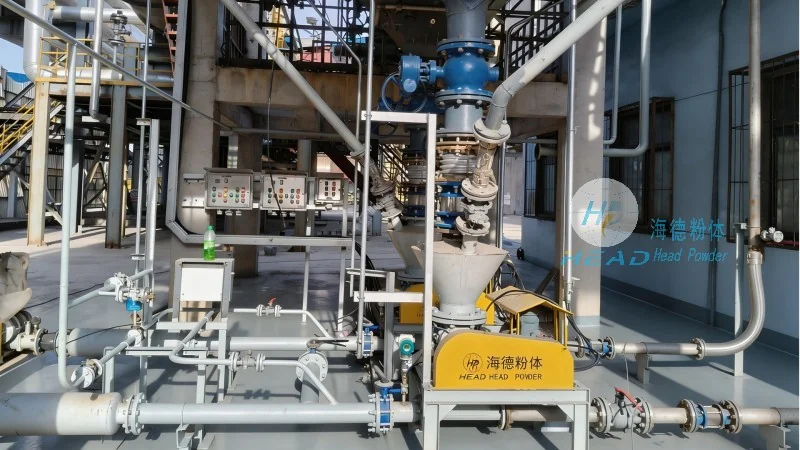
Key Components in Potassium Carbonate Powder Handling Systems
Effective potassium carbonate powder transportation relies on a combination of specialized components that work in harmony to ensure smooth operation. The system typically includes a hopper for material storage, which is designed to prevent material bridging and ensure consistent feed. A rotary valve or feeder is used to control the flow rate of the powder from the hopper into the conveying line. The conveying method, whether pneumatic or mechanical, is selected based on the specific requirements of the application, such as the distance to be covered and the volume of material to be transported. For pneumatic systems, air compressors and filters are essential to maintain the pressure and purity of the conveying air. In mechanical systems, screw conveyors or belt conveyors are used to move the powder through the system. Each component is carefully selected and integrated to ensure that the powder is transported without degradation, maintaining its quality and properties throughout the process.
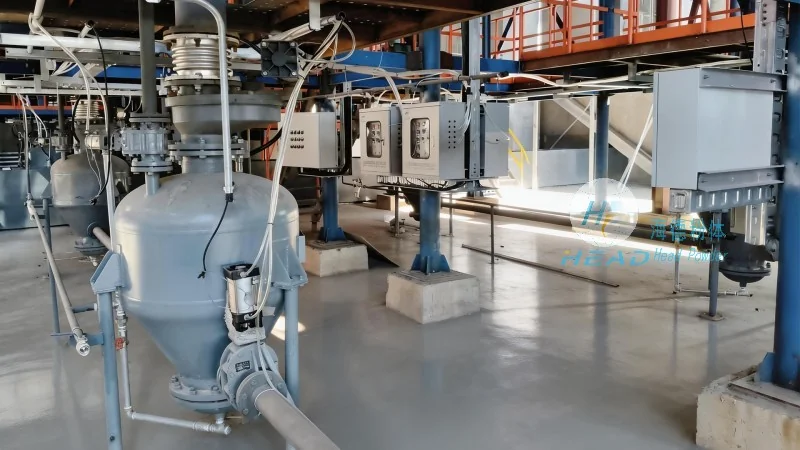
Application Scenarios and Operational Characteristics
The application scenarios for potassium carbonate powder transportation vary widely, depending on the industry and the specific use case. In glass manufacturing, for example, potassium carbonate is used as a flux to lower the melting point of silica, and the transportation system must be capable of handling large volumes of the powder while maintaining a high degree of purity. The system must also be designed to withstand the high temperatures and chemical exposure associated with glass production. In food processing, the powder is used as a food additive, and the transportation system must adhere to strict hygiene standards to prevent contamination. This includes the use of stainless steel components, regular cleaning procedures, and air filtration systems to ensure that the powder remains free from contaminants. In chemical production, the powder may be used as a raw material in various chemical reactions, and the transportation system must be able to handle the material's reactivity and ensure safe handling. The operational characteristics of the system, such as the flow rate, pressure, and temperature, are carefully controlled to optimize the performance and safety of the process.
Advantages of HeadPowder's Powder Handling Solutions
HeadPowder's solutions for potassium carbonate powder transportation offer several advantages that make them ideal for industrial applications. The company's systems are designed to be highly efficient, with minimal energy consumption and low maintenance requirements. The enclosed design of the systems ensures that the powder is handled safely, reducing the risk of dust explosions and other hazards. The use of high-quality materials, such as stainless steel and corrosion-resistant components, ensures the longevity and reliability of the equipment. Additionally, HeadPowder provides customized solutions tailored to the specific needs of each client, ensuring that the system is optimized for their particular application. The company's expertise in powder technology allows them to offer comprehensive support, including design, installation, and maintenance services, to ensure that the system operates at peak performance.




