Stone and coal powder conveying equipment is a critical component in various industrial processes, designed to efficiently transport bulk materials like stone aggregates and coal powders from one location to another. The equipment plays a vital role in optimizing material handling operations, ensuring smooth workflow, and enhancing overall productivity in industrial settings. This article delves into the fundamental principles of such equipment and highlights the key characteristics of its working scenarios, providing insights into how these systems operate and where they are most effectively applied.
Working Principle of the Conveying System
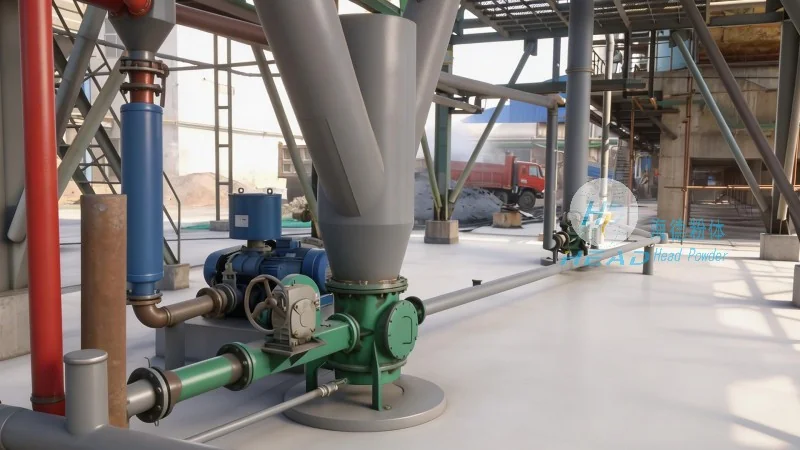
The core mechanism of stone and coal powder conveying equipment typically involves a combination of mechanical and pneumatic components. For instance, many systems utilize a positive displacement blower or a vacuum pump to generate airflow, which then carries the particulate materials through a pipeline. The design of the conveying system is tailored to handle the specific properties of stone and coal powders, such as particle size, density, and moisture content. The equipment often includes a hopper for material storage, a feeder to control the flow rate, and a pipeline network that may incorporate bends, elbows, and filters to ensure efficient and unobstructed transport. The working principle emphasizes the balance between air velocity and material velocity to prevent clogging and maintain consistent material flow. This approach allows for reliable and continuous operation, even with varying material characteristics.
Key Features and Technical Specifications
Headpowder, a leading manufacturer of industrial conveying solutions, offers advanced stone and coal powder conveying equipment that meets the demands of modern industrial applications. The systems are engineered with high-quality materials, ensuring durability and long-term performance. Key technical specifications include adjustable airflow rates, variable speed drives for precise control, and robust filtration systems to maintain air quality and prevent dust contamination. The equipment is designed to handle a wide range of particle sizes, from fine coal powders to larger stone aggregates, making it versatile for diverse industrial needs. Additionally, the systems incorporate safety features such as pressure relief valves and overload protection to ensure safe operation under all conditions. The integration of advanced control systems allows for real-time monitoring and adjustment of the conveying process, enhancing operational efficiency and reducing downtime.
Common Working Scene Applications
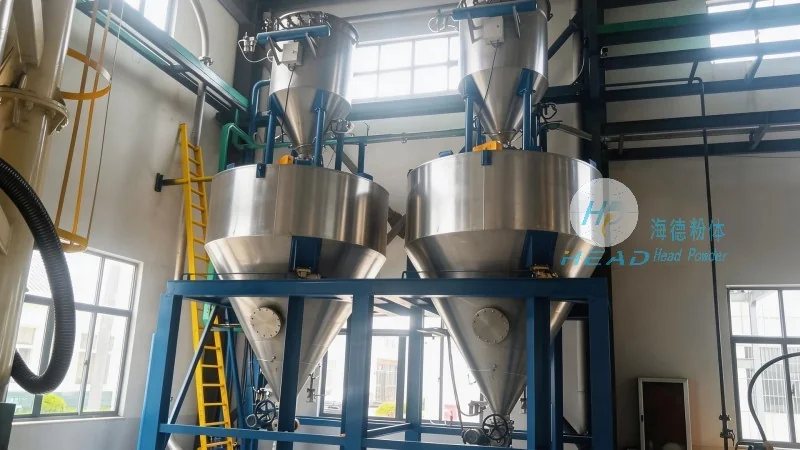
The working scenarios of stone and coal powder conveying equipment are widespread across multiple industries. In the power generation sector, these systems are essential for transporting coal from storage facilities to boilers, ensuring a steady supply of fuel for electricity production. In the cement and concrete industries, the equipment is used to convey raw materials like limestone and coal ash, facilitating the production of cement and other building materials. The manufacturing of chemicals and pharmaceuticals also relies on such equipment to transport coal-based raw materials or stone-based additives, supporting the production of various chemical products. Furthermore, in the mining and quarrying industries, the equipment is utilized to move stone aggregates from processing sites to storage or transportation points, streamlining the material handling process. Each application requires tailored equipment configurations to address the specific challenges of the working environment, such as material variability, space constraints, and environmental regulations.
Advantages in Industrial Operations
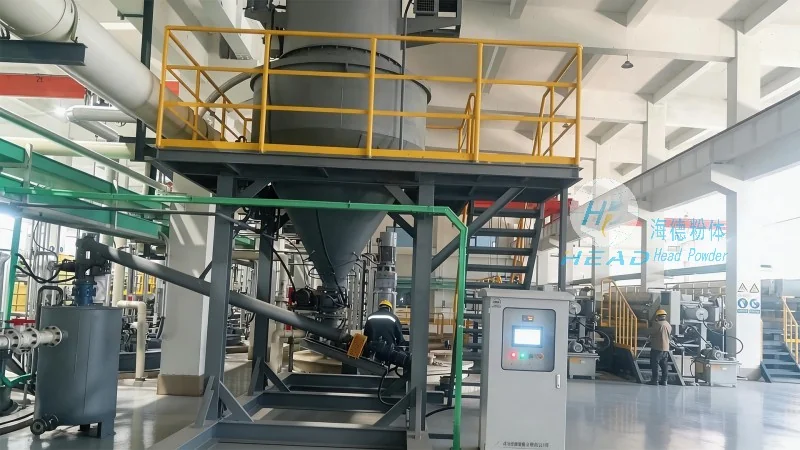
Implementing stone and coal powder conveying equipment brings several advantages to industrial operations. Firstly, it significantly reduces labor costs by automating the material handling process, eliminating the need for manual transport and reducing the risk of human error. Secondly, the equipment enhances safety by minimizing exposure to dust and reducing the physical strain on workers. Thirdly, the systems improve operational efficiency by providing consistent and continuous material flow, which helps maintain production schedules and reduce bottlenecks. Additionally, the advanced control systems allow for precise monitoring and adjustment, enabling operators to optimize the conveying process based on real-time data. This leads to better resource utilization and cost savings over time. The equipment also contributes to environmental compliance by incorporating filtration systems that capture dust and prevent air pollution, aligning with regulatory requirements and promoting sustainable industrial practices.
Conclusion and Company Overview
Stone and coal powder conveying equipment, as exemplified by the solutions offered by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated and essential technology in modern industrial material handling. The equipment’s working principles, technical features, and application scenarios are designed to meet the diverse needs of various industries, ensuring efficient, safe, and reliable material transport. By leveraging advanced engineering and quality materials, Headpowder provides systems that enhance productivity, reduce costs, and support sustainable industrial operations. The company’s commitment to innovation and customer satisfaction positions it as a trusted partner for businesses seeking to optimize their material handling processes. With its headquarters in Shandong, China, Headpowder continues to lead the development of efficient conveying solutions for the global industrial market.




