HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced powder handling systems. Among their offerings is the nitrogen-protected powder conveying system, a critical solution for industries dealing with sensitive or hazardous powders. This article explores the fundamental principles behind such systems and highlights the key working scene characteristics that make them indispensable in modern industrial applications.
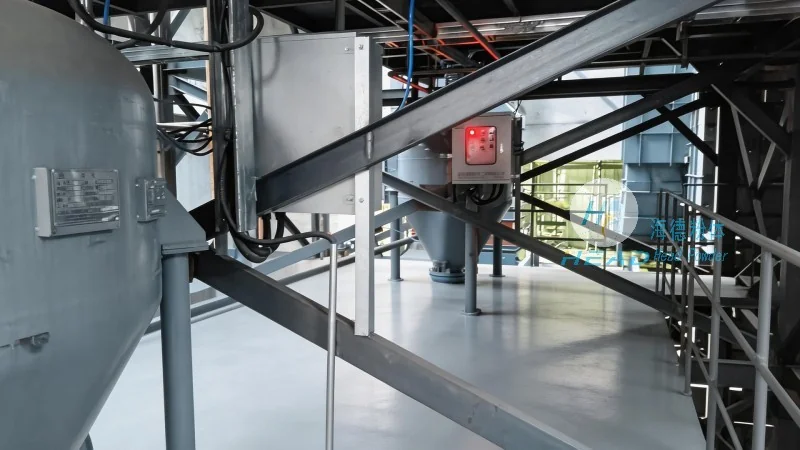
Understanding the Core Principle of Nitrogen-Protected Powder Handling Systems
The primary objective of a nitrogen-protected powder handling system is to maintain an inert gas environment throughout the material flow. By replacing or displacing ambient air with nitrogen, the system creates a barrier that prevents oxidation, moisture absorption, and other chemical reactions that could compromise the quality or safety of the powder. This is particularly crucial for materials that are prone to self-ignition or that require strict contamination control, such as pharmaceuticals, fine chemicals, and food additives. The system typically includes nitrogen generation units, gas distribution networks, and sealed conveying components that ensure the entire process remains under a controlled nitrogen atmosphere.
Key Working Scene Characteristics and Applications
HeadPowder's nitrogen-protected systems are tailored to diverse industrial scenarios, each with specific requirements for safety, efficiency, and material integrity. For instance, in pharmaceutical manufacturing, where product purity is paramount, the system ensures that powders remain free from microbial contamination and moisture, which could affect drug efficacy. In the chemical industry, especially for flammable or explosive powders like sulfur or metal powders, the nitrogen environment eliminates the risk of fire or explosion during transport. The systems are also widely used in food processing, where maintaining the freshness and nutritional value of ingredients is essential. Each application leverages the system's ability to control the gas environment, thereby optimizing both operational safety and product quality.
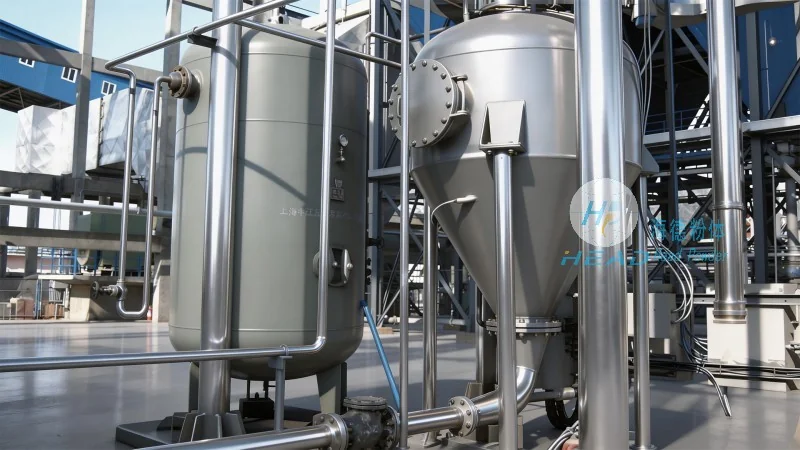
Technical Advantages and Operational Benefits
Implementing a nitrogen-protected powder handling system offers several technical advantages that enhance overall process performance. First, it significantly reduces the risk of dust explosions by eliminating oxygen from the conveying line. This is achieved through continuous nitrogen flow, which maintains a negative pressure or inert gas pressure within the system, preventing the ingress of ambient air. Second, the system improves material flow characteristics by preventing agglomeration and caking, which can occur when powders are exposed to moisture or air. This leads to more consistent and reliable conveying rates, reducing downtime and maintenance costs. Additionally, the sealed design of the system minimizes material loss and cross-contamination, which is critical in industries with strict regulatory compliance, such as pharmaceuticals and food.
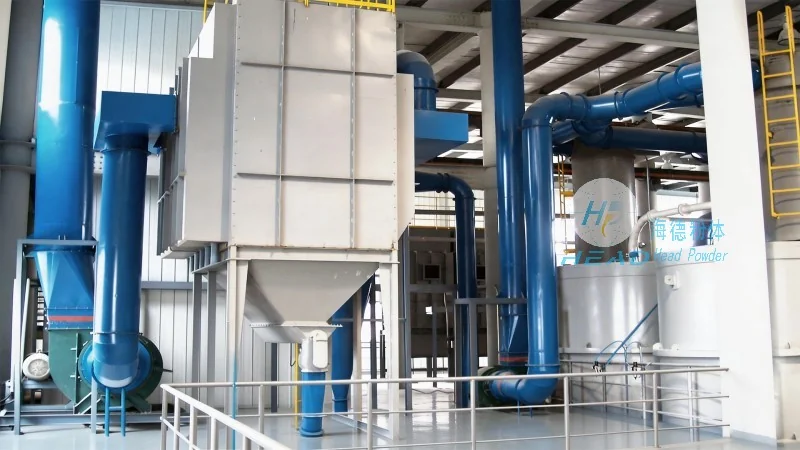
Customization and Scalability for Diverse Needs
HeadPowder recognizes that no two industrial processes are identical, and thus, their nitrogen-protected powder handling systems are highly customizable. The company works closely with clients to understand their specific material properties, flow rates, and environmental constraints, then designs a system that meets those requirements. Whether for small-scale laboratory applications or large-scale industrial production lines, the systems can be scaled to accommodate varying throughput demands. The modular design allows for easy integration with existing infrastructure, minimizing installation time and disruption to operations. This flexibility ensures that clients receive a solution that is both effective and cost-efficient, tailored to their unique operational needs.
Conclusion: The Role of Nitrogen-Protected Systems in Modern Manufacturing
In conclusion, the nitrogen-protected powder handling system developed by HeadPowder represents a sophisticated solution to the challenges of safe and efficient powder transport. By leveraging the principles of inert gas protection, the system addresses critical issues such as oxidation, moisture absorption, and fire hazards, while maintaining material integrity and process efficiency. With applications spanning pharmaceuticals, chemicals, and food industries, these systems are becoming increasingly vital as industries strive for higher standards of safety and quality. HeadPowder's expertise in engineering and customization ensures that clients can rely on these systems to meet their operational goals, contributing to a safer and more productive manufacturing environment.




