HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced high-pressure pulse powder conveying systems. These systems are engineered to efficiently transport bulk powders over long distances with minimal maintenance and high reliability. The company's products are widely used in various industrial sectors, including chemical, pharmaceutical, food processing, and mining, where precise and consistent powder handling is critical.
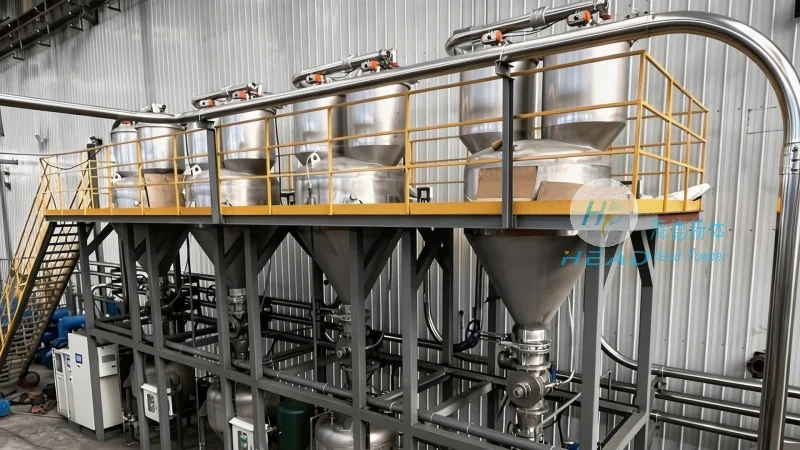
Introduction to High-Pressure Pulse Powder Conveying Systems
High-pressure pulse powder conveying systems represent a sophisticated approach to bulk material handling, leveraging compressed air or other gases to create high-velocity pulses that propel powders through pipelines. Unlike traditional screw or belt conveyors, these systems are particularly effective for transporting fine or abrasive powders that are prone to caking or segregation. The core technology involves a series of pulses generated by a control unit, which alternates between high and low pressure to create a dynamic flow of material.
Principle of Operation
The fundamental principle of the high-pressure pulse powder conveying system is based on the Venturi effect and the Bernoulli principle. When a high-pressure pulse is introduced into the pipeline, it creates a low-pressure zone that draws the powder particles into the flow. The system typically consists of a hopper, a pulse generator, a pipeline network, and a receiver. The hopper stores the powder, while the pulse generator produces the controlled pressure pulses. The pipeline transports the material from the hopper to the receiver, where it is collected. The system's efficiency is enhanced by the use of a filter or separator to prevent dust from entering the pipeline and to maintain air quality.
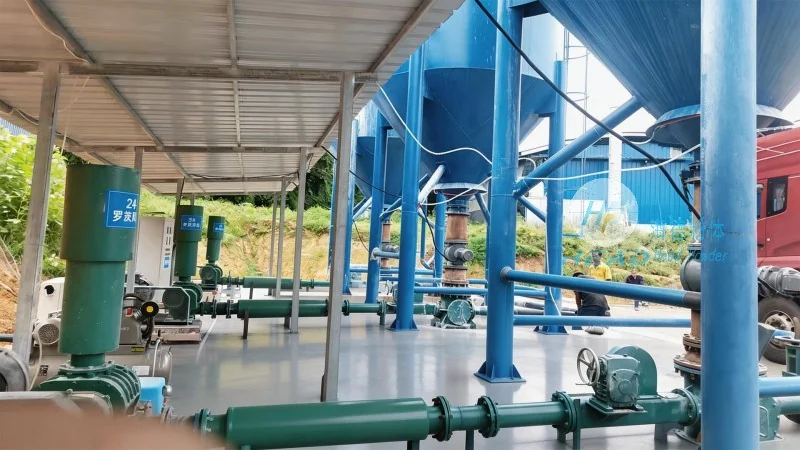
Key Working Scene Characteristics
High-pressure pulse powder conveying systems are deployed in diverse industrial environments, each with unique requirements that the technology addresses effectively. In chemical plants, for example, these systems are used to transport reactive powders or those that require strict contamination control. The systems' ability to maintain a consistent flow and prevent material degradation makes them ideal for pharmaceutical applications, where product purity is paramount. In food processing facilities, the systems are designed to handle powders such as flour, sugar, or spices, ensuring hygienic and efficient transfer without cross-contamination. Mining operations also benefit from these systems, as they can handle abrasive and heavy-duty powders like ore or coal, reducing the need for manual handling and improving safety.
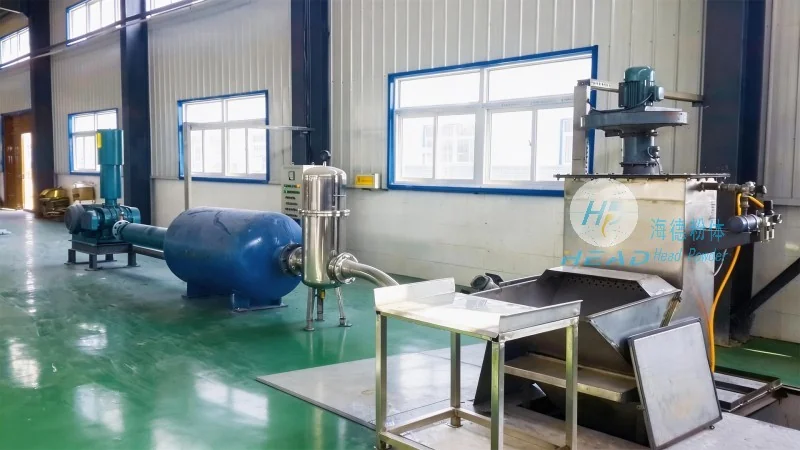
Advantages and Technical Features
One of the primary advantages of high-pressure pulse powder conveying systems is their ability to transport powders over long distances with minimal energy consumption. The systems are also highly flexible, as they can be adapted to different pipeline configurations and material types. Additionally, the technology reduces wear and tear on equipment compared to traditional conveyors, leading to lower maintenance costs and longer service life. The use of compressed air as the driving force also allows for easy integration with existing plant infrastructure, making it a cost-effective solution for many industrial applications.
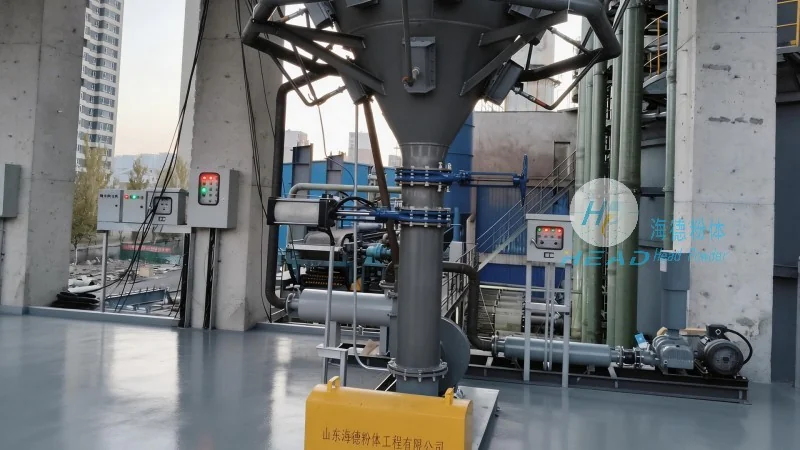
Application Examples and Case Studies
Real-world applications of high-pressure pulse powder conveying systems demonstrate their versatility and reliability. In a chemical manufacturing plant, the system was used to transport a fine, reactive powder from a storage silo to a processing unit over a distance of 500 meters. The system maintained a consistent flow rate of 10 tons per hour, with minimal pressure loss, ensuring that the production process ran smoothly without interruptions. In a pharmaceutical facility, the system was implemented to transfer a sterile powder into a filling machine, where the hygienic design and low-dust operation of the system prevented contamination and ensured product quality. These examples highlight the system's effectiveness in critical industrial environments where precision and reliability are non-negotiable.
Conclusion
High-pressure pulse powder conveying systems, as offered by Shandong HeadPowder Engineering Co., Ltd., represent a cutting-edge solution for bulk powder handling. By combining advanced control technology with efficient material transport mechanisms, these systems provide industries with a reliable, cost-effective, and environmentally friendly method of handling powders. The systems' adaptability to various applications and their ability to maintain product quality make them an essential component in modern industrial operations. As demand for efficient and sustainable material handling solutions grows, high-pressure pulse conveying systems will continue to play a vital role in meeting the needs of diverse industrial sectors.




