Automatic weighing powder pneumatic conveying equipment is a critical piece of industrial machinery designed to efficiently transport bulk powders while ensuring precise weight measurement. This equipment integrates pneumatic conveying technology with advanced weighing systems, making it indispensable in various industries such as pharmaceuticals, food processing, and chemical manufacturing. The seamless operation of this device not only enhances production efficiency but also guarantees the accuracy of material handling, which is crucial for maintaining product quality and regulatory compliance.
Key Components and Their Functions
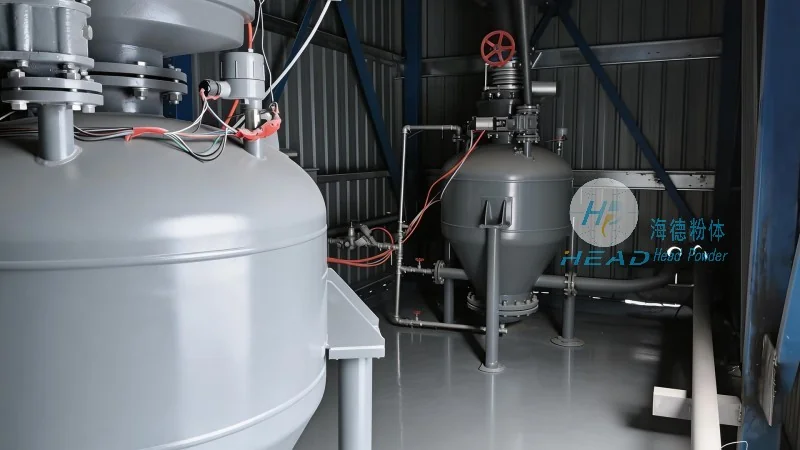
The automatic weighing powder pneumatic conveying system typically consists of several core components, each playing a vital role in the overall functionality. These components include the material hopper, air compressor, conveying pipeline, dust filter, and the integrated weighing scale. The material hopper serves as the storage container for the bulk powder, ensuring a steady supply of material to the system. The air compressor generates the necessary pressure to create a flow of air within the conveying pipeline, which transports the powder particles from the hopper to the discharge point. The conveying pipeline is designed with smooth, airtight connections to minimize material loss and ensure efficient transport. The dust filter is essential for maintaining air quality and preventing dust accumulation, which can affect the performance of the equipment and pose health hazards. The integrated weighing scale, often equipped with load cells, provides real-time weight measurement of the material being conveyed, enabling precise control over the process.
Operation Process of the Equipment
The operation of the automatic weighing powder pneumatic conveying equipment follows a systematic sequence of steps to ensure smooth and accurate material handling. Initially, the bulk powder is loaded into the material hopper. The system then activates the air compressor, which generates compressed air to create a pressure differential within the conveying pipeline. As the air flows through the pipeline, it entrains the powder particles, forming a dense phase flow that is efficiently transported to the discharge point. Simultaneously, the weighing scale continuously monitors the weight of the material being conveyed, providing real-time data to the control system. The control system uses this data to adjust the air flow rate and pressure as needed, maintaining a consistent and accurate weight of the material being transported. The discharge point, typically a valve or a hopper, releases the material at the desired location, completing the conveying cycle. The entire process is automated, with minimal human intervention required, which reduces operational errors and enhances productivity.
Working Principle of the Pneumatic Conveying System
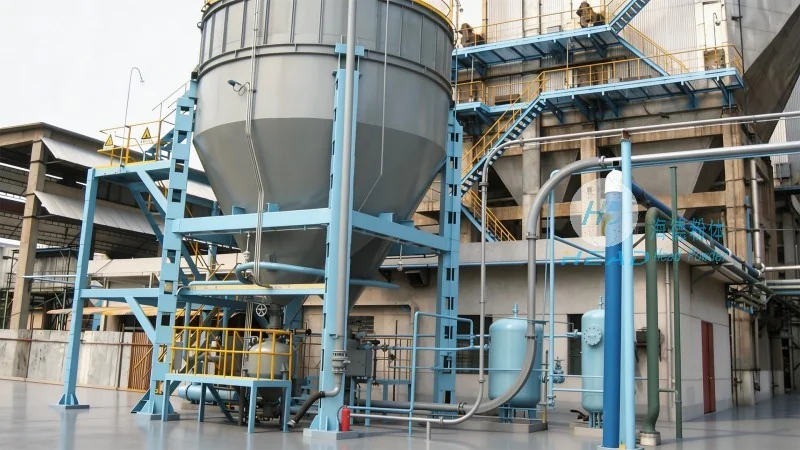
The working principle of the automatic weighing powder pneumatic conveying system is based on the fundamental concept of pneumatic transport, where material is moved through a pipeline using a gas (usually air). In this system, the air compressor supplies high-pressure air to the conveying pipeline, creating a flow that pulls the powder particles into the stream. The powder particles are suspended in the air flow, and the velocity of the air ensures that they are transported efficiently without clogging the pipeline. The integrated weighing scale measures the mass of the material as it passes through the weighing zone, typically located near the discharge point or within the pipeline. This measurement is crucial for controlling the flow rate and ensuring that the desired weight of material is delivered. The system uses feedback control to adjust the air pressure and flow rate, maintaining a stable and accurate weight of the conveyed material. The dust filter is incorporated to remove any fine particles from the air stream, ensuring that the exhaust air is clean and that the equipment operates efficiently without dust accumulation.
Advantages of Using Automatic Weighing Powder Pneumatic Conveying Equipment
Implementing automatic weighing powder pneumatic conveying equipment offers numerous advantages for industrial operations. Firstly, it provides high accuracy in weight measurement, which is essential for applications where precise dosing is required, such as in pharmaceutical manufacturing or food processing. The integrated weighing system eliminates manual errors and ensures consistent product quality. Secondly, the pneumatic conveying method is highly efficient, allowing for the transport of bulk powders over long distances without the need for mechanical conveyors, which can be costly and prone to maintenance issues. Thirdly, the automated operation reduces labor costs and increases production throughput, as the system can operate continuously without the need for constant monitoring. Additionally, the equipment is designed for easy maintenance and cleaning, which is critical for industries that handle hygienic materials, such as food and pharmaceuticals. The dust filter and sealed pipeline design help maintain a clean working environment, reducing the risk of contamination and improving safety in the workplace.
Applications and Industries
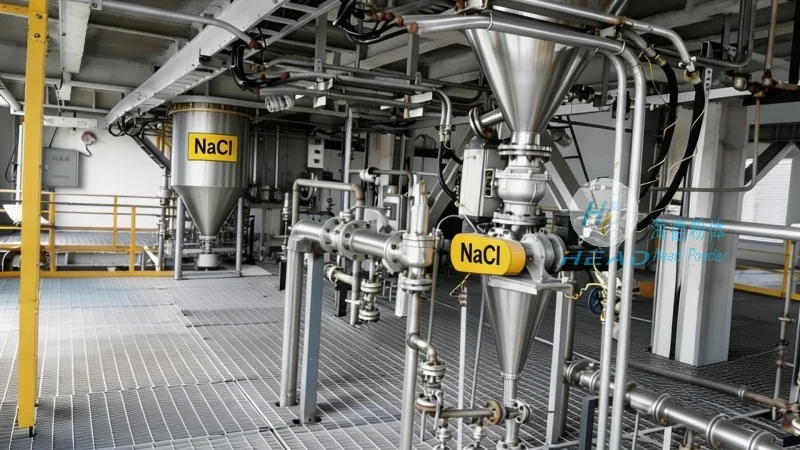
The automatic weighing powder pneumatic conveying equipment is widely used across various industries due to its versatility and efficiency. In the pharmaceutical industry, it is used for transporting active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the final dosage is accurate and meets regulatory standards. In the food processing industry, it is employed to handle powders such as flour, sugar, and spices, maintaining the quality and freshness of the products. The chemical manufacturing industry utilizes this equipment for transporting raw materials and intermediates, which often require precise measurement and handling. Other applications include the handling of cement, minerals, and other bulk materials in construction and mining industries. The adaptability of the system allows it to be customized for specific material properties and operational requirements, making it a versatile solution for diverse industrial needs.
Maintenance and Operational Tips
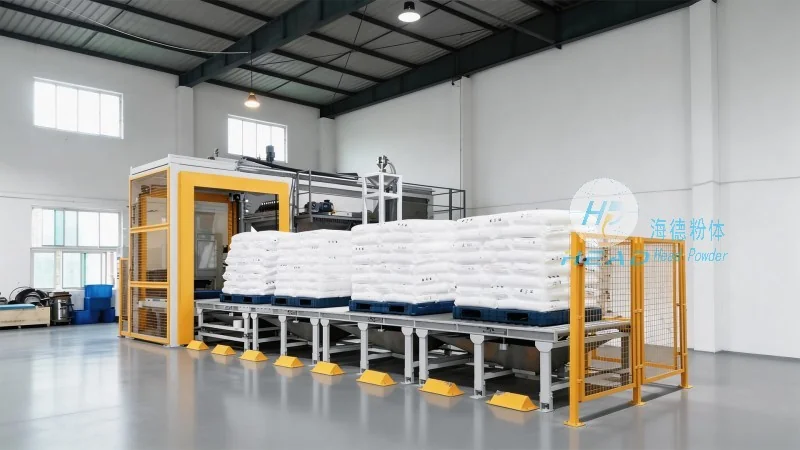
To ensure the optimal performance and longevity of the automatic weighing powder pneumatic conveying equipment, regular maintenance and proper operational practices are essential. Regular cleaning of the material hopper, conveying pipeline, and dust filter is necessary to prevent clogging and maintain air quality. The air compressor should be checked for proper pressure and oil levels to ensure efficient operation. The weighing scale should be calibrated periodically to maintain accuracy, as even minor deviations can affect the weight measurement. It is also important to monitor the air flow rate and pressure during operation, as fluctuations can impact the conveying efficiency and weight accuracy. Additionally, the system should be inspected for any signs of wear and tear, such as leaks in the pipeline or damage to the components, and addressed promptly to prevent further issues. Following these maintenance and operational tips will help maximize the equipment's lifespan and ensure consistent performance over time.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of industrial powder handling equipment. With a focus on innovation and quality, the company has established itself as a trusted provider of pneumatic conveying systems and related solutions. Headpowder's products are designed to meet the diverse needs of various industries, offering high efficiency, precision, and reliability. The company's commitment to customer satisfaction and technical excellence has made it a preferred choice for businesses seeking advanced powder handling solutions. Headpowder's headquarters is located in Shandong, China, where the company operates its research and development facilities, manufacturing plants, and customer support centers. The company's team of experts is dedicated to providing tailored solutions and technical support to ensure that clients achieve their operational goals effectively and efficiently.




