For industries dealing with bulk powder materials, efficient and reliable material handling systems are crucial for maintaining production efficiency and product quality. The intelligent tonne bag feeding station equipped with a powder pneumatic conveying machine is a sophisticated solution designed to streamline the process of transferring bulk powders from large bags into processing lines. This article provides a detailed overview of the operation process and working principles of such a system, highlighting its key components, operational steps, and the underlying technology that enables seamless material transfer. Developed by Shandong HeadPowder Engineering Co., Ltd. (headpowder), this system is engineered to meet the demanding requirements of modern industrial applications.
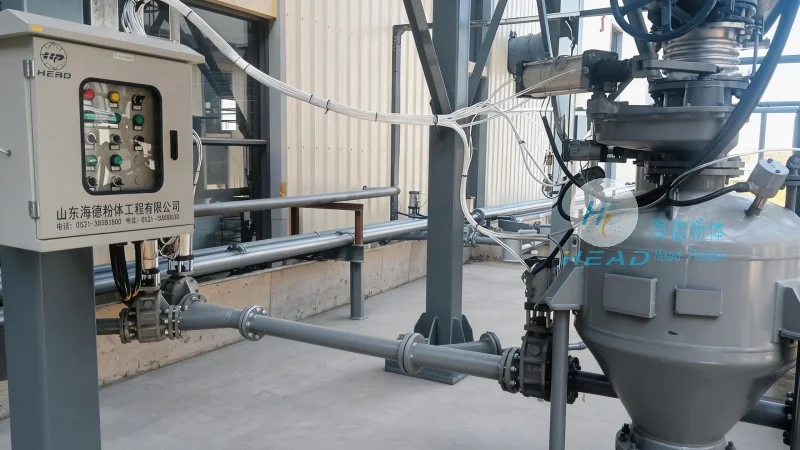
Overview of the Intelligent Tonne Bag Feeding Station
The intelligent tonne bag feeding station is a specialized system engineered to handle large volume powder bags, typically 1 tonne or more, and convert them into a manageable flow for downstream processing. The system integrates advanced automation and control technologies to ensure precise and consistent material transfer, minimizing human intervention and reducing the risk of contamination or material loss. Key components of this station include the bag opening mechanism, the pneumatic conveying system, and the control panel, all working in harmony to achieve optimal performance.
Key Components and Their Functions
1. Bag Opening and Sealing System: This component is responsible for safely opening the tonne bag and sealing it after the material is fully transferred. It typically uses a combination of cutting tools and sealing devices to ensure no material is spilled during the process. The system is designed to handle various bag types and materials, providing flexibility for different applications.
2. Pneumatic Conveying System: The core of the material transfer process, the pneumatic conveying system uses air pressure to transport the powder from the bag to the processing equipment. This system includes a hopper, a blower, and a pipeline network that directs the material to the desired location. The blower generates the necessary air flow, while the hopper collects the material from the bag and feeds it into the pipeline.
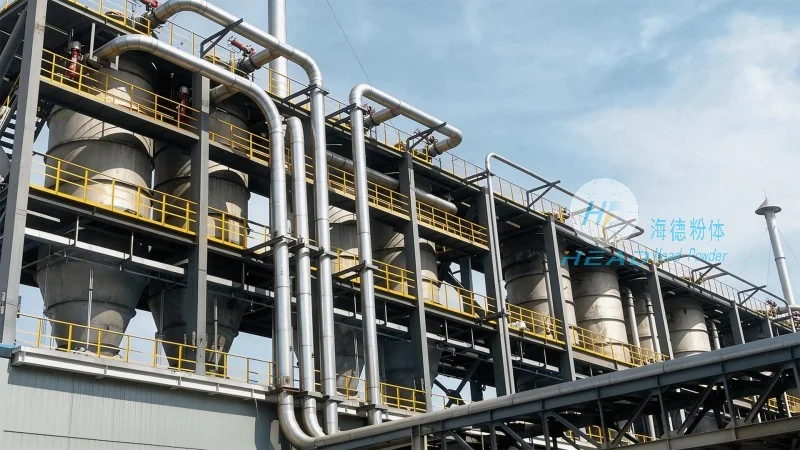
3. Control Panel and Automation: The control panel houses the electronic controls and sensors that monitor and regulate the entire operation. It allows operators to set parameters such as flow rate, pressure, and bag opening speed, ensuring the system operates within safe and efficient parameters. Automation features, such as automatic bag detection and material level monitoring, enhance the system's reliability and reduce downtime.
Operation Process Step-by-Step
The operation of the intelligent tonne bag feeding station follows a systematic sequence of steps to ensure smooth and efficient material transfer. The process begins with the placement of a tonne bag onto the station's loading platform. The system then automatically detects the bag and initiates the opening sequence. Once the bag is opened, the material is drawn into the hopper by the pneumatic conveying system. The blower generates the required air pressure, which propels the powder through the pipeline to the processing equipment. As the material is transferred, the system continuously monitors the bag's weight and material level, stopping the process once the bag is empty. The bag is then sealed, and the system is ready for the next bag.
Working Principle of the Pneumatic Conveying System
The working principle of the powder pneumatic conveying machine is based on the use of air as the conveying medium. When the blower operates, it creates a pressure difference between the hopper and the discharge point. This pressure difference causes the powder to be entrained in the air stream and transported through the pipeline. The system can operate in either positive or negative pressure modes, depending on the application requirements. Positive pressure systems are commonly used for short-distance conveying, while negative pressure systems are suitable for longer distances or when the material needs to be collected from multiple sources.
The design of the pipeline network is critical to the system's performance. It includes bends, filters, and silencers to ensure the smooth flow of material and to prevent blockages or pressure losses. The use of appropriate materials for the pipeline, such as stainless steel or plastic, is essential to prevent material degradation or contamination. The system also incorporates safety features, such as pressure relief valves and emergency stop buttons, to protect operators and equipment from potential hazards.
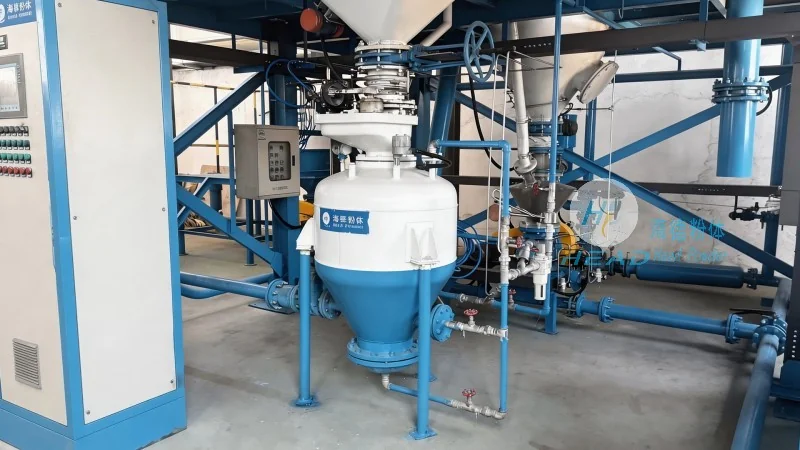
Advantages of the Intelligent Tonne Bag Feeding Station
The intelligent tonne bag feeding station offers several advantages over traditional manual or semi-automatic systems. These include improved efficiency, reduced labor costs, enhanced product quality, and increased safety. The automation of the process minimizes human error and ensures consistent material transfer, which is crucial for maintaining product quality and meeting production targets. Additionally, the system reduces the risk of dust exposure and material spillage, contributing to a safer working environment.
Applications and Industries
The intelligent tonne bag feeding station is widely used in various industries that handle bulk powders, including pharmaceuticals, food processing, chemicals, and minerals. In the pharmaceutical industry, the system is used to transfer active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination. In the food industry, it is used to handle ingredients such as flour, sugar, and spices, ensuring that the final product meets quality standards. In the chemical industry, the system is used to transfer raw materials and intermediates, contributing to the efficiency of production processes.
Conclusion
The intelligent tonne bag feeding station with a powder pneumatic conveying machine is a highly effective solution for industries requiring efficient and reliable bulk powder handling. By integrating advanced automation and control technologies, this system ensures precise and consistent material transfer, minimizing downtime and maximizing productivity. The working principles and operation process of the system are designed to meet the specific needs of different applications, providing flexibility and adaptability. As industries continue to demand higher efficiency and quality in material handling, such systems will play an increasingly important role in modern manufacturing processes.




