HeadPowder, a prominent name in the field of pneumatic conveying systems, specializes in providing advanced solutions for material handling, particularly through its dust-free bag loading stations. These stations are engineered to efficiently and safely transfer bulk materials from sealed bags into processing equipment, ensuring minimal contamination and optimal operational performance. This article delves into the operation process and working principles of such a system, highlighting the key components and the step-by-step procedures involved.
About HeadPowder: Pioneering Pneumatic Conveying Technologies
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company has established itself as a leading manufacturer and supplier of high-quality pneumatic conveying equipment, catering to diverse industrial sectors including pharmaceuticals, food processing, chemicals, and more. With a strong commitment to innovation and precision engineering, HeadPowder offers customized solutions tailored to meet the specific needs of clients, ensuring reliability, efficiency, and compliance with industry standards.
Dust-Free Bag Loading Station: A Core Component in Material Handling
The dust-free bag loading station is a critical piece of equipment designed to handle bulk materials from sealed bags without generating dust or contamination. This system integrates advanced filtration and air management technologies to maintain a clean and safe working environment. The station typically consists of several key components, including a bag opening mechanism, a hopper for material collection, a pneumatic conveying line, and a filtration system. Each component plays a vital role in the overall operation, ensuring smooth and efficient material transfer.
Operation Process: Step-by-Step Execution
The operation of a dust-free bag loading station for material pneumatic conveying involves a systematic sequence of steps, each designed to optimize material handling while maintaining safety and cleanliness. The process begins with the placement of a sealed bag into the station's designated position. The bag opening mechanism then activates, carefully cutting or tearing the bag's seal to allow material to flow into the hopper. Simultaneously, the filtration system begins to operate, drawing in filtered air to create a negative pressure environment within the station, which helps in preventing dust from escaping.
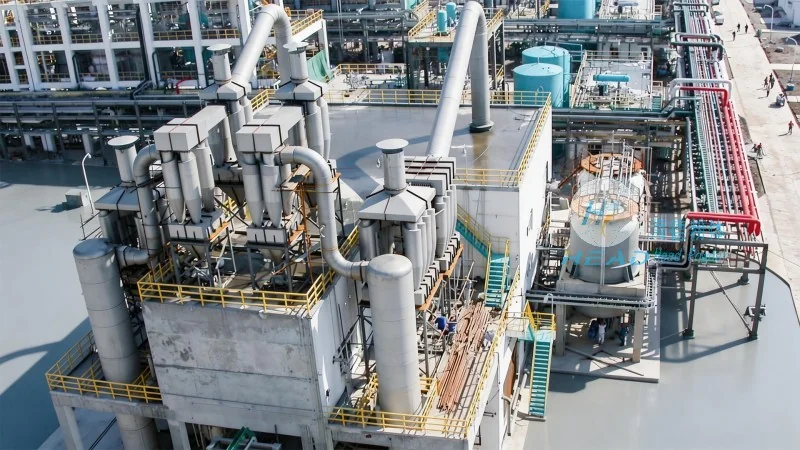
Once the bag is opened and material starts flowing into the hopper, the pneumatic conveying system is activated. The system uses compressed air to transport the material from the hopper through the conveying line to the processing equipment. The air flow is carefully controlled to ensure the material is conveyed smoothly without clogging or excessive pressure. As the material is transferred, the filtration system continuously captures any fine particles, ensuring that the air released from the station is clean and free from contaminants.
Working Principle: How the System Functions
The working principle of the dust-free bag loading station is based on the principles of pneumatic conveying, which utilizes air as the medium to transport bulk materials. The system operates by creating a pressure differential between the hopper and the processing equipment. The negative pressure within the hopper draws the material into the conveying line, while the positive pressure at the discharge end pushes the material forward. This pressure differential, combined with the air flow, ensures efficient and continuous material transfer.
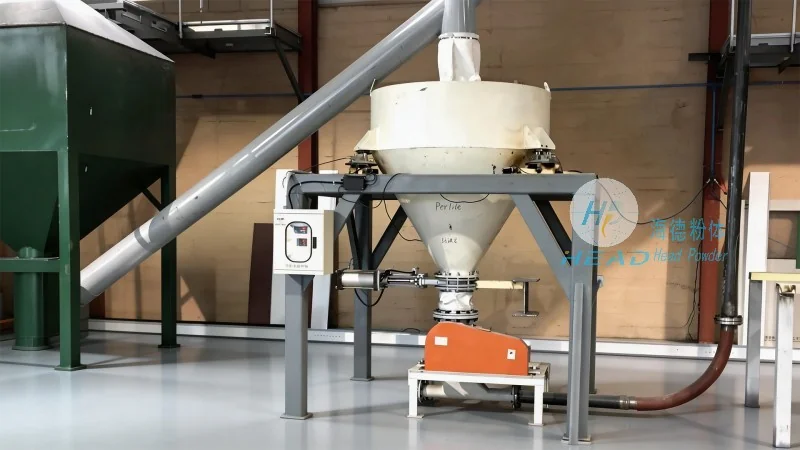
The filtration system is a crucial part of the working principle, as it maintains the cleanliness of the station and the surrounding environment. The system typically includes a pre-filter and a final filter, which work together to capture dust particles and other contaminants. The filtered air is then released back into the environment, ensuring that the station operates in a dust-free manner. Additionally, the system may include a vacuum pump or a blower to control the air pressure and flow, further enhancing the efficiency of the material transfer process.
Key Advantages and Applications
The dust-free bag loading station offers several advantages over traditional material handling methods. These include reduced dust exposure, improved safety for operators, and enhanced product quality due to minimal contamination. The system is particularly suitable for handling sensitive materials, such as pharmaceuticals, food products, and chemicals, where maintaining a clean environment is critical. Additionally, the station can handle a wide range of materials, including powders, granules, and bulk solids, making it a versatile solution for various industrial applications.
Conclusion: Enhancing Material Handling Efficiency
In conclusion, the dust-free bag loading station for material pneumatic conveying is a sophisticated system that combines advanced engineering and technology to provide efficient and safe material handling solutions. By understanding the operation process and working principles, users can appreciate the importance of each component and the step-by-step procedures involved. HeadPowder's expertise in designing and manufacturing such systems ensures that clients receive reliable and high-performance equipment tailored to their specific needs. With its headquarters in Shandong, China, HeadPowder continues to lead the way in providing innovative solutions for the material handling industry.




