Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer and supplier of industrial conveying systems. Based in Shandong, China, the company specializes in designing, manufacturing, and delivering efficient solutions for transporting bulk materials, particularly in the stone and coal powder sectors. With a focus on innovation and quality, headpowder has established itself as a trusted partner in the material handling industry, providing reliable equipment that meets the diverse needs of its clients.
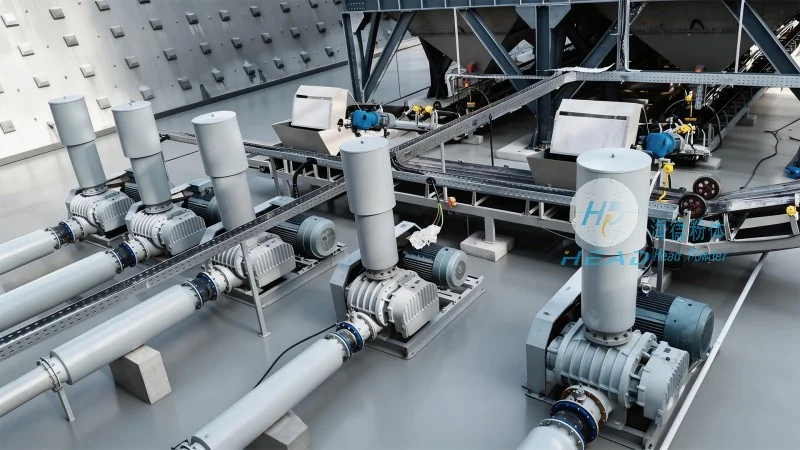
Overview of the Stone and Coal Powder Conveying System
The stone and coal powder conveying system is a specialized industrial equipment designed to transport bulk materials such as crushed stone, coal powder, and other fine or semi-fine powders. This system is widely used in mining, power generation, construction, and other industries where the efficient movement of bulk materials is critical to operational efficiency. The system combines advanced engineering principles with robust construction to ensure safe, reliable, and cost-effective material handling. By integrating various components like feeders, conveyors, and control systems, the system offers a comprehensive solution for material transport from source to destination.
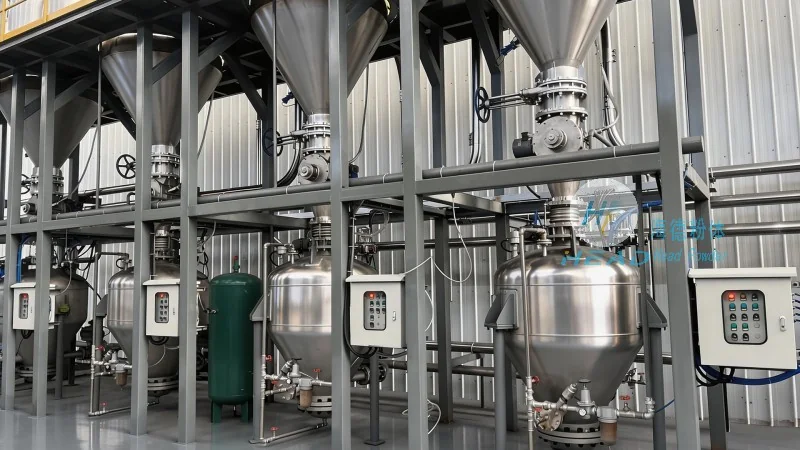
Structural Principles and Working Mechanism
The core of the stone and coal powder conveying system lies in its integrated structure, which includes key components such as the feeding mechanism, conveyor belt or pipe, drive system, and control unit. The feeding mechanism, typically a hopper or feeder, ensures a consistent and controlled flow of material into the system. This is followed by the conveyor section, which may be a belt conveyor, screw conveyor, or pneumatic conveyor, depending on the material characteristics and application requirements. The drive system, usually powered by electric motors, provides the necessary force to move the material along the conveyor path. The control unit, equipped with sensors and automation features, monitors the system's performance, adjusts the flow rate, and ensures safe operation. The structural design emphasizes durability, with materials like stainless steel and high-strength alloys used to withstand the abrasive nature of stone and coal powders. Additionally, the system incorporates features like dust suppression and sealing to maintain environmental compliance and operational safety.
Advantages of the Conveying System
Headpowder's stone and coal powder conveying system offers several advantages that make it a preferred choice for industrial applications. Firstly, the system is highly efficient, with optimized flow rates that minimize material loss and downtime. The robust construction ensures long service life, reducing maintenance costs and increasing overall productivity. The system's modular design allows for easy installation and customization, adapting to different site conditions and material types. Furthermore, the integration of automation and control features enhances operational safety and reduces the risk of accidents. The system also complies with industry standards for environmental protection, with features like dust collection and filtration to minimize air pollution. These advantages collectively contribute to improved operational performance and cost savings for users.
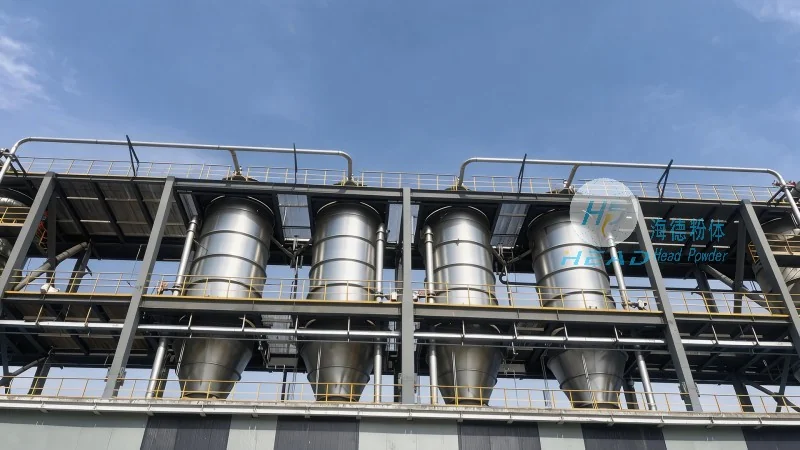
Applications and Industries
The stone and coal powder conveying system is versatile and finds applications in various industries. In the mining sector, it is used to transport crushed stone and coal from mines to processing facilities. In power generation, it plays a crucial role in delivering coal powder to boilers for energy production. The construction industry utilizes the system for transporting aggregates and other bulk materials to job sites. Additionally, in the chemical and food processing industries, similar conveying systems are employed for handling fine powders. The system's adaptability to different materials and operating conditions makes it suitable for a wide range of industrial processes, ensuring reliable material transport in diverse environments.




