The efficient and safe handling of sulfur materials is a critical aspect of industrial operations, particularly in sectors such as chemical manufacturing, petrochemical processing, and mining. Sulfur, in its various forms—solid, liquid, or gas—requires specialized equipment and systems to ensure proper transportation, storage, and processing. This article explores the fundamental concepts of sulfur material handling and the key design principles that underpin effective systems.
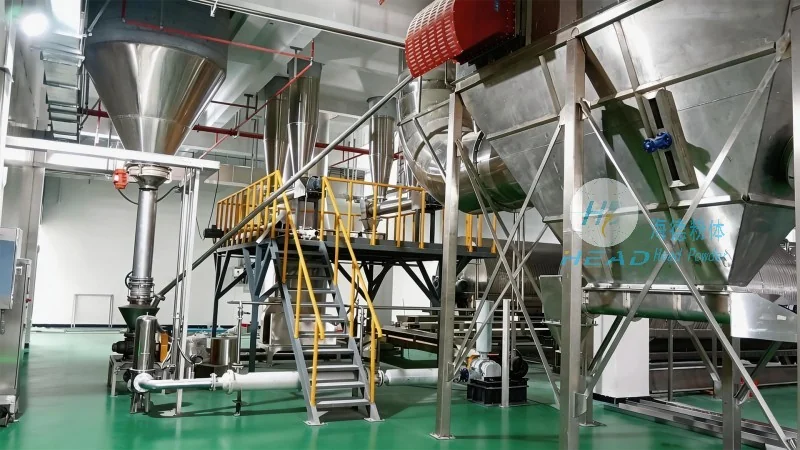
Company Overview
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, development, and implementation of advanced material handling solutions. With a strong focus on safety, efficiency, and reliability, HeadPowder provides tailored systems for sulfur processing, ensuring compliance with industry standards and operational requirements.
Key Design Principles for Sulfur Material Handling
The design of sulfur material handling systems involves several critical principles that address the unique properties of sulfur. These include:
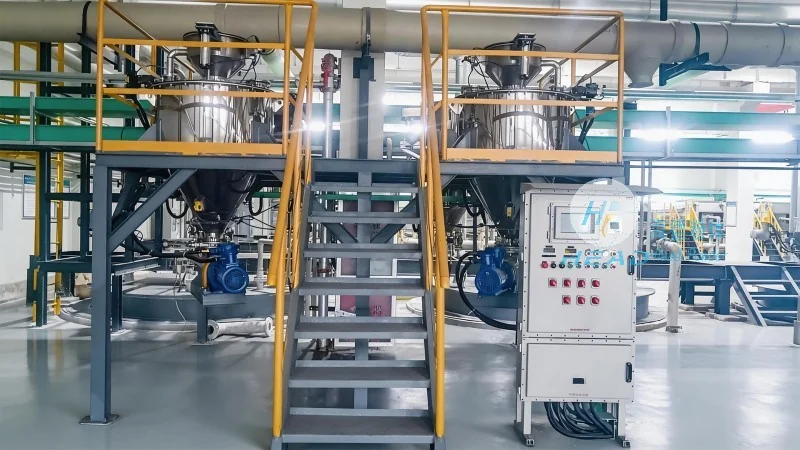
1. Material Compatibility and Corrosion Resistance
Sulfur, especially in its molten state, can be highly corrosive to certain materials. Designing systems with corrosion-resistant materials, such as stainless steel, Hastelloy, or specialized alloys, is essential to prevent equipment degradation and ensure long-term durability.
2. Temperature Management
Molten sulfur has a high melting point (around 115°C) and can operate at elevated temperatures. Effective temperature control systems, including insulation, heating elements, and cooling mechanisms, are crucial to maintain process stability and prevent thermal stress on components.
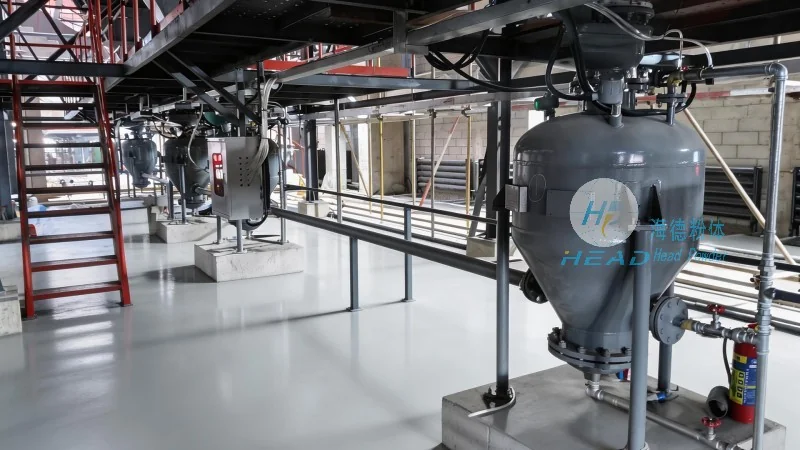
3. Flow Control and Pneumatic Systems
For solid sulfur, pneumatic conveying systems are often employed to transport material through pipelines. These systems use compressed air to move sulfur particles, requiring precise control of air pressure, flow rates, and pipeline design to avoid blockages or pressure drops.
4. Safety and Environmental Considerations
Sulfur handling involves potential hazards, including fumes, dust, and the risk of fire or explosion. Design principles incorporate safety features like explosion-proof equipment, dust collection systems, and proper ventilation to mitigate risks and comply with environmental regulations.
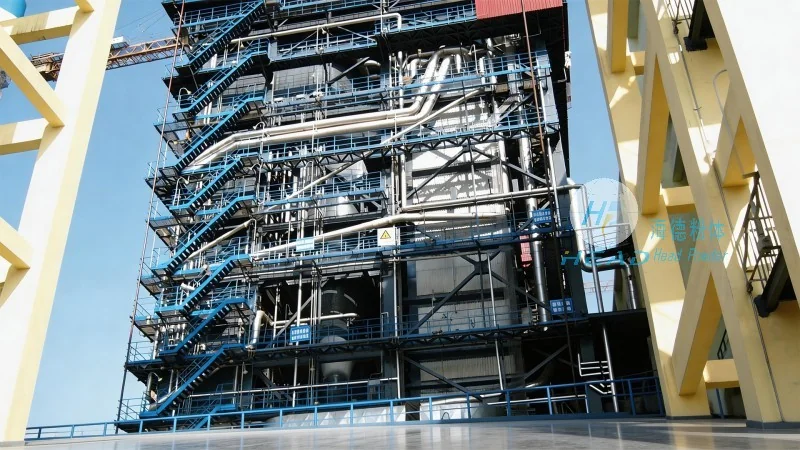
5. System Integration and Automation
Modern sulfur handling systems integrate various components, including feeders, conveyors, storage tanks, and processing units, with automation controls. This integration enhances operational efficiency, reduces human error, and enables real-time monitoring and control of the process.
Customized Solutions by HeadPowder
HeadPowder's expertise lies in customizing these design principles to meet specific client needs. By leveraging advanced engineering techniques and industry experience, the company develops solutions that optimize material flow, minimize downtime, and enhance overall plant performance. Whether for small-scale or large-scale operations, HeadPowder's systems are built to withstand the demanding conditions of sulfur processing while ensuring safety and reliability.




