For coffee processing facilities, efficient and reliable material handling is crucial to maintaining product quality and operational efficiency. The coffee powder pneumatic conveying system is a specialized solution designed to transport coffee powder and other fine particulate materials with precision and control. This article provides an overview of the equipment used in such systems, along with a detailed explanation of their structural principles and operational mechanisms.
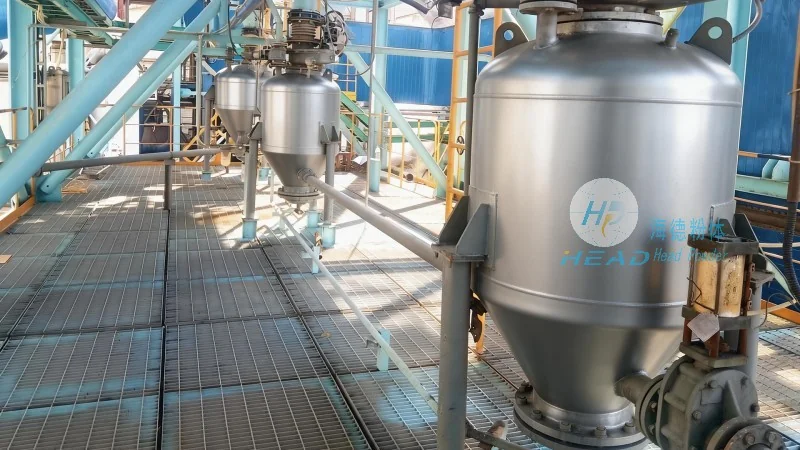
Coffee Powder Pneumatic Conveying System Overview
The coffee powder pneumatic conveying system is a closed-loop system that uses compressed air or other gases to transport coffee powder from one location to another. Unlike traditional mechanical conveyors, which rely on physical contact and friction, pneumatic systems operate by suspending particles in a gas stream, allowing for gentle and low-impact transport. This method is particularly advantageous for delicate materials like coffee powder, as it minimizes particle degradation and preserves the product's aroma and flavor characteristics.
Key Components of the Coffee Powder Pneumatic Conveying System
The coffee powder pneumatic conveying system consists of several critical components that work in tandem to ensure smooth operation. These include the material feed hopper, which holds the coffee powder and controls the flow rate; the air compressor or blower, which generates the necessary pressure to move the material; the conveying line, which is typically made of flexible or rigid tubing; and the receiver or discharge hopper, where the coffee powder is deposited. Additionally, the system may incorporate filters, cyclones, and control valves to regulate pressure, separate particles from the air stream, and manage the flow of material. The material feed hopper is equipped with a rotary valve or feeder to control discharge, preventing overfilling and maintaining a steady flow. The air compressor or blower is selected based on required pressure and flow rate, with options including rotary, reciprocating, or centrifugal types. The conveying line, often made of stainless steel or PVC, is designed to withstand system pressure and minimize friction. The receiver or discharge hopper may include a filter or cyclone to separate particles from the air stream and prevent dust contamination. Control valves such as pressure regulators and flow meters monitor and adjust system performance, ensuring optimal operation under varying conditions.
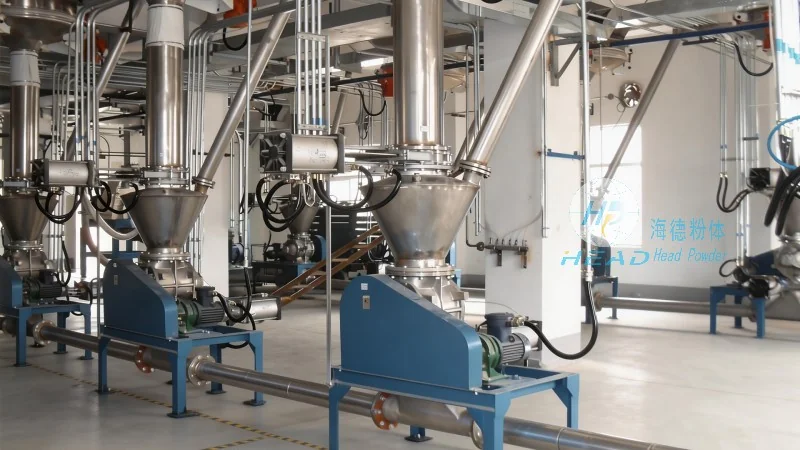
Structural Principles and Operational Mechanisms
The structural design of the coffee powder pneumatic conveying system is based on the principles of fluidization and particle suspension. When compressed air is introduced into the conveying line, it creates a low-density gas stream that lifts and transports the coffee powder particles. The velocity of the air stream is carefully controlled to maintain a stable suspension of particles, preventing clogging or blockages in the system. The system's design considers particle size, density, and moisture content, as these variables affect the optimal air velocity and pressure. For example, finer particles may require higher air velocities for stable suspension, while larger particles need lower velocities to avoid clogging. The system incorporates bends, elbows, and expansion joints to accommodate directional changes and pressure variations, ensuring smooth flow and preventing particle accumulation.
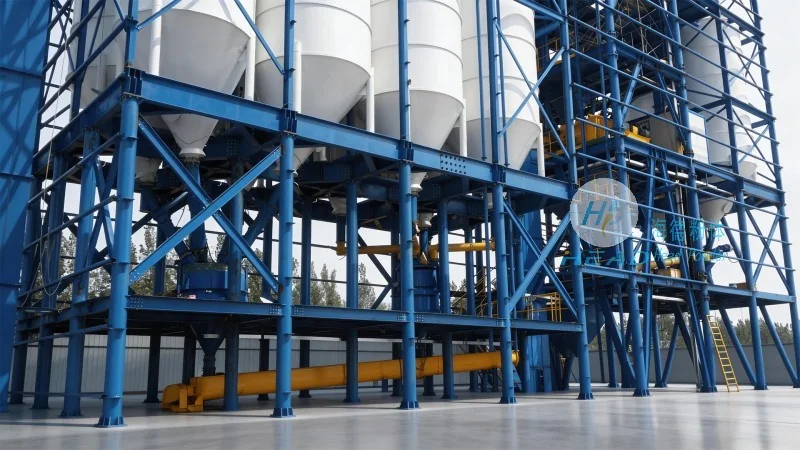
Advantages of Using a Coffee Powder Pneumatic Conveying System
Implementing a coffee powder pneumatic conveying system offers several benefits for coffee processing operations. Firstly, it provides a hygienic and enclosed environment, reducing contamination risk and minimizing dust exposure for operators. This is vital in food processing environments where product safety and quality are paramount. Secondly, the system's gentle handling minimizes product degradation, preserving the coffee powder's aroma, flavor, and color—critical for maintaining market value. Thirdly, the system is highly flexible, allowing easy integration with existing processing lines and enabling facility upgrades or expansions without significant disruption. Finally, the closed-loop design enhances energy efficiency by recycling the air stream and reducing waste, leading to lower operational costs over time. The system's reliability and durability also ensure long-term performance, reducing maintenance and downtime for coffee processing facilities.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of specialized material handling equipment, including coffee powder pneumatic conveying systems. With a focus on innovation and quality, the company has developed advanced solutions tailored to the unique needs of the coffee industry. Headpowder's equipment is designed to meet the highest standards of performance, reliability, and durability, ensuring long-term operational efficiency for coffee processing facilities. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with modern technology and quality control measures. Headpowder's team of engineers and technicians has extensive experience in designing and manufacturing high-performance equipment, ensuring that each system meets the specific requirements of its clients. The company's products are designed to meet international standards and are widely used in coffee processing facilities around the world, providing reliable and efficient material handling solutions. The company's focus on customer satisfaction and technical support ensures that clients receive comprehensive assistance throughout the equipment lifecycle, from installation to maintenance and troubleshooting.




