

Working Principle and Features of Brown Sugar Pneumatic Conveying Equipment
Brown sugar, with its rich molasses content and distinct granular structure, presents unique handling challenges in industrial processing. Traditional conveying methods such as belt conveyors or bucket elevators may struggle with the sticky and hygroscopic nature of this sweetener. Pneumatic conveying systems, particularly those designed for bulk materials like brown sugar, offer an efficient and hygienic solution to these challenges. This article explores the working principle and key features of brown sugar pneumatic conveyors, highlighting how they enhance operational efficiency and product quality in sugar processing facilities.
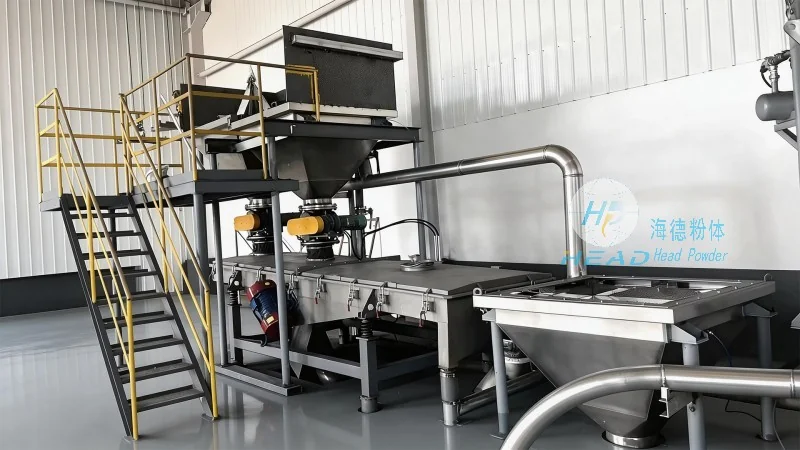
Working Principle of Brown Sugar Pneumatic Conveyors
The core mechanism of a brown sugar pneumatic conveyor involves the use of compressed air to transport bulk material through a pipeline system. The process typically begins with the material being fed into a hopper or feeder, where it is then drawn into the conveying line by the vacuum or pressure created by the air flow. For brown sugar, which is often handled in loose or granular form, the conveying system uses either positive pressure (air blowing material forward) or negative pressure (air sucking material into the line). The choice between these two modes depends on factors such as the material's density, moisture content, and the distance to be conveyed. In a positive pressure system, a blower generates high-pressure air that propels the sugar particles through the pipeline, while in a negative pressure system, a vacuum pump creates a low-pressure environment that pulls the material into the line. The pipeline network is designed with appropriate bends, elbows, and expansion joints to accommodate the flow dynamics and prevent material blockages or degradation. The entire system is equipped with filters and cyclones to separate the air from the sugar, ensuring that the conveyed material remains clean and free from dust or contaminants. This separation process is crucial for maintaining the quality of brown sugar, as any residual air or particles could affect its taste and appearance.
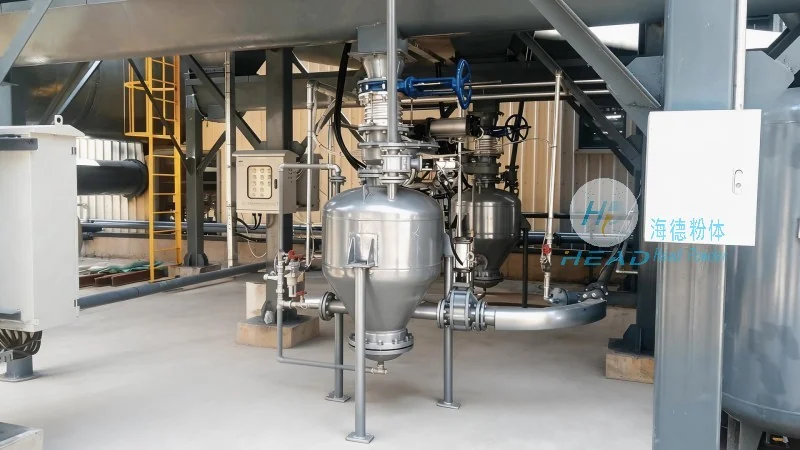
Key Features of Brown Sugar Pneumatic Conveyors
When selecting a pneumatic conveyor for brown sugar applications, several key features must be considered to ensure optimal performance and durability. First, the material's hygroscopic nature requires equipment that can handle moisture without causing clumping or caking. Pneumatic conveyors with smooth, non-stick surfaces and efficient cleaning mechanisms are essential to prevent material buildup. Second, the system must be designed to maintain the integrity of the sugar granules, avoiding excessive pressure or friction that could break down the crystals. This is achieved through the use of flexible hoses or smooth metal pipes with minimal bends, which reduce stress on the particles. Third, the conveying speed and air pressure must be precisely controlled to prevent overloading the system and ensure consistent flow rates. Advanced control systems, often integrated with sensors, allow operators to monitor and adjust the parameters in real-time, optimizing the conveying process for different batch sizes and material characteristics. Additionally, the system's hygienic design is critical in food processing environments, where compliance with regulatory standards is mandatory. Components such as hoppers, valves, and filters are constructed from stainless steel and other food-grade materials, with smooth surfaces that are easy to clean and sanitize. This design minimizes the risk of bacterial growth and cross-contamination, which is vital for maintaining the safety and quality of brown sugar products.
Benefits of Using Pneumatic Conveyors for Brown Sugar Handling
Implementing a pneumatic conveying system for brown sugar processing offers numerous advantages over traditional methods. One of the most significant benefits is the improvement in operational efficiency. Pneumatic conveyors can transport large volumes of material over long distances with minimal labor, reducing the need for manual handling and lowering the risk of accidents. The system's ability to handle bulk quantities in a continuous flow also streamlines production processes, allowing for faster batch completion and increased throughput. Another key benefit is the enhancement of product quality. By avoiding contact with metal surfaces or excessive friction, the conveyor preserves the natural texture and flavor of the brown sugar, ensuring that the final product meets the highest standards. The hygienic design of the equipment also contributes to better product quality by preventing contamination from dust, moisture, or foreign particles. Furthermore, pneumatic conveyors are more energy-efficient compared to other conveying methods, as they use compressed air to move material without the need for mechanical components like belts or chains. This results in lower operational costs and reduced environmental impact. The flexibility of the system is another advantage, as it can be easily adapted to different processing requirements, such as varying conveyor lengths or material types. This adaptability makes pneumatic conveyors a versatile solution for sugar processing facilities, whether they are handling raw brown sugar or finished products.
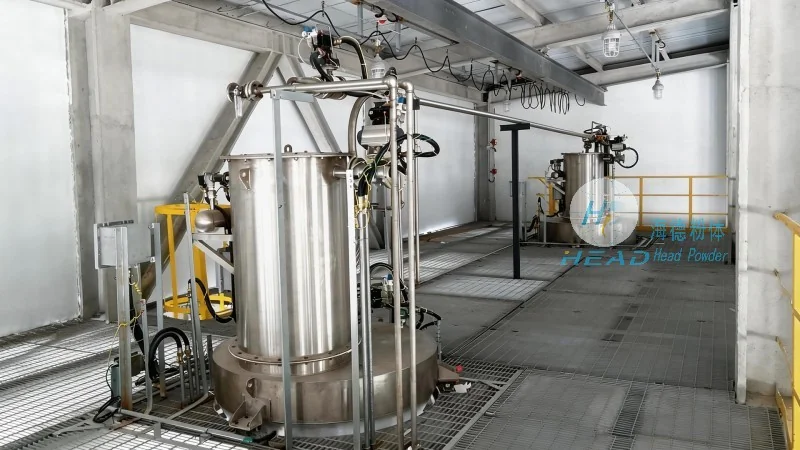
Conclusion and Company Information
As the demand for efficient and hygienic material handling solutions in the sugar industry continues to grow, brown sugar pneumatic conveyors have emerged as a reliable and effective choice. The working principle, which relies on compressed air to transport bulk material, combined with key features such as hygienic design and precise control, ensures that these systems meet the stringent requirements of modern sugar processing. By choosing a pneumatic conveyor from a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd., based in China, sugar processing facilities can enhance their operational efficiency, maintain product quality, and reduce costs. With a focus on innovation and quality, HeadPowder provides customized pneumatic conveying solutions tailored to the unique needs of brown sugar handling, helping businesses in the industry achieve optimal performance and sustainability. Whether for small-scale or large-scale operations, the benefits of pneumatic conveyors make them an indispensable component in the modern sugar processing landscape.