Cement fly ash is a byproduct of coal combustion in thermal power plants, widely used as a supplementary cementitious material in concrete production. The efficient handling and transportation of this fine powder are crucial for construction projects, as it directly impacts the quality and cost-effectiveness of concrete. This article explores the cement fly ash powder conveying equipment, its design principles, and the key factors that ensure optimal performance in industrial applications.
Introduction to Cement Fly Ash Powder Conveying Equipment
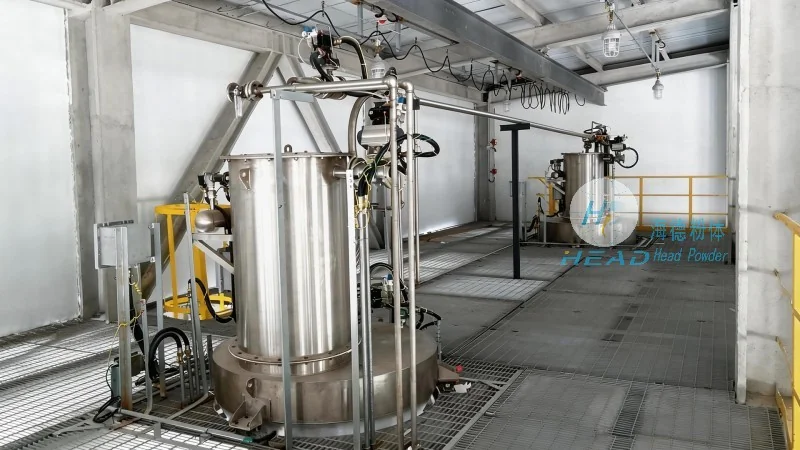
Cement fly ash powder conveying equipment is a specialized system designed to transport cement fly ash, a fine particulate material, from storage silos or production sites to concrete mixing plants or other processing facilities. These systems are engineered to handle the unique properties of fly ash, such as its low bulk density, high moisture content, and abrasive nature, ensuring reliable and continuous operation. The equipment typically includes components like feeders, conveyors, and control systems, all integrated to maintain consistent flow rates and prevent material degradation.
Key Components and Working Principle
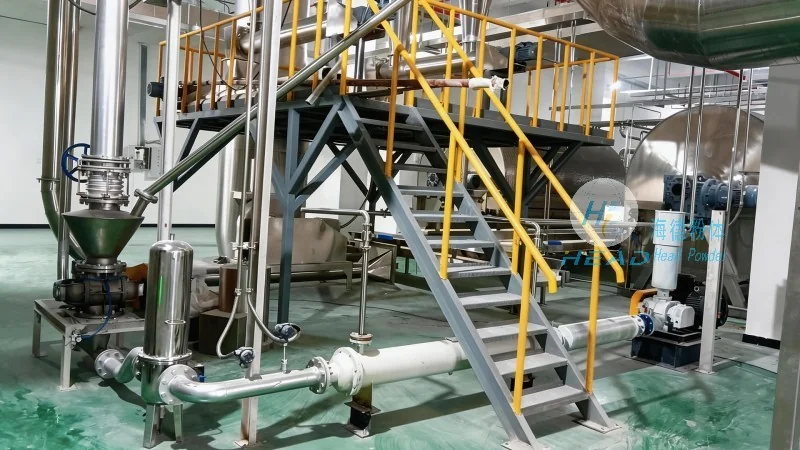
The core components of a cement fly ash powder conveying system include a hopper or silo for material storage, a feeding device (e.g., screw feeder or rotary valve) to regulate the flow of fly ash, a conveyor (such as a pneumatic or mechanical conveyor) to transport the material, and a control panel to monitor and adjust the system parameters. The working principle involves the material being discharged from the silo into the feeder, where it is metered and then conveyed through the system to the destination. Pneumatic conveying systems, for instance, use compressed air to move the fly ash in a pipeline, while mechanical systems rely on belts or screws to transport the material. The choice of component depends on factors like the material's characteristics, distance to be conveyed, and required flow rate.
Design Principles for Efficient Operation
Efficient design of cement fly ash powder conveying equipment is critical to minimize material loss, energy consumption, and operational downtime. Key design principles include:
1. **Material Compatibility**: The equipment must be constructed from materials resistant to corrosion and abrasion, such as stainless steel or special alloys, to withstand the harsh conditions of fly ash handling. This prevents equipment wear and ensures long-term reliability.
2. **Adequate Airflow or Mechanical Force**: For pneumatic systems, sufficient airflow is essential to maintain the material in suspension and prevent blockages. Mechanical systems require robust drive mechanisms to handle the high torque and load of fly ash transport. Proper sizing of the conveyor and air ducts is crucial to avoid excessive energy use or insufficient material transport.
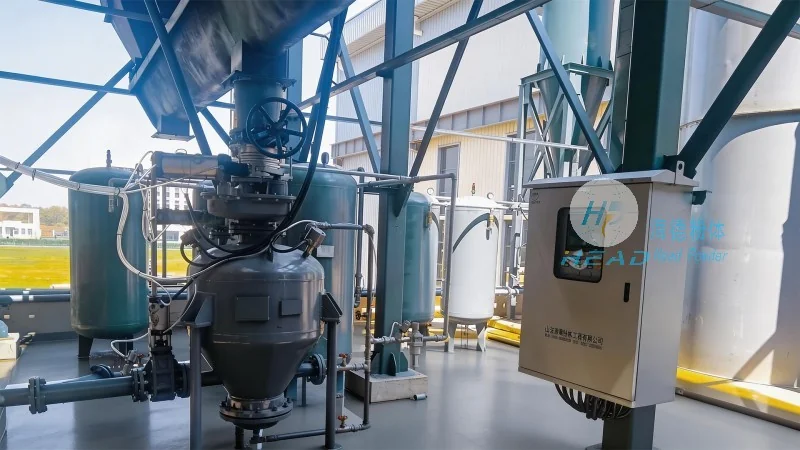
3. **Seal and Leak Prevention**: Fly ash is a fine powder that can easily escape through leaks, leading to environmental contamination and material loss. High-quality seals and tight fittings are incorporated into the system to minimize air or material leakage, ensuring compliance with environmental regulations and maintaining material integrity.
4. **Control and Monitoring Systems**: Modern conveying systems are equipped with advanced control panels that allow operators to adjust flow rates, monitor pressure, and detect blockages or malfunctions in real-time. This automation enhances operational efficiency and reduces the risk of system failures.
Application Scenarios and Benefits
Cement fly ash powder conveying equipment is widely used in the construction industry, particularly in large-scale concrete production plants, precast concrete manufacturers, and infrastructure projects. The benefits of using such equipment include:
1. **Improved Material Handling Efficiency**: The system enables continuous and automated transport of fly ash, reducing labor costs and increasing production throughput. This is especially valuable in high-demand construction projects where timely delivery of materials is critical.
2. **Enhanced Concrete Quality**: By ensuring consistent and uniform mixing of fly ash with other concrete ingredients, the equipment contributes to the production of high-quality concrete with improved durability and strength. This is essential for structures that require long-term performance, such as bridges and buildings.
3. **Environmental Protection**: Proper handling of fly ash reduces the risk of dust emissions and environmental pollution. The sealed systems and efficient conveying processes minimize the release of fine particles into the air, aligning with environmental regulations and promoting sustainable construction practices.
4. **Cost Reduction**: Efficient material transport reduces the overall cost of concrete production by minimizing material waste and energy consumption. The automation and reliability of the system also lower maintenance costs and downtime, contributing to better project economics.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of cement fly ash powder conveying equipment, with a strong presence in the Chinese construction industry. The company specializes in designing and manufacturing customized conveying systems tailored to the specific needs of clients, ensuring optimal performance and reliability. HeadPowder's products are known for their durability, efficiency, and compliance with industry standards, making them a trusted choice for construction companies and infrastructure projects.
Contact Information
For inquiries or to learn more about cement fly ash powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd., please contact us at our headquarters in Shandong, China.




