Understanding the working principle and key features of a hydrated sodium nitrate powder conveying system is crucial for industries that handle this specific chemical. This system is designed to efficiently transport hydrated sodium nitrate, a compound widely used in agriculture, food processing, and industrial applications. The following sections provide a detailed overview of how such a system operates and its distinguishing characteristics.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design, manufacturing, and installation of advanced powder handling systems. With a strong focus on precision engineering and customer-specific solutions, the company has established itself as a reliable partner for industries requiring efficient and safe material transport. The expertise of HeadPowder engineers ensures that each system is tailored to meet the unique demands of the application, whether it involves high-volume production or specialized chemical handling.
Working Principle of the Hydrated Sodium Nitrate Powder Conveying System
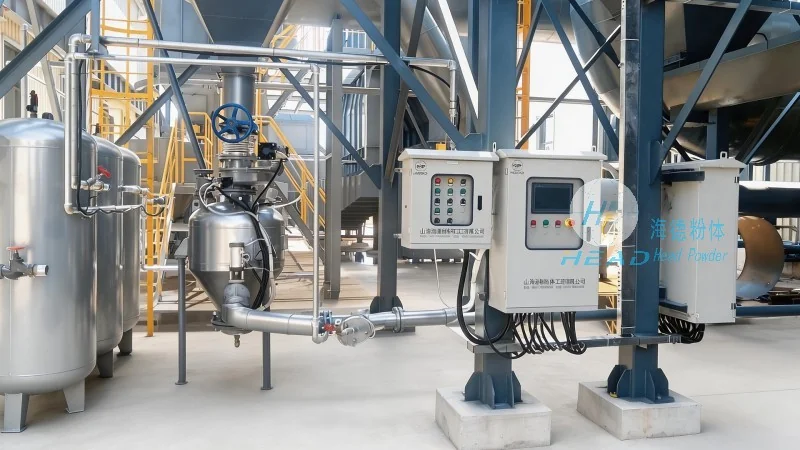
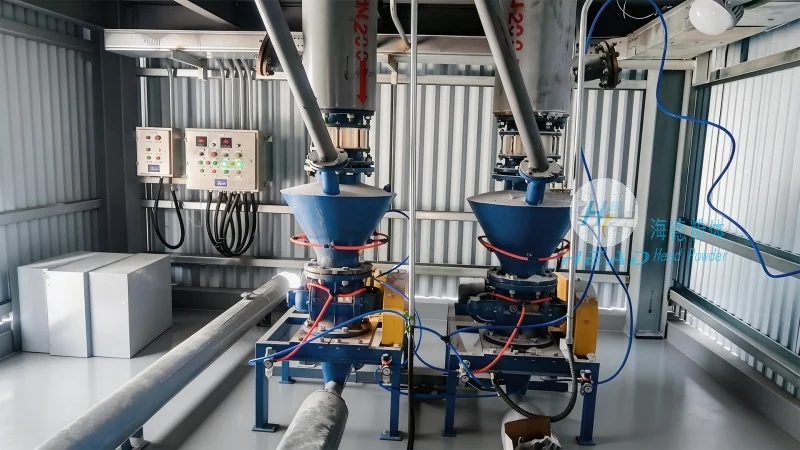
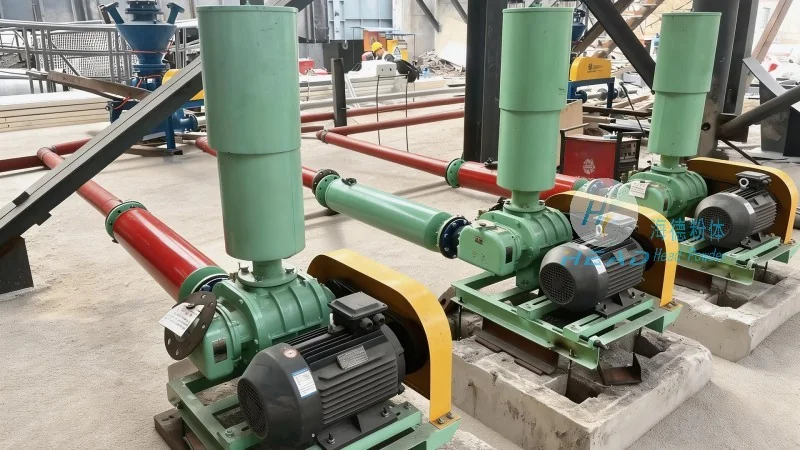
The core of the hydrated sodium nitrate powder conveying system lies in its integrated components that work in tandem to ensure smooth and controlled material movement. The system typically comprises a hopper for material storage, a feeding mechanism to regulate the flow of powder, a conveying device (such as a screw conveyor or pneumatic system), and a control unit to monitor and adjust the process. The hopper is designed to accommodate the bulk quantity of hydrated sodium nitrate, preventing caking and ensuring consistent feeding. The feeding mechanism, often a variable-speed feeder, controls the rate at which the powder is released into the conveying line, preventing overloading and maintaining a steady flow. The conveying device then transports the material to the desired destination, such as a storage silo or processing unit. The control unit plays a critical role by monitoring parameters like pressure, flow rate, and temperature, and adjusting the system in real-time to maintain optimal performance. This closed-loop control system enhances efficiency and reduces the risk of material degradation or equipment damage.
Key Features of the Hydrated Sodium Nitrate Powder Conveying System
The hydrated sodium nitrate powder conveying system from Shandong HeadPowder Engineering Co., Ltd. is equipped with several key features that enhance its performance and reliability. One of the primary features is its robust construction, which is built to withstand the corrosive and abrasive nature of hydrated sodium nitrate. The system uses high-quality materials, such as stainless steel and specialized coatings, to prevent corrosion and ensure long-term durability. Another notable feature is the system's ability to handle varying moisture content in the powder, which is crucial for maintaining the quality of the material during transport. The design includes moisture control mechanisms, such as drying or conditioning sections, to adjust the moisture level as needed. The system also incorporates safety features, including overfill protection, pressure relief valves, and emergency stop buttons, to ensure safe operation and prevent accidents. Additionally, the system is designed for easy maintenance, with accessible components and modular design that allows for quick repairs and replacements. This reduces downtime and lowers the overall maintenance cost for the user.
Efficiency and Performance Benefits
The hydrated sodium nitrate powder conveying system offers significant efficiency and performance benefits for industrial applications. By maintaining a consistent flow rate and minimizing material loss, the system reduces waste and improves overall productivity. The closed-loop control system ensures that the conveying process is optimized, leading to lower energy consumption and operational costs. The system's ability to handle high volumes of material without clogging or degradation makes it ideal for continuous production lines. Furthermore, the system's design allows for easy integration with existing production equipment, reducing the need for extensive modifications to the facility. This flexibility makes the system a cost-effective solution for industries looking to upgrade their material handling capabilities. The reliability of the system, backed by the expertise of HeadPowder engineers, ensures that it operates consistently over long periods, providing a stable supply of hydrated sodium nitrate to downstream processes.
Application-Specific Adaptations
Shandong HeadPowder Engineering Co., Ltd. recognizes that different industries have unique requirements for hydrated sodium nitrate handling. Therefore, the company offers customized solutions that adapt to specific application needs. For example, in agricultural applications, the system may be designed to handle larger quantities of material and integrate with storage silos for farm use. In food processing, the system may incorporate additional cleaning and sanitation features to meet food safety standards. The company's engineers work closely with clients to understand their operational needs and design a system that maximizes efficiency and safety. This tailored approach ensures that the system not only meets the technical requirements but also aligns with the client's operational goals. The adaptability of the system makes it suitable for a wide range of applications, from small-scale operations to large industrial facilities.
Conclusion
In summary, the hydrated sodium nitrate powder conveying system from Shandong HeadPowder Engineering Co., Ltd. combines advanced engineering with robust design to provide an efficient and reliable solution for material transport. The system's working principle, which involves integrated components and closed-loop control, ensures smooth and controlled movement of hydrated sodium nitrate. Key features such as corrosion resistance, moisture control, and safety mechanisms enhance its performance and longevity. The efficiency and adaptability of the system make it a valuable asset for industries handling this chemical. With its headquarters in Shandong, China, HeadPowder Engineering continues to deliver high-quality solutions that meet the evolving needs of its clients, ensuring that the hydrated sodium nitrate powder conveying system remains a reliable choice for material handling applications.




