Working Principle and Features of Magnesium Sulfate Material Handling Equipment
Release time:2026-09-17 20:01:24
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in material handling equipment, with a focus on solutions for magnesium sulfate transport. The company is located in Shandong, China, and has extensive experience in designing and manufacturing equipment tailored to the needs of the chemical industry. This article explores the working principle and key features of magnesium sulfate material handling equipment, providing insights into how these systems operate and their benefits for industrial applications.
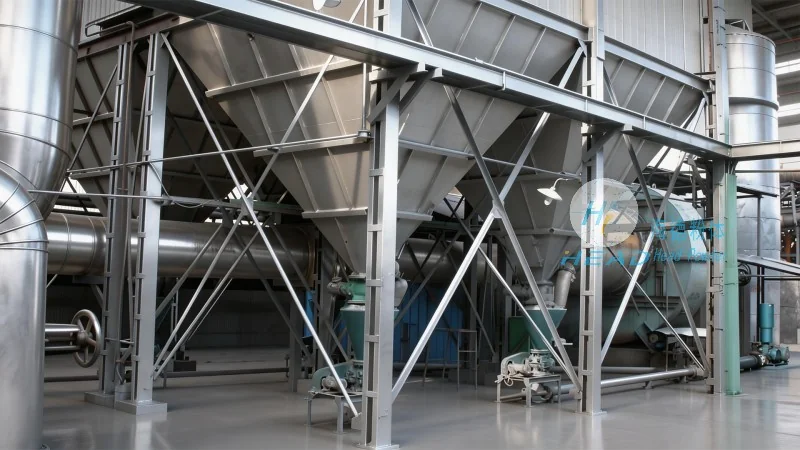
Working Principle of Magnesium Sulfate Material Handling Equipment
The working principle of magnesium sulfate material handling equipment typically involves several key components and processes. These systems are designed to efficiently transport bulk magnesium sulfate from storage areas to processing or packaging units. The equipment often includes conveyors, such as belt conveyors or screw conveyors, which move the material through the system. Magnetic separators may be integrated to remove metal contaminants, ensuring the purity of the magnesium sulfate. The control system manages the flow rate and direction of the material, optimizing the overall operation. Additionally, the system may include feeding mechanisms to regulate the amount of material entering the conveyor, preventing overloading and maintaining consistent flow. The entire process is automated to minimize human intervention, enhancing operational efficiency and reducing the risk of errors.
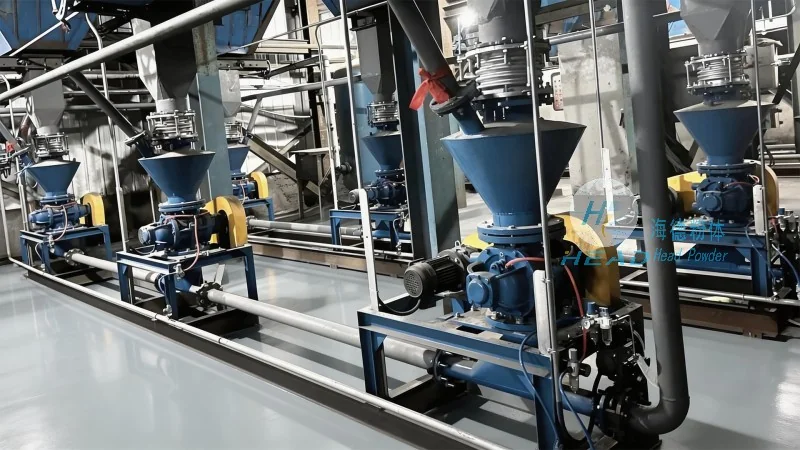
Key Features of Magnesium Sulfate Material Handling Equipment
Key features of magnesium sulfate material handling equipment include high efficiency and reliability. The equipment is engineered to handle the specific physical properties of magnesium sulfate, such as its bulk density and flow characteristics. Advanced materials are used in the construction to resist corrosion and wear, extending the equipment's service life. The design also emphasizes safety, with features like emergency stop buttons and protective guards to prevent accidents. Additionally, the systems are modular, allowing for easy integration into existing production lines and future expansion. The control system is user-friendly, with intuitive interfaces that enable operators to monitor and adjust the equipment's performance in real-time. This ensures that the system operates at peak efficiency and can be quickly adjusted to meet changing production demands.
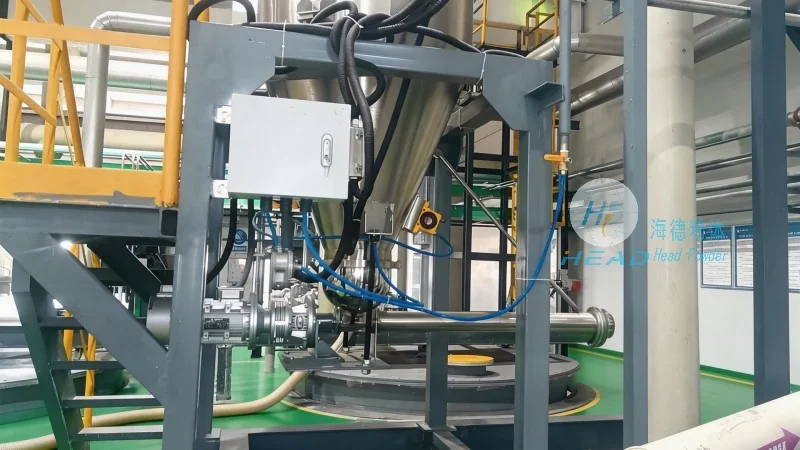
Advantages of Using Magnesium Sulfate Material Handling Equipment
Implementing magnesium sulfate material handling equipment offers several advantages for industrial operations. The primary benefit is improved productivity, as the equipment can handle large volumes of material with minimal downtime. The automated control system reduces the need for manual labor, lowering labor costs and minimizing the risk of human error. The equipment's durability and resistance to corrosion ensure long-term reliability, reducing maintenance costs and extending the equipment's service life. Furthermore, the modular design allows for scalability, enabling companies to expand their operations without significant capital investment. The safety features integrated into the design protect both personnel and equipment, reducing the risk of accidents and associated costs. Overall, magnesium sulfate material handling equipment is a critical component in modern industrial processes, enhancing efficiency, safety, and cost-effectiveness.




