HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of intelligent powder pneumatic conveying equipment. This article aims to provide a detailed explanation of the working principle and key features of such equipment, highlighting its technological advancements and practical applications in various industries.
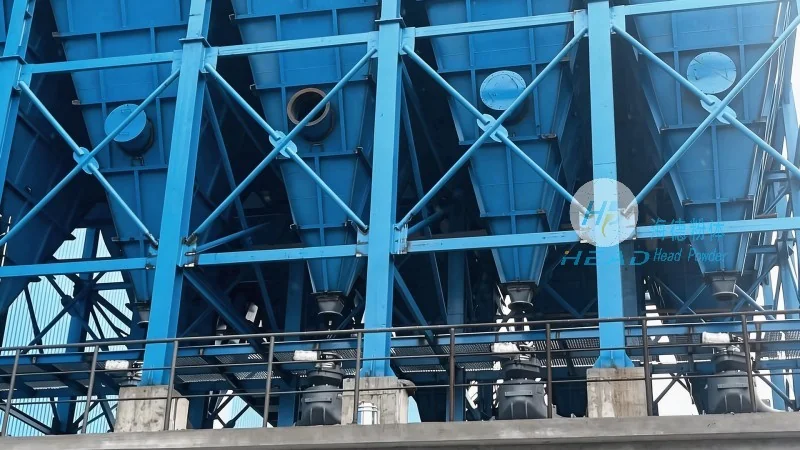
Understanding the Working Principle of Intelligent Powder Pneumatic Conveying Equipment
The core function of intelligent powder pneumatic conveying equipment is to transport bulk powder materials through an air stream. The system typically operates by generating a high-pressure air flow, which draws the powder from a hopper or storage tank into a pipeline. The equipment uses a combination of positive and negative pressure zones to control the flow of both air and powder, ensuring efficient and reliable material transfer. Advanced control systems, often integrated with sensors and automation technology, enable real-time monitoring and adjustment of the conveying process. This intelligent control enhances operational efficiency, reduces energy consumption, and minimizes material loss or degradation during transport.
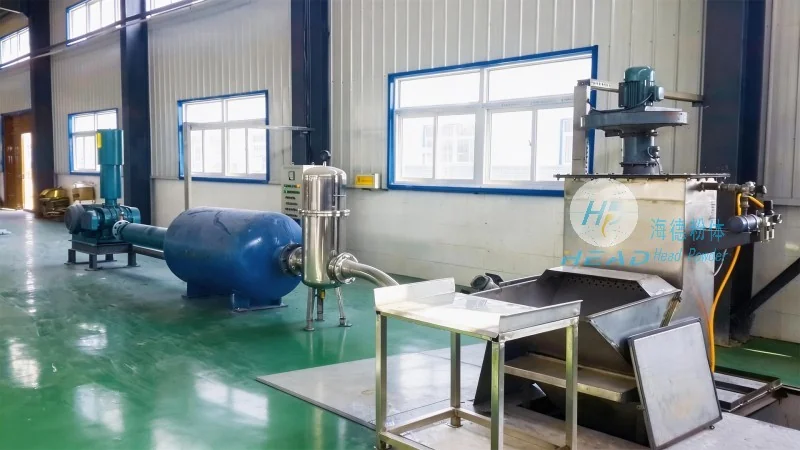
Key Features of Intelligent Powder Pneumatic Conveying Equipment
Intelligent powder pneumatic conveying equipment from HeadPowder is characterized by several advanced features that set it apart in the industry. Firstly, the system incorporates smart control technology, allowing for precise regulation of air pressure, flow rate, and material feed. This ensures consistent and stable conveying performance, even with varying powder properties or load conditions. Secondly, the equipment is designed with robust and durable components, such as high-quality stainless steel pipelines and advanced air compressors, to withstand the demands of continuous operation in demanding environments. Thirdly, the integration of sensors and data analytics provides operators with real-time insights into system performance, enabling proactive maintenance and troubleshooting. Additionally, the equipment is equipped with safety features, including pressure relief valves and emergency shut-off mechanisms, to ensure safe and reliable operation. These features collectively contribute to improved productivity, reduced downtime, and enhanced overall operational efficiency.
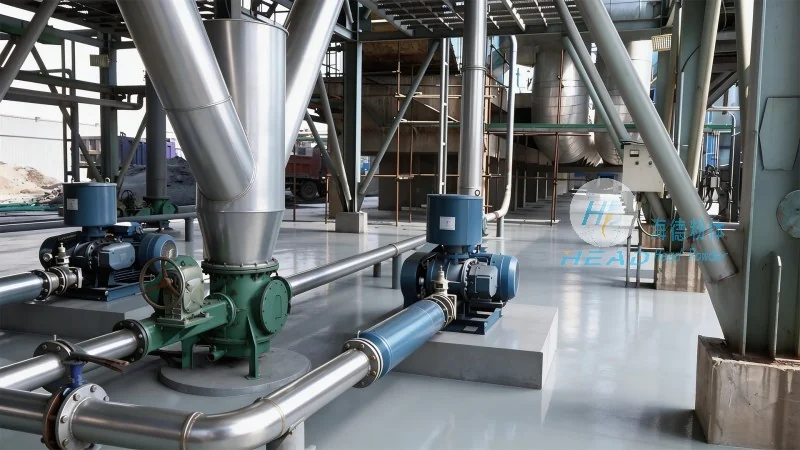
Applications and Benefits in Industrial Settings
Intelligent powder pneumatic conveying equipment is widely used across various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. The technology offers significant advantages over traditional conveying methods, such as reduced labor costs, improved material handling safety, and the ability to transport materials over long distances without the need for intermediate storage or manual handling. The equipment's ability to handle a wide range of powder types, from fine powders to bulk materials, makes it versatile for different industrial applications. Furthermore, the intelligent control systems help maintain product quality by preventing contamination and ensuring consistent particle size distribution. In summary, the adoption of intelligent powder pneumatic conveying equipment not only enhances operational efficiency but also contributes to cost savings and improved product quality in industrial settings.




