For industries dealing with gray calcium powder, efficient material handling is crucial. Pneumatic conveyors, specifically designed for handling such powders, offer a reliable solution. This article explores the working principle and key features of these specialized conveyors, highlighting how they enhance operational efficiency and safety in material transport.
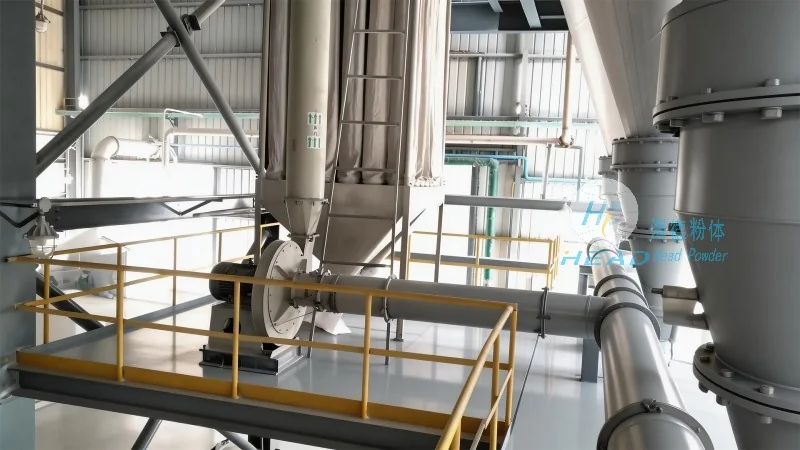
Introduction to Pneumatic Conveyors for Gray Calcium Powder
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in developing advanced pneumatic conveying systems tailored for gray calcium powder applications. Based in China, the company leverages years of expertise to craft equipment that meets the stringent demands of the industry. The following sections delve into the core mechanisms and distinctive attributes of these systems, providing a comprehensive understanding for potential users.
The Working Principle of Pneumatic Conveyors
Pneumatic conveyors operate by utilizing air pressure to transport dry materials like gray calcium powder through a pipeline system. The process typically involves a combination of positive and negative pressure or vacuum to move the material from the source to the destination. In the case of gray calcium powder, the conveyor system may employ a positive pressure method, where compressed air forces the powder through the pipeline. The key components include a hopper for material storage, a blower or compressor to generate air flow, and a pipeline network that guides the material. The material is fed into the system, often via a rotary valve or feeder, and is then carried by the air stream to the discharge point. This method ensures a continuous and controlled flow of the powder, minimizing the risk of clogging and ensuring consistent performance.
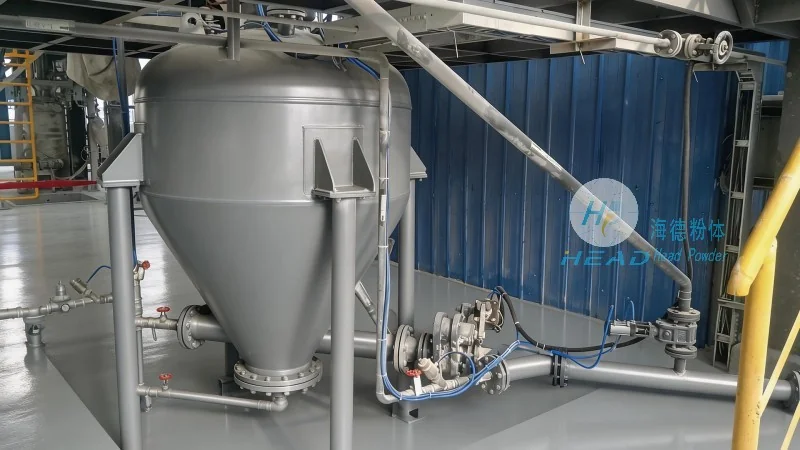
Key Features of Gray Calcium Powder Pneumatic Conveyors
Several distinctive features make pneumatic conveyors ideal for gray calcium powder handling. Firstly, the system is fully enclosed, which prevents dust dispersion and ensures a clean working environment. This is particularly important for gray calcium powder, as it can be a source of airborne particles that may affect air quality and worker health. Secondly, the equipment offers high efficiency in material transport, with the ability to move large quantities of powder over significant distances without the need for manual handling. The design also allows for easy integration with existing production lines, reducing downtime and enhancing overall productivity. Additionally, the conveyors are designed for low maintenance, with components that are resistant to wear and corrosion, ensuring long-term reliability. Another notable feature is the flexibility in system configuration, as the pipeline layout can be adjusted to suit different facility layouts and operational requirements. This adaptability makes the conveyors suitable for various industrial applications, from small-scale operations to large-scale production lines.
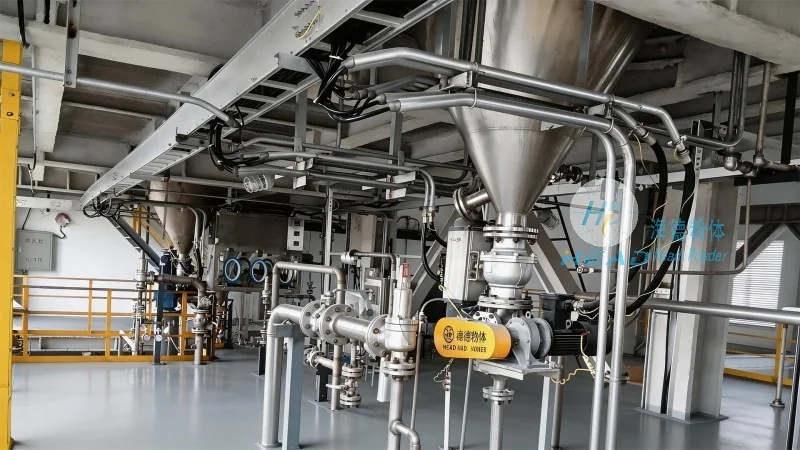
Benefits and Applications
The adoption of pneumatic conveyors for gray calcium powder offers numerous benefits. From a practical standpoint, the enclosed system enhances workplace safety by containing dust and preventing contamination. This not only protects workers from respiratory issues but also maintains product quality by avoiding exposure to external elements. Economically, the system reduces labor costs associated with manual material handling and minimizes material loss due to spillage. In terms of operational efficiency, the continuous flow of material ensures that production processes run smoothly, with minimal interruptions. The technology is also environmentally friendly, as it reduces the need for external transportation methods that may contribute to carbon emissions. Industries such as construction, pharmaceuticals, and food processing can all benefit from these systems, as they handle gray calcium powder in a manner that aligns with modern safety and sustainability standards.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides advanced pneumatic conveyors specifically designed for gray calcium powder materials. By understanding the working principle and key features of these systems, users can make informed decisions about integrating such equipment into their operations. The enclosed design, high efficiency, and low maintenance requirements make these conveyors a superior choice for industries seeking reliable and safe material handling solutions. With a strong presence in China, the company continues to innovate and deliver products that meet the evolving needs of the market, ensuring that gray calcium powder is transported effectively and efficiently.




