For those in the agricultural and fertilizer processing industries, understanding the efficient operation of fertilizer powder conveying equipment is crucial for optimizing production lines and ensuring consistent material handling. This article provides a detailed overview of the operation process and working principle of such equipment, presented by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China.
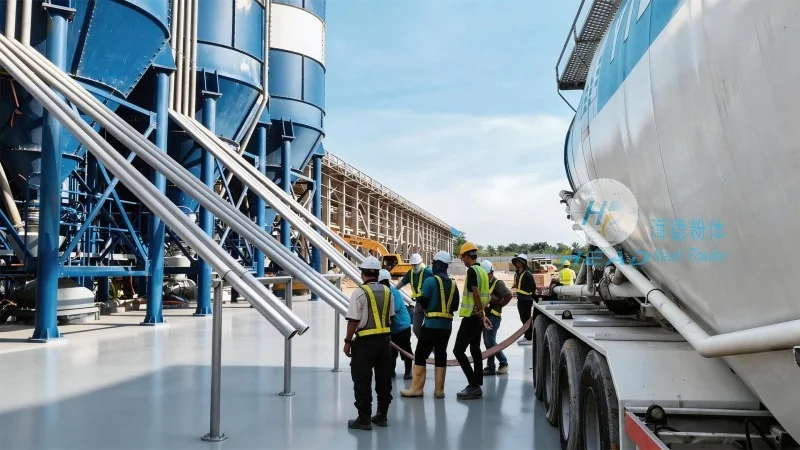
Company Introduction
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer specializing in the design, development, and production of high-quality conveying equipment for various industries. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the field of material handling solutions. The company’s headquarters is located in Shandong, China, where it leverages advanced technology and skilled expertise to deliver reliable and efficient equipment to global markets.
Overview of Fertilizer Powder Conveying Equipment
Fertilizer powder conveying equipment is designed to transport bulk fertilizer powders from storage silos or production lines to processing units, packaging systems, or storage areas. These systems are essential for maintaining smooth workflow in fertilizer manufacturing and distribution operations. The equipment typically includes components such as hoppers, feeders, conveyor belts or pipes, and control systems, all working in tandem to ensure safe and efficient material movement.
Working Principle of Fertilizer Powder Conveying Equipment
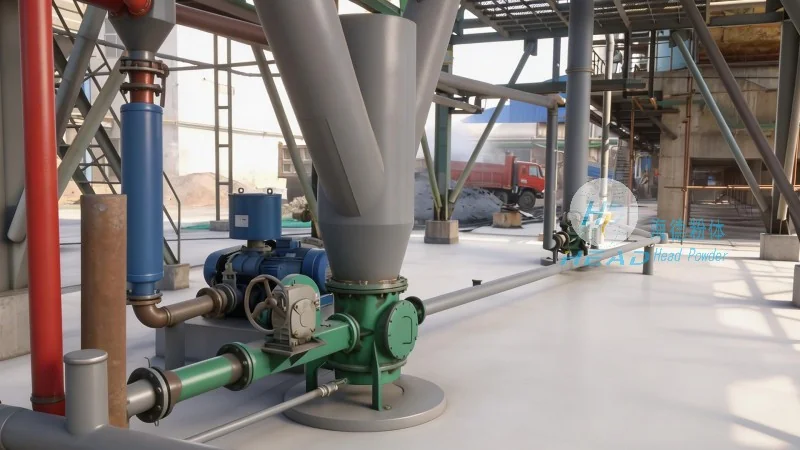
The working principle of fertilizer powder conveying equipment revolves around the controlled movement of bulk materials using mechanical or pneumatic systems. The process begins with the material being fed into a hopper, where it is stored and prepared for transport. A feeder, often a rotary valve or a screw feeder, then regulates the flow of fertilizer powder into the conveying system. The conveying mechanism, which can be a screw conveyor, pneumatic conveyor, or a combination of both, then transports the material through a pipeline or along a conveyor belt. The control system monitors the flow rate, pressure, and other parameters to ensure consistent and safe operation. This integrated approach ensures that the fertilizer powder is moved efficiently without degradation or loss.
Operation Process of Fertilizer Powder Conveying Equipment
The operation process of fertilizer powder conveying equipment involves several key steps that ensure the smooth and continuous movement of materials. First, the system is initiated by the control panel, which activates the feeder and conveyor. The feeder regulates the amount of fertilizer powder entering the system, while the conveyor transports it to the next stage of processing. During operation, the control system continuously monitors the pressure and flow rate to maintain optimal performance. If any abnormalities are detected, such as blockages or pressure drops, the system will automatically adjust or stop to prevent damage to the equipment or material. The process concludes when the fertilizer powder reaches its destination, such as a packaging machine or storage silo, where it is then processed or stored for distribution.
Key Components and Their Functions
Several key components work together to ensure the efficient operation of fertilizer powder conveying equipment. The hopper serves as a storage container, providing a buffer for the bulk material and preventing spillage. The feeder, typically a rotary valve or screw feeder, controls the flow rate of the fertilizer powder into the conveying system, ensuring a consistent and controlled feed. The conveyor mechanism, which can be a screw conveyor, pneumatic conveyor, or a combination, transports the material through the system. The control system monitors and regulates the operation of these components, ensuring optimal performance and safety. Each component plays a critical role in maintaining the integrity of the fertilizer powder and ensuring efficient material handling.
Advantages of Fertilizer Powder Conveying Equipment
Using fertilizer powder conveying equipment offers several advantages for fertilizer manufacturers and processors. These systems provide a safe and efficient method for transporting bulk materials, reducing the risk of dust explosions and material loss. The controlled flow rates and consistent operation help maintain product quality and prevent degradation. Additionally, the automated control systems reduce the need for manual intervention, improving operational efficiency and reducing labor costs. The equipment is also designed to be durable and reliable, with components that can withstand the harsh conditions of fertilizer processing, ensuring long-term performance and minimal downtime.
Application in Fertilizer Production Lines
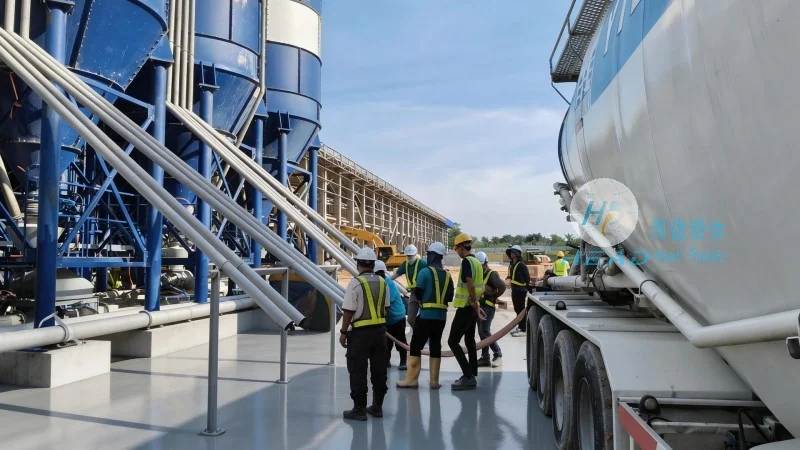
Fertilizer powder conveying equipment is widely used in various stages of fertilizer production lines. In the initial stages, it transports raw materials from storage silos to mixing and granulation units. In the later stages, it moves finished products from the packaging line to storage or shipping areas. The equipment is also used in blending operations, where different types of fertilizers are mixed to create customized formulations. The consistent and controlled transport of materials ensures that the final product meets quality standards and is delivered to customers efficiently. By integrating conveying equipment into the production line, manufacturers can achieve higher productivity and reduce operational costs.
Maintenance and Safety Considerations
Maintaining fertilizer powder conveying equipment is essential for ensuring its long-term performance and safety. Regular maintenance, including cleaning, lubrication, and inspection of components, helps prevent blockages and equipment failure. The control system should be checked regularly to ensure it is functioning correctly and that all safety features are active. Dust suppression systems are also important to prevent dust accumulation and reduce the risk of explosions. Proper training for operators is crucial to ensure they understand the equipment’s operation and safety procedures. By following these maintenance and safety guidelines, manufacturers can ensure the safe and efficient operation of fertilizer powder conveying equipment.
Conclusion
Fertilizer powder conveying equipment is a critical component of modern fertilizer production and distribution operations. The operation process and working principle of such equipment involve a combination of mechanical and control systems that work together to ensure efficient and safe material handling. By understanding these processes and maintaining the equipment properly, fertilizer manufacturers can optimize their production lines, improve product quality, and reduce operational costs. Shandong HeadPowder Engineering Co., Ltd. continues to lead in the development of advanced conveying equipment, providing reliable solutions for the global fertilizer industry.




