

Operation Process and Working Principle of Rice Husk Ash Powder Pneumatic Conveying System
HeadPowder, a leading provider in the field, specializes in advanced pneumatic conveying systems tailored for handling rice husk ash powder. This article delves into the operational process and underlying principles of such systems, highlighting the efficiency and reliability they offer in material transport.
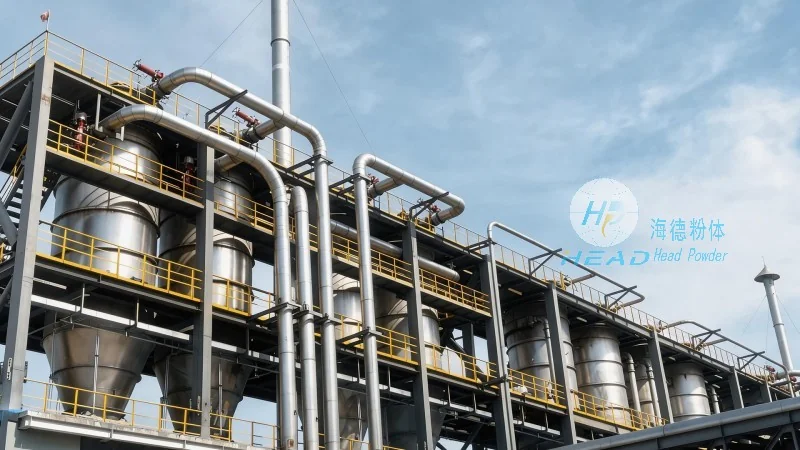
Company Overview
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company is dedicated to developing and manufacturing high-performance pneumatic conveying solutions, with a focus on optimizing material handling processes for various industrial applications.
Understanding Pneumatic Conveying
Pneumatic conveying systems utilize air or gas to transport bulk materials like rice husk ash powder through a pipeline network. This method offers several advantages over traditional mechanical conveying, including reduced equipment wear, lower maintenance costs, and the ability to handle materials with high moisture content or abrasive properties.
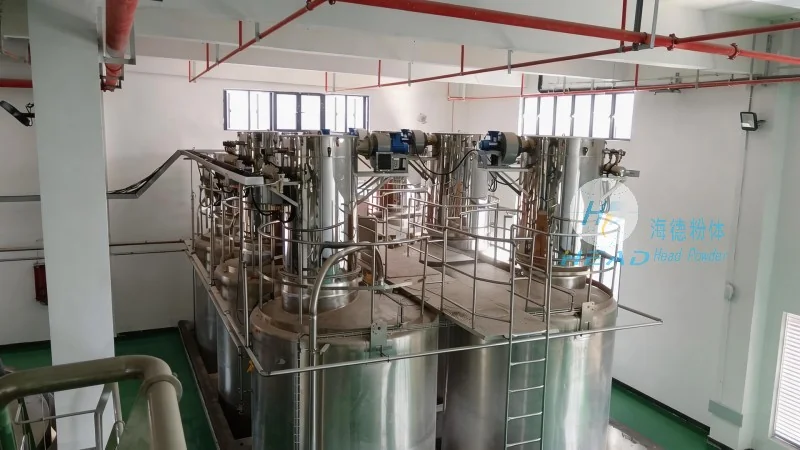
The Working Principle of the System
The core of the rice husk ash powder pneumatic conveying system operates on the principle of creating a pressure differential within the conveying line. A blower or compressor generates airflow that draws the powder from the source container into the pipeline. The system typically includes components such as a hopper, a rotary valve, a filter, and a receiver, each playing a critical role in the material transport process.
Step-by-Step Operation Process
The operation of the rice husk ash powder pneumatic conveying system involves several key steps:
- Material Loading: Rice husk ash powder is loaded into the hopper from the source container. The rotary valve controls the flow of material into the conveying line, ensuring a consistent feed rate.
- Airflow Generation: The blower or compressor starts, creating a negative pressure in the pipeline. This pressure difference draws the powder particles into the air stream.
- Conveying: The mixed powder and air travel through the pipeline to the destination receiver. The system’s design ensures minimal particle separation and efficient transport over long distances.
- Material Discharge: At the receiver, the powder is deposited into the target container. The system may include a filter to remove any fine particles from the air before it is released back into the environment.
Key Components and Their Functions
Several critical components work in tandem to ensure the smooth operation of the pneumatic conveying system:
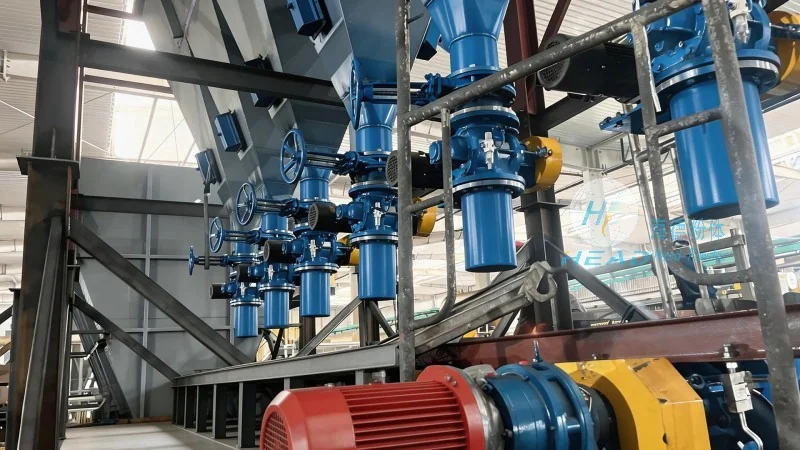
- Hopper: Stores the rice husk ash powder and provides a controlled feed to the rotary valve.
- Rotary Valve: Regulates the flow of powder from the hopper into the conveying line, preventing backflow and maintaining consistent material delivery.
- Blower/Compressor: Generates the necessary airflow to create the pressure differential and transport the powder.
- Filter: Captures fine particles from the air stream, ensuring compliance with environmental regulations and preventing contamination.
- Receiver: Collects the conveyed powder and may include a venting system to manage air pressure.
Advantages of the System
The rice husk ash powder pneumatic conveying system offers numerous benefits for industrial applications:
- Efficiency: High transport rates and minimal material loss compared to traditional methods.
- Flexibility: Ability to handle varying particle sizes and moisture content without significant performance degradation.
- Low Maintenance: Reduced wear and tear on components due to the absence of moving parts in direct contact with the powder.
- Environmental Compliance: Integrated filtration systems ensure that emissions are controlled, meeting regulatory standards.
Conclusion
HeadPowder’s rice husk ash powder pneumatic conveying system exemplifies advanced material handling technology. By understanding the operational process and working principles, industries can leverage this system to enhance productivity, reduce costs, and ensure compliance with environmental regulations. With its robust design and efficient performance, the system is a reliable solution for transporting rice husk ash powder in various industrial settings.