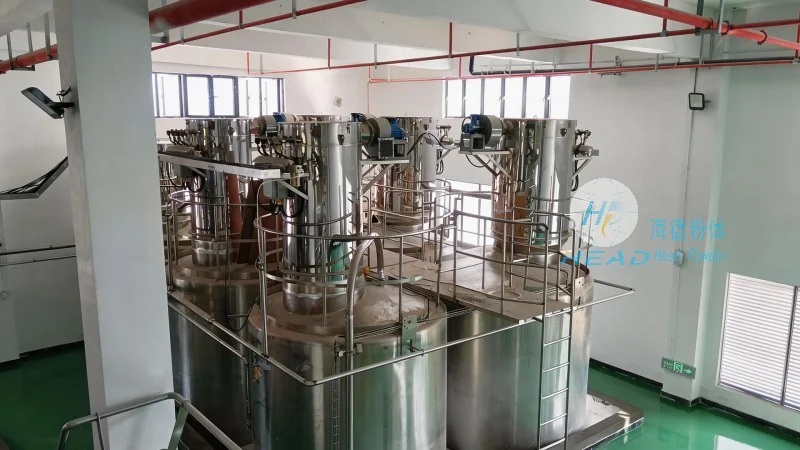
HeadPowder, a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems tailored for soda ash applications. This article provides a comprehensive overview of the soda ash pneumatic conveying equipment, focusing on its structural design and operational principles to help users understand its functionality and benefits.
Company Profile and Background
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a professional manufacturer dedicated to providing high-quality material handling equipment. With years of experience in the industry, the company has established itself as a reliable partner for clients seeking efficient and reliable solutions for bulk material transport. The company's commitment to innovation and customer satisfaction has enabled it to develop cutting-edge pneumatic conveying systems that meet the stringent requirements of the soda ash industry.
Understanding Soda Ash Pneumatic Conveying Equipment
Soda ash, also known as sodium carbonate, is a widely used chemical in various industrial processes, including glass manufacturing, paper production, and water treatment. The efficient and safe transport of soda ash is crucial for maintaining production efficiency and ensuring product quality. Pneumatic conveying equipment offers a solution to this challenge by utilizing air to move bulk materials through a closed system, eliminating the need for traditional mechanical conveying methods that may cause dust, contamination, or material degradation.
Key Components and Structural Design
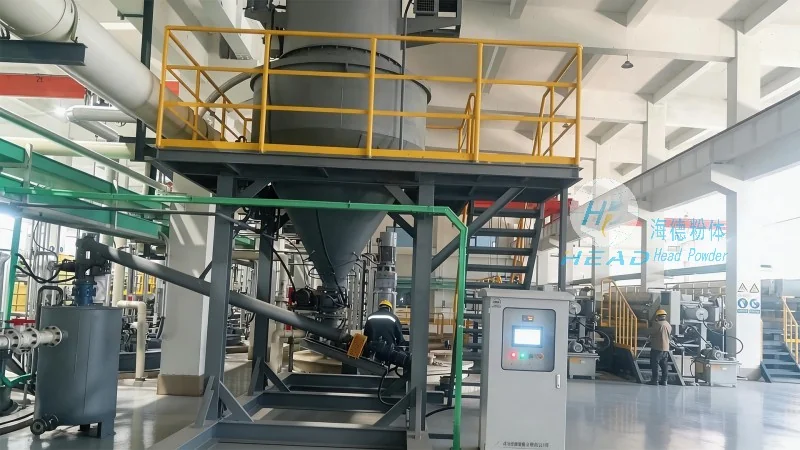
The soda ash pneumatic conveying system typically consists of several key components that work in harmony to achieve effective material transport. The main components include the hopper, feeder, air compressor, conveying line, and receiver. The hopper is designed to store the soda ash and provide a consistent feed to the feeder. The feeder ensures a controlled and steady flow of material into the conveying line, preventing blockages and maintaining system efficiency. The air compressor generates the necessary air pressure to move the material through the pipeline. The conveying line, often made of stainless steel or other corrosion-resistant materials, is designed to withstand the chemical properties of soda ash and ensure durability. The receiver collects the conveyed material and discharges it into the next processing stage.
Working Principle of the Conveying Process
The operation of the soda ash pneumatic conveying equipment follows a systematic process. Initially, the soda ash is stored in the hopper. The feeder then meters the material at a controlled rate into the conveying line. Simultaneously, the air compressor supplies compressed air into the line, creating a flow that propels the material forward. The combination of air and material creates a slurry-like mixture that travels through the pipeline to the receiver. The receiver, equipped with a dust collection system, captures any fine particles and returns them to the hopper for reprocessing. This closed-loop system ensures minimal material loss and maintains a clean working environment.
Advantages of Pneumatic Conveying for Soda Ash
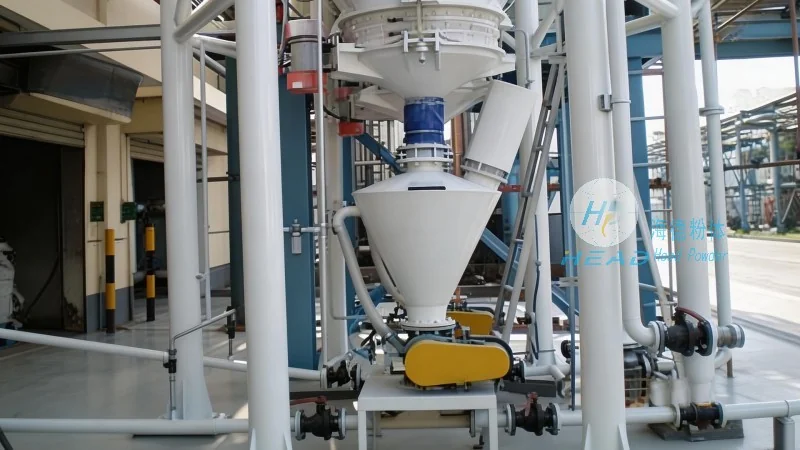
Compared to traditional conveying methods, pneumatic conveying offers several advantages for soda ash transport. Firstly, it provides a dust-free and clean operation, which is essential for maintaining product purity and meeting environmental regulations. Secondly, the system is highly flexible, allowing for changes in material flow rates and destinations without significant modifications. Thirdly, it reduces the risk of material degradation due to minimal contact with equipment surfaces and reduced handling. Additionally, the closed system enhances safety by preventing exposure to harmful dust and fumes, contributing to a healthier workplace.
Application Scenarios and Customization
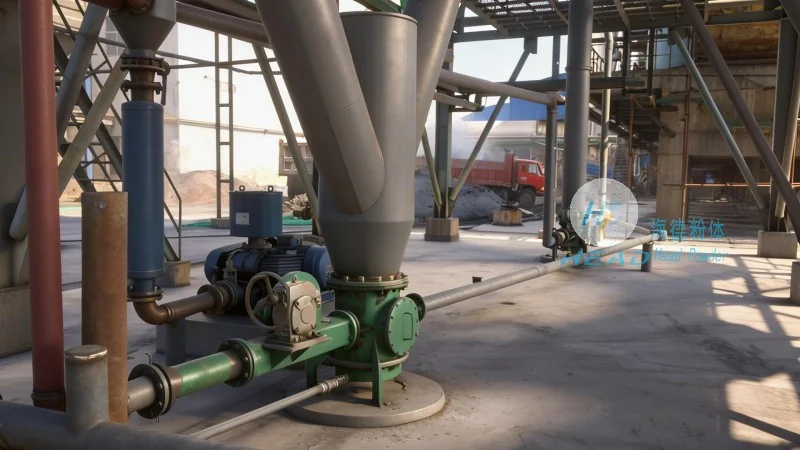
The soda ash pneumatic conveying equipment is suitable for various applications within the chemical and industrial sectors. It is commonly used in soda ash production plants, where it facilitates the transport of raw materials and finished products between different processing stages. The system can also be integrated into downstream processes such as packaging and storage, ensuring a seamless flow of materials. HeadPowder offers customized solutions tailored to specific client needs, including different conveying capacities, pipeline configurations, and material handling requirements. The company's engineering team works closely with clients to design systems that optimize performance and meet operational goals.
Conclusion and Company Commitment
In conclusion, the soda ash pneumatic conveying equipment is a sophisticated and efficient solution for bulk material transport in the soda ash industry. Its structural design and working principles ensure reliable operation, while its advantages in dust control, flexibility, and safety make it a preferred choice for many industrial applications. HeadPowder Engineering Co., Ltd., with its expertise and commitment to quality, continues to provide innovative and reliable pneumatic conveying systems that enhance productivity and operational efficiency for its clients. By leveraging advanced technology and customer-centric approach, HeadPowder remains at the forefront of material handling solutions, supporting the growth and success of the soda ash industry.




