For industrial applications requiring efficient and reliable handling of bulk powders, the automatic bulk powder bag opening and powder handling system offers a comprehensive solution. This system is engineered to streamline the process of unpacking, conveying, and managing powder materials, ensuring high efficiency and minimal waste. The following sections will provide an overview of the system's structure and working principles, highlighting its key components and operational mechanisms.
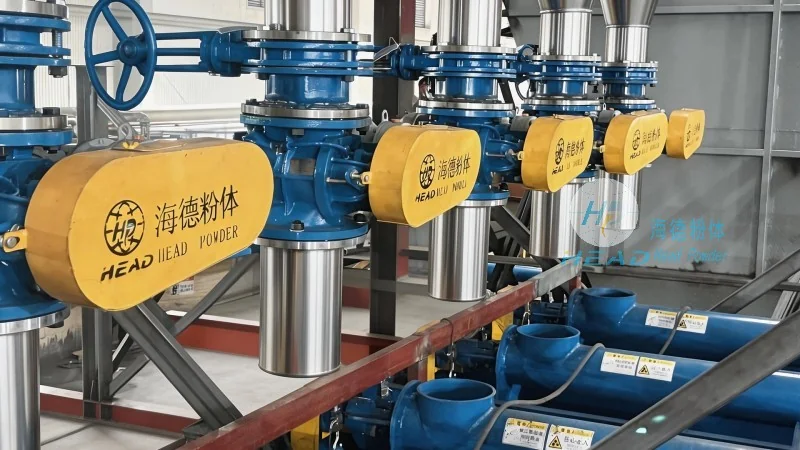
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer of this advanced powder handling system, is a leading enterprise based in Shandong, China. With a strong commitment to innovation and quality, the company specializes in the design, development, and production of industrial powder processing equipment. The company's headquarters is located in Shandong, China, where it leverages advanced technology and expertise to deliver reliable solutions for various industrial sectors.
System Structure and Key Components
The automatic bulk powder bag opening and powder handling system comprises several integrated components that work in concert to achieve efficient powder processing. The primary components include a bag opening mechanism, a powder conveying system, a dust collection unit, and a control panel. Each component is meticulously engineered to ensure optimal performance and durability in industrial environments.
The bag opening mechanism is designed to safely and efficiently open bulk powder bags without causing spillage or contamination. It typically features a mechanical or pneumatic system capable of handling various bag sizes and materials, such as polyethylene or paper. This component ensures that the powder is released smoothly into the conveying system, minimizing the risk of material loss.
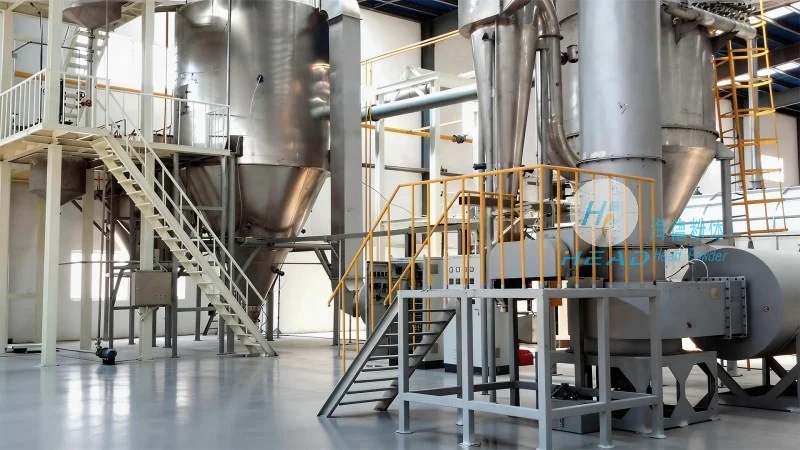
The powder conveying system is the core of the handling process, responsible for transporting the powder from the bag opening unit to the storage or processing equipment. It may utilize air-based systems, such as pneumatic conveying, or mechanical systems, like screw conveyors, depending on the specific application requirements. The system is designed to maintain consistent flow rates and prevent clogging, ensuring reliable operation.
The dust collection unit is an essential part of the system, designed to capture and filter airborne particles during the powder handling process. This unit helps maintain a clean and safe working environment by preventing dust accumulation and ensuring compliance with industrial safety standards. The filtration system typically includes high-efficiency particulate air (HEPA) filters or other advanced filtration technologies to ensure effective dust removal.
The control panel is equipped with user-friendly interfaces and monitoring systems that allow operators to control and monitor the entire process. It may include sensors, indicators, and adjustable settings to optimize the system's performance based on the specific powder characteristics and handling requirements. The control panel ensures that the system operates efficiently and safely, reducing the risk of operational errors.
Working Principle of the System
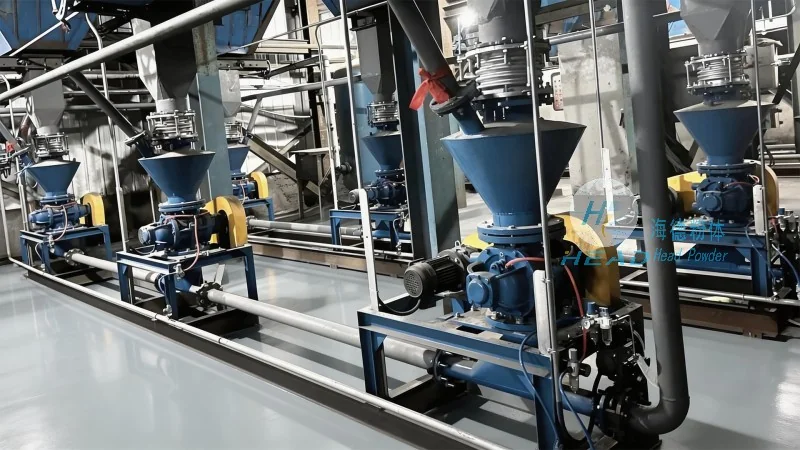
The operation of the automatic bulk powder bag opening and powder handling system follows a sequential process that ensures efficient and controlled powder handling. The system begins with the placement of a bulk powder bag into the bag opening mechanism. The mechanism then activates, opening the bag and allowing the powder to flow into the conveying system. The powder is then transported through the conveying system to the desired destination, such as a silo or processing equipment.
During the operation, the dust collection unit continuously captures any airborne particles, ensuring a clean environment. The control panel monitors the system's performance, providing real-time feedback on flow rates, pressure, and other critical parameters. Operators can adjust the system settings as needed to maintain optimal performance and prevent issues such as clogging or overloading.
The system is designed to operate continuously, with minimal downtime for maintenance or adjustments. Its automated nature reduces the need for manual intervention, increasing overall efficiency and productivity. The integration of advanced technologies, such as sensors and control systems, ensures that the system adapts to varying powder characteristics and handling conditions, providing reliable performance in diverse industrial applications.




