Green bean material handling equipment is essential for the efficient processing and transportation of green beans, which are widely utilized in food products and industrial applications. These specialized machines are engineered to move, sort, and process green beans from raw to finished goods, ensuring high productivity and quality control in production lines. Understanding the types and design principles of such equipment is vital for businesses in green bean processing, as it directly impacts operational efficiency and cost-effectiveness.
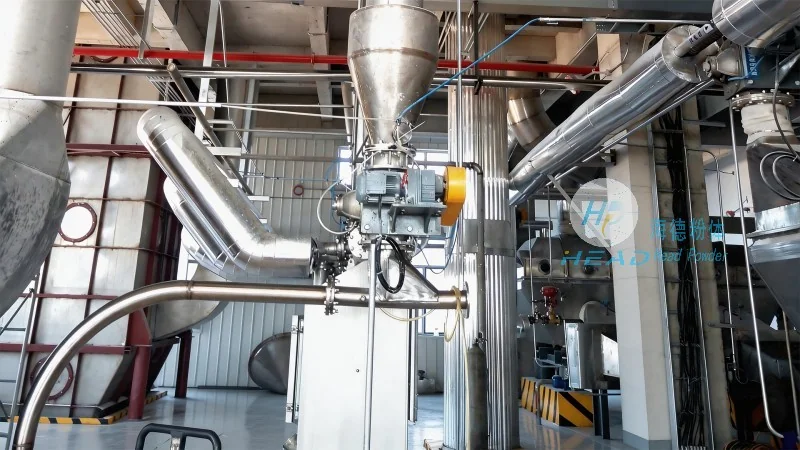
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a professional manufacturer based in Shandong, China, specializes in developing and producing advanced material handling solutions for agricultural and food processing industries. With years of experience and a commitment to innovation, HeadPowder has established itself as a trusted partner for companies seeking reliable and efficient equipment for green bean processing. The company’s headquarters is located in Shandong, China, where it leverages local resources and expertise to deliver high-quality products that meet international standards.
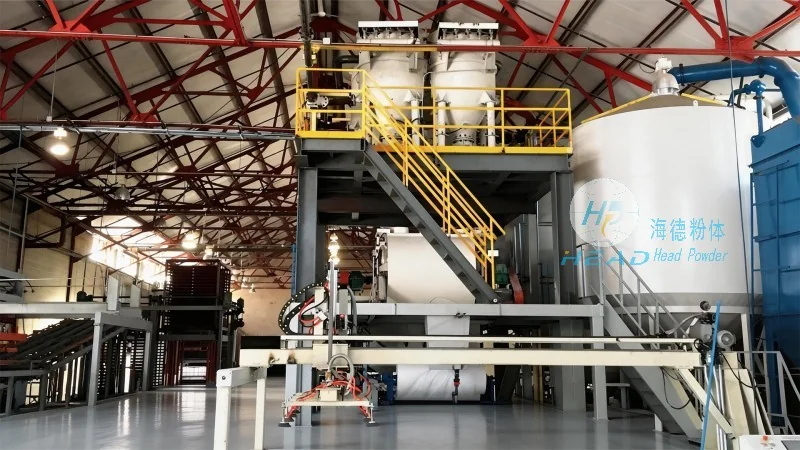
Design Principles of Green Bean Material Handling Equipment
The design of green bean material handling equipment is guided by several key principles to ensure optimal performance and durability. First, the equipment must accommodate the unique characteristics of green beans, including their size, shape, and moisture content. This involves specialized components like conveyor belts, sorting mechanisms, and cleaning systems engineered specifically for green bean processing. Second, the design prioritizes efficiency and minimal downtime, critical in high-volume production environments. Features such as automated controls, easy maintenance access, and robust construction help reduce operational costs and increase productivity. Third, the equipment is designed with hygiene and food safety in mind, adhering to strict industry standards to ensure green beans are handled in a clean and safe manner throughout processing.
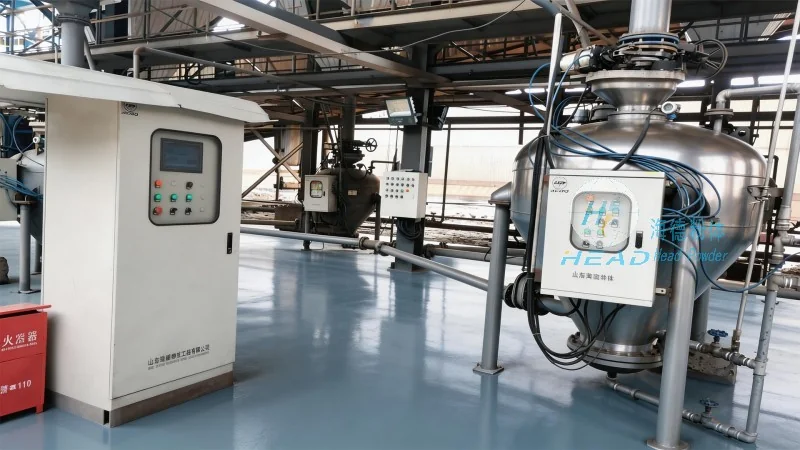
Key Components and Functionalities
Green bean material handling equipment typically consists of several key components working in tandem to achieve efficient processing. The primary components include conveyor systems, which transport green beans through various processing stages. Sorting mechanisms—such as optical or mechanical sorters—are used to separate defective or unqualified beans from high-quality ones, ensuring only premium beans proceed. Cleaning systems, including washing and drying units, remove dirt, debris, and contaminants from the green beans. Additionally, processing units like hulling or peeling machines may be integrated to remove the outer shell or skin, depending on final product requirements. Each component is designed to operate seamlessly with others, creating a streamlined production line that minimizes waste and maximizes output.
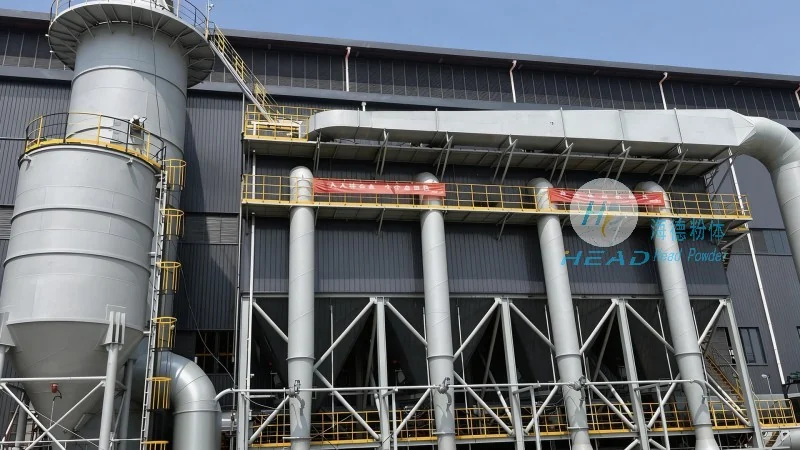
Benefits of Using Advanced Green Bean Material Handling Equipment
Investing in advanced green bean material handling equipment offers numerous advantages for businesses in the green bean processing industry. Firstly, it significantly enhances operational efficiency by automating handling and processing, reducing manual labor and human error. This leads to higher productivity and consistent product quality. Secondly, the equipment helps lower processing costs by minimizing waste and optimizing resource usage. Efficient sorting and cleaning reduce discarded material, while energy consumption is optimized. Thirdly, advanced equipment improves food safety and regulatory compliance, ensuring green beans are handled hygienically—an essential priority in the food industry. Finally, the equipment’s durability and low maintenance requirements contribute to long-term cost savings and reliable operation, making it a worthwhile investment for businesses aiming to enhance processing capabilities.




