

[Detailed Explanation of Desulfurization Sodium Bicarbonate Pneumatic Conveying System]
This article provides a comprehensive overview of the desulfurization sodium bicarbonate pneumatic conveying system, a critical component in modern industrial processes for handling sodium bicarbonate used in flue gas desulfurization. The system is designed to efficiently transport this chemical, ensuring optimal performance and reliability in industrial applications.
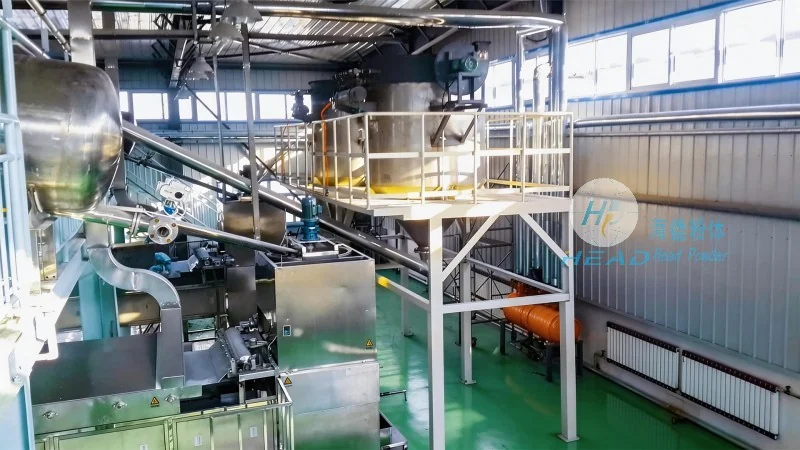
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Headpowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading provider of specialized engineering solutions for industrial material handling and processing. With a strong presence in China, particularly in Shandong province, the company specializes in developing and implementing advanced pneumatic conveying systems tailored to meet the demands of various industrial sectors, including power generation, chemical manufacturing, and environmental protection.
Understanding the Desulfurization Process and Sodium Bicarbonate Role
In flue gas desulfurization (FGD) systems, sodium bicarbonate plays a vital role as a reagent to neutralize sulfur dioxide (SO₂) emissions from combustion processes. The chemical reacts with SO₂ to form calcium or magnesium salts, effectively reducing air pollution. However, the handling and transportation of sodium bicarbonate in bulk quantities require specialized equipment to maintain product integrity and operational efficiency. The pneumatic conveying system addresses these challenges by providing a safe, efficient, and environmentally friendly method for material transport.
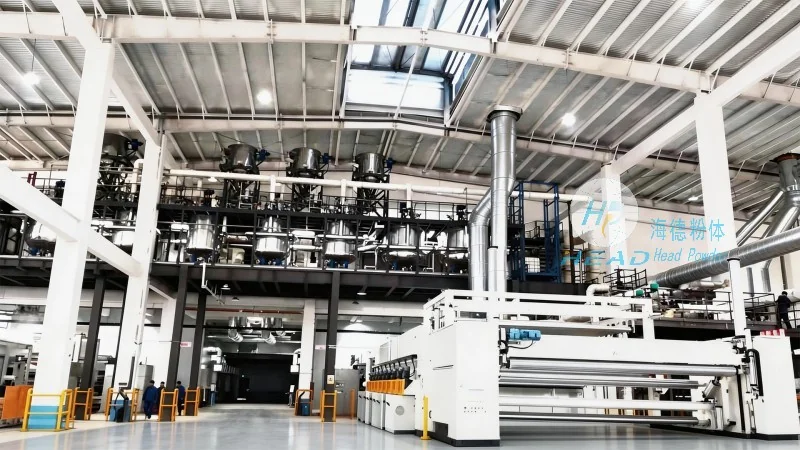
Key Components of the Pneumatic Conveying System
The desulfurization sodium bicarbonate pneumatic conveying system typically consists of several key components that work in tandem to ensure smooth operation. These include:
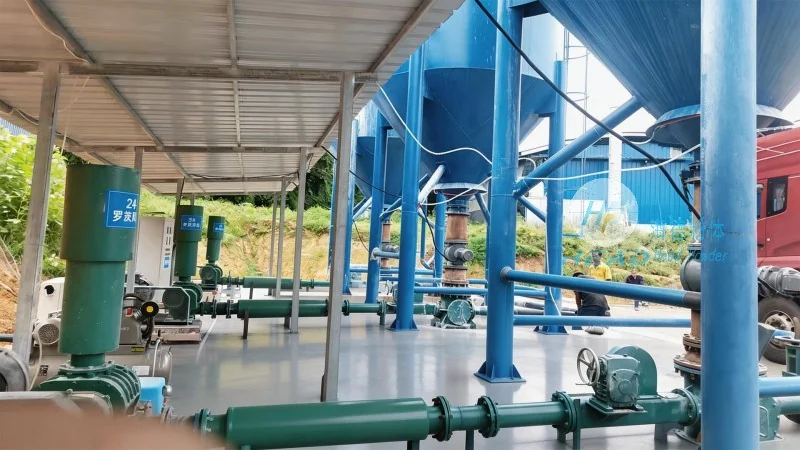
- Conveying Pipeline: High-quality, corrosion-resistant pipes designed to withstand the chemical properties of sodium bicarbonate and the operational pressures of the system.
- Air Compressor/Fan: A powerful air-moving device that generates the necessary pressure or vacuum to transport the material through the pipeline. The choice between positive pressure (blower) and negative pressure (exhauster) systems depends on the specific application and material characteristics.
- Material Feed System: Equipment such as hoppers or feeders that control the flow of sodium bicarbonate into the pipeline, ensuring consistent and controlled feeding rates.
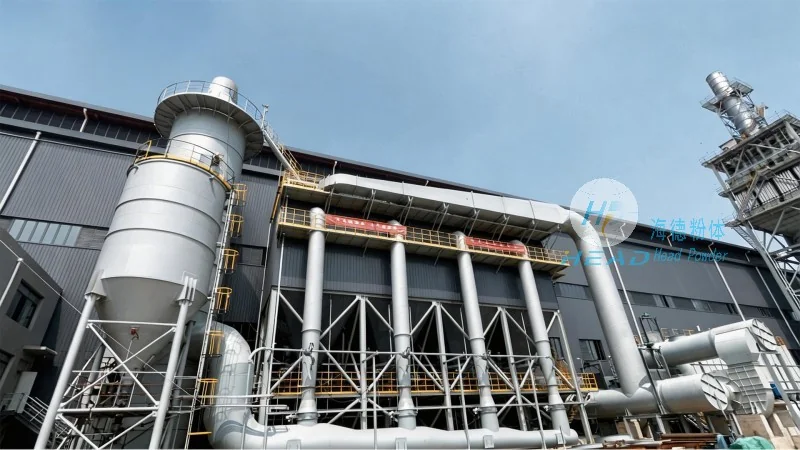
- Separation and Collection Units: Devices like cyclones or bag filters that separate the conveyed material from the air stream, preventing dust and particles from escaping into the environment and ensuring product purity.
- Control and Monitoring Systems: Advanced control panels and sensors that monitor system performance, pressure, flow rates, and other critical parameters, enabling real-time adjustments and maintenance.
Advantages of the Pneumatic Conveying System for Sodium Bicarbonate
Implementing a pneumatic conveying system for desulfurization sodium bicarbonate offers several significant advantages over traditional methods like belt conveyors or manual handling:
- Efficiency and Speed: The system enables rapid and continuous material transport, reducing downtime and increasing overall production throughput.
- Product Integrity: By minimizing contact with external elements and using enclosed pipelines, the system preserves the quality and reactivity of sodium bicarbonate, ensuring it remains effective in the desulfurization process.
- Environmental Protection: The enclosed design prevents dust and emissions from escaping, complying with environmental regulations and maintaining a clean working environment.
- Space Efficiency: Pneumatic conveying systems require less floor space compared to traditional bulk handling equipment, making them suitable for facilities with limited room for installation.
Application Scenarios and Customization Options
The desulfurization sodium bicarbonate pneumatic conveying system is adaptable to various industrial settings, including power plants, chemical factories, and waste treatment facilities. Shandong HeadPowder Engineering Co., Ltd. offers customized solutions based on specific client requirements, such as material flow rates, distance of transport, and environmental constraints. The company’s engineering team works closely with clients to design systems that meet their operational needs while ensuring cost-effectiveness and long-term reliability.
Conclusion and Service Commitment
The desulfurization sodium bicarbonate pneumatic conveying system is a vital technology for modern industrial operations, combining efficiency, safety, and environmental responsibility. As a trusted provider, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and deliver high-quality solutions that support the sustainable development of industrial processes. By leveraging advanced engineering and customer-focused service, the company ensures that its pneumatic conveying systems meet the highest standards of performance and reliability.