When it comes to transporting sodium bicarbonate, the choice of conveying system can significantly impact operational efficiency, safety, and cost-effectiveness. Pneumatic conveying systems have emerged as a reliable solution for handling this chemical, offering various types tailored to different industrial needs. This article explores the different types of pneumatic conveying systems used in sodium bicarbonate transport and their practical applications.
Overview of Pneumatic Conveying Systems for Sodium Bicarbonate
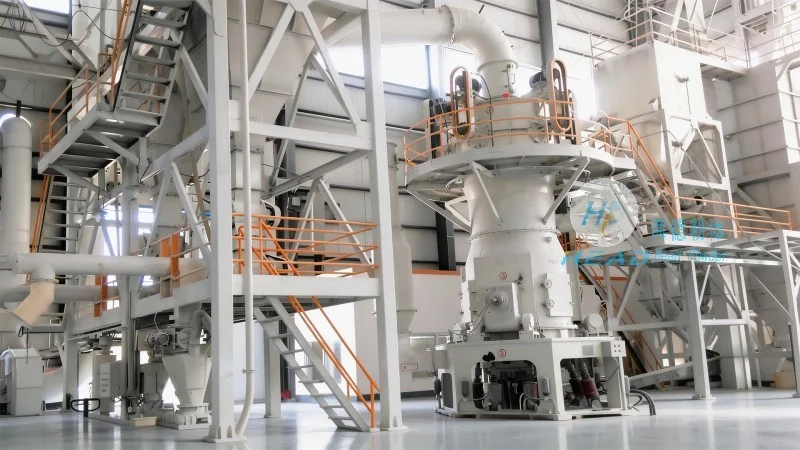
Pneumatic conveying systems utilize air or gas to move bulk materials like sodium bicarbonate from one location to another. These systems are particularly advantageous for sodium bicarbonate due to its light weight and potential dustiness, as they can handle the material without direct contact, reducing the risk of contamination and equipment wear. The primary goal is to ensure a smooth, efficient, and safe transfer process, which is critical in industrial settings where sodium bicarbonate is used in various applications, including food processing, pharmaceuticals, and chemical manufacturing.
Types of Pneumatic Conveying Systems
There are two main categories of pneumatic conveying systems: positive pressure and negative pressure systems. Each type has distinct characteristics and is suitable for different scenarios.
Positive Pressure Systems
Positive pressure systems operate by blowing air or gas into the conveying line, creating a pressure higher than the ambient air pressure. This method is effective for long-distance and high-capacity transport. In the context of sodium bicarbonate, positive pressure systems are often used when the material needs to be conveyed over considerable distances or when multiple delivery points are required. The system pushes the material forward, ensuring consistent flow and minimizing the risk of blockages. This type of system is particularly beneficial for large-scale operations where continuous and reliable transport is essential.
Negative Pressure Systems
Negative pressure systems, also known as vacuum systems, operate by creating a vacuum in the conveying line, drawing the material into the system. This approach is ideal for short-distance transport and when the material is to be collected from multiple sources. For sodium bicarbonate, negative pressure systems are commonly used in applications where the material is to be collected from storage silos or hoppers and transported to processing units. The vacuum helps in maintaining a clean and controlled environment, preventing dust dispersion and ensuring compliance with safety regulations.
Practical Applications in Industrial Settings
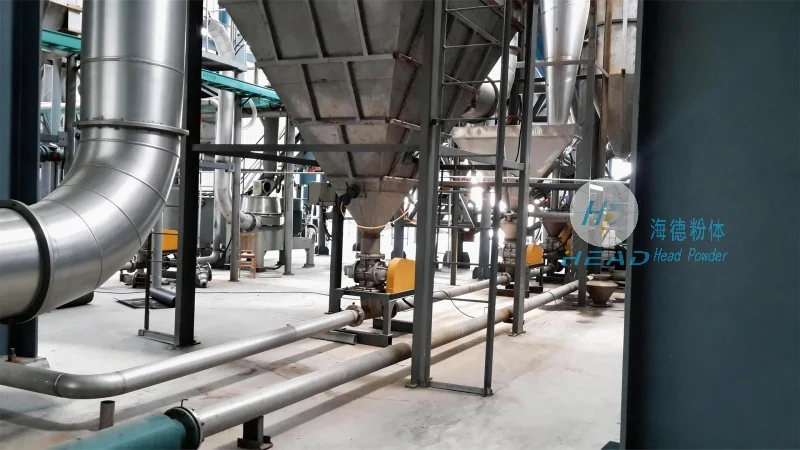
The practical application of pneumatic conveying systems for sodium bicarbonate varies based on the specific requirements of the industry. In food processing facilities, for instance, the system must meet stringent hygiene standards, ensuring that the material remains free from contaminants. This is achieved through the use of stainless steel components and sealed systems, which are common in modern pneumatic conveying solutions. Similarly, in pharmaceutical manufacturing, the system must adhere to GMP (Good Manufacturing Practice) guidelines, emphasizing cleanliness and material integrity.
In chemical manufacturing, the focus is on efficiency and scalability. Pneumatic conveying systems can handle large volumes of sodium bicarbonate, making them suitable for production lines that require continuous material flow. The ability to integrate with existing production equipment is another key advantage, as it allows for seamless integration without disrupting the overall workflow. This integration capability is crucial for maintaining high production rates and minimizing downtime.
Key Considerations for Selecting a Pneumatic Conveying System
When selecting a pneumatic conveying system for sodium bicarbonate transport, several factors must be considered to ensure optimal performance and cost-effectiveness. These include the material's properties, such as its bulk density, flowability, and dustiness, as well as the distance and number of delivery points. The system's capacity and pressure requirements are also critical, as they directly impact the system's design and operational costs.
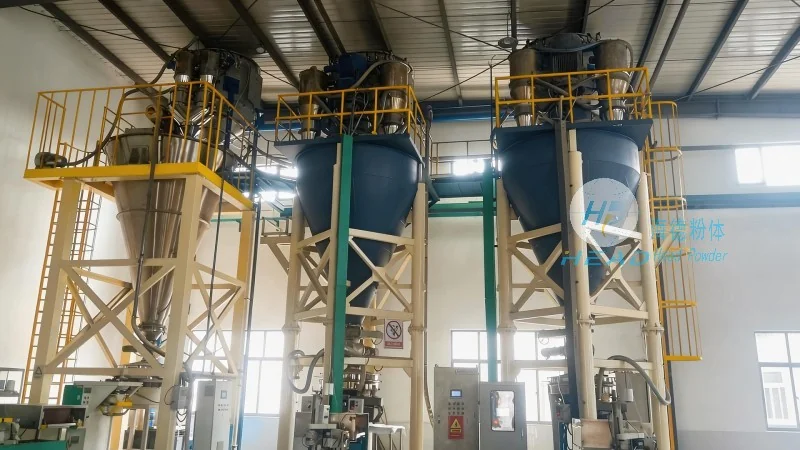
Another important consideration is the environmental impact and safety aspects. Pneumatic conveying systems should be designed to minimize dust emissions and comply with local regulations. This may involve the use of filtration systems and proper ventilation to maintain a safe working environment. Additionally, the system's maintenance requirements and long-term reliability should be evaluated to ensure it meets the operational needs of the facility.
About HeadPowder: Your Partner in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of specialized pneumatic conveying systems tailored for sodium bicarbonate and other bulk materials. With years of experience in the industry, HeadPowder offers customized solutions that address the unique challenges of each application. The company's expertise lies in designing and manufacturing systems that are efficient, reliable, and compliant with industry standards.
HeadPowder's team of engineers and technicians work closely with clients to understand their specific needs and provide tailored solutions. Whether it's a positive pressure or negative pressure system, the company ensures that the equipment is designed to handle the material's properties and operational requirements. The company's commitment to quality and customer satisfaction has made it a trusted partner for many industrial facilities worldwide.
With its headquarters in Shandong, China, HeadPowder serves clients globally, providing comprehensive support from system design and installation to maintenance and troubleshooting. The company's focus on innovation and customer service ensures that clients receive the best possible solutions for their sodium bicarbonate transport needs.




