

Introduction to Ammonia Fertilizer Pneumatic Conveying and the Working Principle of Pneumatic Convey
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier specializing in pneumatic conveying systems, particularly for ammonia fertilizer applications. With its headquarters located in Shandong, China, the company has established itself as a leading provider of efficient and reliable solutions for material handling in the fertilizer industry.
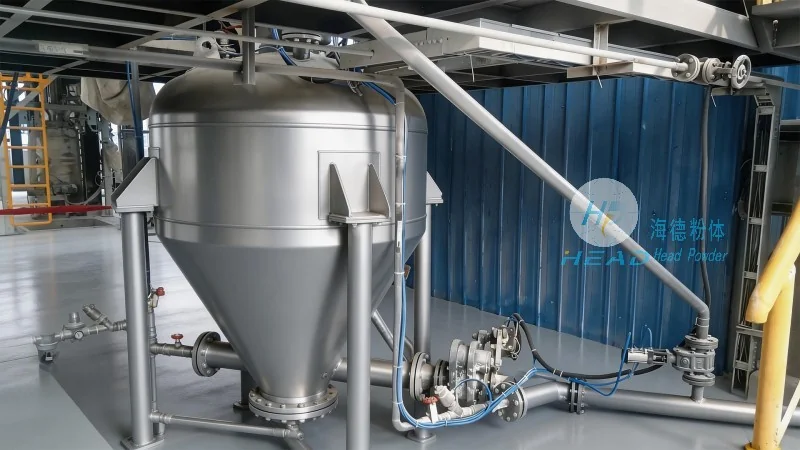
Overview of Ammonia Fertilizer Pneumatic Conveying Systems
Ammonia fertilizer, a critical component in modern agriculture, requires specialized handling equipment to ensure safe and efficient transport from production facilities to storage or distribution points. Pneumatic conveying systems offer a versatile and effective method for moving these materials, which are often in powder or granular form. These systems utilize air or other gases to transport the fertilizer through a network of pipes, eliminating the need for mechanical components like belts or buckets that might be prone to wear and tear or contamination.
The Working Principle of Pneumatic Conveying Systems
The core of a pneumatic conveying system is the ability to create a flow of air that can carry the fertilizer particles. This is achieved through a combination of components, including a blower or compressor, a hopper for material storage, a feed mechanism to introduce the fertilizer into the system, and a series of pipes that guide the material to its destination. The system operates by generating a pressure differential: either positive pressure, where air is forced through the system, or negative pressure, where air is drawn out, creating a vacuum that pulls the material along. In the case of ammonia fertilizer, positive pressure systems are commonly used due to the need to maintain a safe environment and prevent the release of hazardous gases.
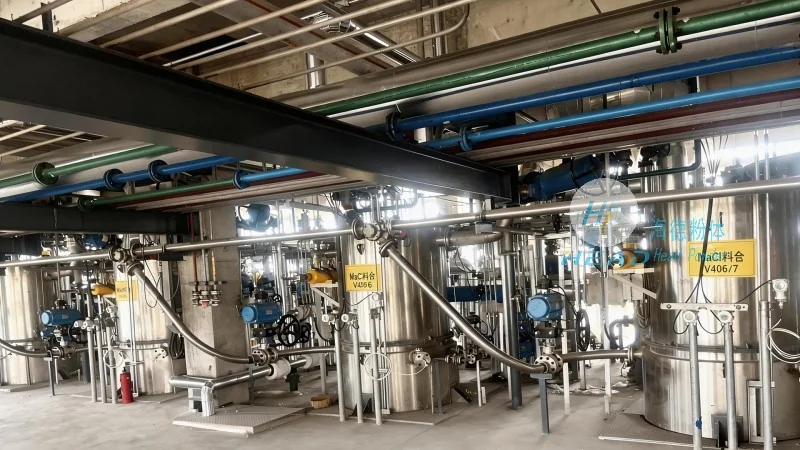
Key Components and Their Functions
Several key components work together to ensure the smooth operation of a pneumatic conveying system for ammonia fertilizer. The blower or compressor provides the necessary air pressure, typically ranging from low to high pressure depending on the system's capacity and the distance the material needs to travel. The hopper serves as a storage container, often equipped with a discharge valve to control the flow of fertilizer into the system. The feed mechanism, such as a rotary valve or a star feeder, regulates the amount of material introduced into the air stream, preventing overloading and ensuring consistent flow. The pipes, usually made of stainless steel or other corrosion-resistant materials, are designed to withstand the abrasive nature of the fertilizer and the pressure of the air. Additionally, filters and cyclones are used to separate the fertilizer from the air, ensuring that the material is delivered to the destination without contamination and that the air is cleaned before being released back into the environment.
Advantages of Pneumatic Conveying for Ammonia Fertilizer
Implementing a pneumatic conveying system for ammonia fertilizer offers several advantages over traditional methods. First, it provides a closed system, which is crucial for maintaining safety and preventing the release of ammonia gas into the environment. This not only protects workers from exposure to hazardous substances but also ensures compliance with environmental regulations. Second, the system is highly efficient in terms of energy use, as it can transport large quantities of material with relatively low power consumption compared to other methods. Third, it offers flexibility in terms of layout, as the pipes can be arranged in various configurations to suit the specific needs of a facility, allowing for easy expansion or modification as production needs change. Finally, the system reduces labor costs by automating the material handling process, minimizing the need for manual handling and reducing the risk of accidents or injuries.
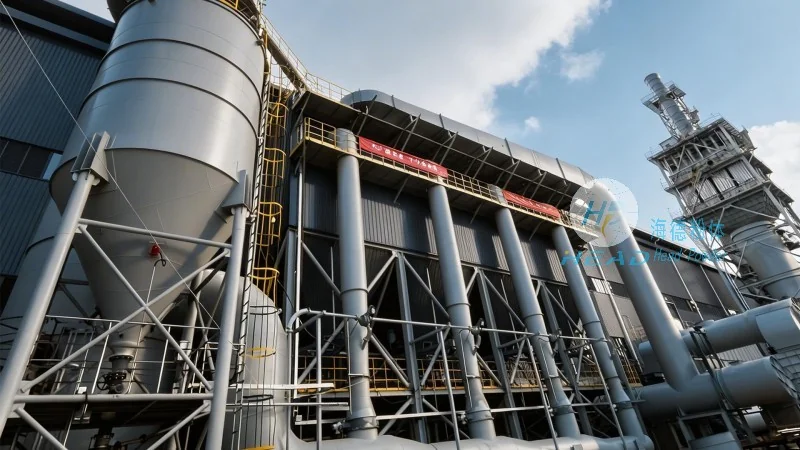
Applications and Use Cases
Pneumatic conveying systems are widely used in the fertilizer industry for various applications involving ammonia fertilizer. These include transporting raw materials from storage silos to processing plants, moving finished products from production lines to packaging areas, and delivering fertilizer to storage tanks or loading docks for distribution. The systems are also used in bulk handling operations, where large quantities of fertilizer need to be moved over long distances, such as from a manufacturing facility to a port for export. In addition, the systems can be integrated with other equipment, such as mixers and granulators, to form a complete production line, enhancing overall operational efficiency.
Conclusion and Company Commitment
As a leading manufacturer of pneumatic conveying systems, Shandong HeadPowder Engineering Co., Ltd. is committed to providing high-quality, reliable solutions for the handling of ammonia fertilizer. By leveraging advanced technology and a deep understanding of the fertilizer industry's needs, the company ensures that its systems are designed to meet the specific requirements of each client, whether it's for small-scale operations or large industrial facilities. With its headquarters in Shandong, China, HeadPowder continues to innovate and improve its products to deliver the best possible performance and safety for its customers. The company's dedication to quality and customer satisfaction has established it as a trusted partner in the global fertilizer industry, offering solutions that enhance efficiency, safety, and sustainability in material handling.