Sugar material handling refers to the processes and systems used to transport, store, and manage bulk sugar from its raw form to various processing stages or final distribution. This involves a range of equipment and methodologies tailored to the unique properties of sugar, such as its granular structure, hygroscopic nature, and the need for efficient, hygienic handling to maintain product quality. Effective sugar material handling is crucial for optimizing production efficiency, ensuring product integrity, and meeting regulatory standards in the sugar industry.
Key Design Principles for Sugar Material Handling Systems
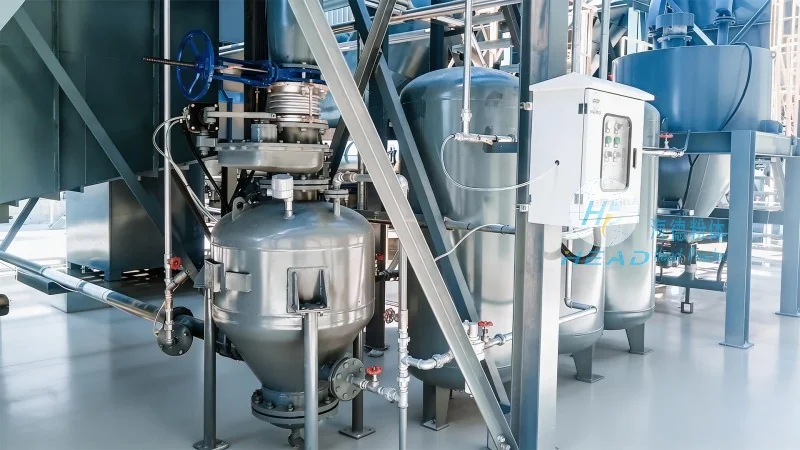
The design of sugar material handling systems follows several critical principles to ensure safety, efficiency, and product quality. First, hygiene and sanitation are paramount, as sugar is a food product and must be handled in compliance with food safety regulations. This includes the use of stainless steel equipment, smooth surfaces, and easy-to-clean designs to prevent contamination. Second, material flow optimization is essential to minimize energy consumption and reduce handling losses. This involves designing a logical flow from raw sugar storage to processing lines, using gravity feed where possible and mechanical conveyors for longer distances. Third, flexibility and adaptability are important to accommodate different sugar types (e.g., raw sugar, refined sugar, sugar syrups) and varying production volumes. Systems should be modular and scalable to adapt to changing production needs. Fourth, maintenance and reliability are critical to ensure continuous operation. Components like conveyors, elevators, and storage silos must be durable and require minimal downtime for maintenance.
HeadPowder Engineering: Expertise in Sugar Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial engineering solutions, specializes in designing and manufacturing custom sugar material handling systems. With headquarters in Shandong, China, HeadPowder has extensive experience in the sugar industry, working with clients to develop tailored solutions that meet their specific operational requirements. The company’s team of engineers and technicians leverages advanced technology and industry best practices to create efficient, reliable, and cost-effective systems. HeadPowder’s approach focuses on understanding the unique challenges of sugar handling, such as dust control, moisture management, and product separation, and addresses these through innovative design and high-quality materials.
Common Equipment in Sugar Material Handling Systems
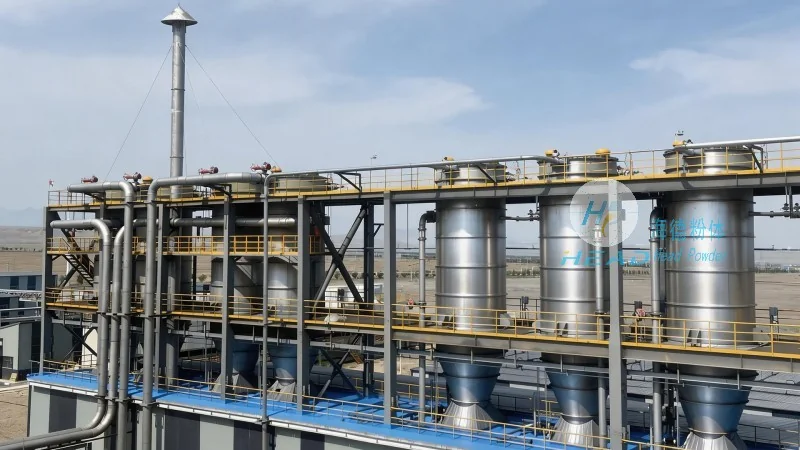
Sugar material handling systems typically include a variety of equipment to handle different stages of the process. Conveyors are a primary component, used to transport sugar from storage silos to processing lines or packaging areas. Screw conveyors are commonly used for horizontal or slight incline transport due to their ability to handle bulk materials without spillage. Belt conveyors are suitable for longer distances and higher capacities, while bucket elevators are used for vertical transport, efficiently lifting sugar from lower to upper levels. Storage silos are essential for storing raw or processed sugar, providing a controlled environment to maintain product quality and prevent contamination. These silos are often equipped with aeration systems to control moisture and prevent caking. Screening and separation equipment may also be included to remove impurities or separate different sugar grades, ensuring that only high-quality material proceeds to the next stage. Additionally, loading and unloading systems are used to transfer sugar between trucks, ships, or other storage facilities, facilitating smooth logistics operations.
System Layout and Flow Optimization
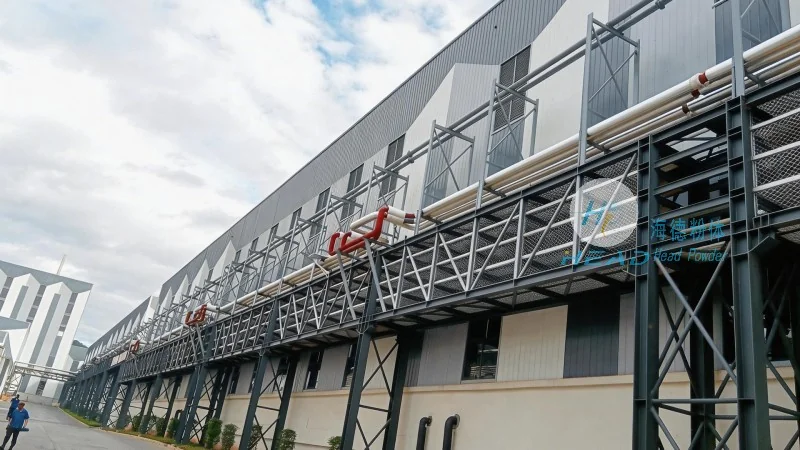
The layout of a sugar material handling system is critical to its overall efficiency. A well-designed system minimizes the distance between storage, processing, and packaging areas, reducing energy consumption and handling time. The flow is typically designed to follow a logical sequence: raw sugar is stored in a silo, then conveyed to a processing line where it is refined or processed into other products. The processed sugar is then stored in another silo before being packaged and shipped. This linear flow reduces the need for multiple transfers and minimizes the risk of cross-contamination. Additionally, the system should be designed to accommodate future expansion, allowing for additional storage or processing capacity as production needs grow. HeadPowder Engineering specializes in creating these optimized layouts, ensuring that each component is positioned to maximize efficiency and minimize downtime.
Quality Control and Safety in Sugar Material Handling
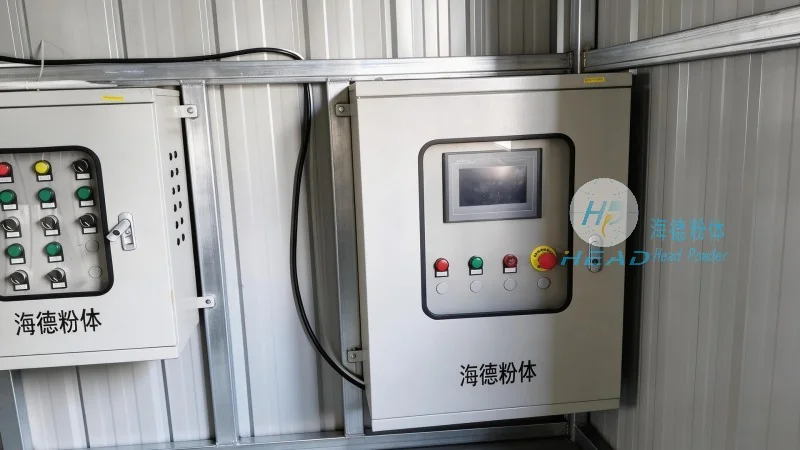
Quality control is a top priority in sugar material handling, as any contamination or quality issues can impact the final product and brand reputation. Systems are designed with features to monitor and control moisture levels, temperature, and particle size, ensuring that the sugar meets the required specifications. Sensors and monitoring systems are integrated into the equipment to provide real-time data on process parameters, allowing operators to make adjustments as needed. Safety is also a critical consideration, with systems incorporating features such as emergency stop buttons, protective guards, and dust suppression systems to prevent accidents and protect workers. HeadPowder Engineering adheres to strict safety and quality standards, ensuring that all equipment is compliant with industry regulations and designed to minimize risks.
Conclusion: The Importance of Effective Sugar Material Handling
Effective sugar material handling is essential for the success of any sugar production operation. By following key design principles, using appropriate equipment, and optimizing system layout, companies can improve efficiency, maintain product quality, and ensure compliance with regulations. Shandong HeadPowder Engineering Co., Ltd. offers expert solutions in this area, leveraging its experience and expertise to help clients achieve their operational goals. Whether it’s a new installation or an upgrade to an existing system, HeadPowder provides tailored solutions that meet the unique needs of the sugar industry, ensuring long-term success and profitability.




