For industrial applications involving sulfur tablet powders, efficient and reliable material handling is crucial. The pneumatic conveying system designed by Shandong HeadPowder Engineering Co., Ltd. (headpowder) addresses these needs by providing a sophisticated solution for transporting sulfur tablet powders. This article explores the working principle and key features of this system, highlighting its benefits and technical advantages.
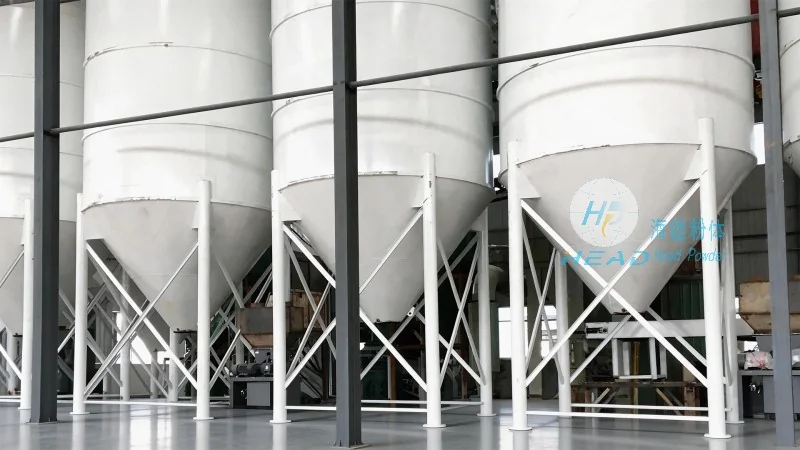
Overview of the Sulfur Tablet Powder Pneumatic Conveying System
The system developed by headpowder is engineered to handle sulfur tablet powders with precision and efficiency. It integrates advanced pneumatic technology to ensure smooth material transport from storage to processing units. By leveraging air as the conveying medium, the system minimizes the need for mechanical components, reducing maintenance requirements and operational costs. This approach is particularly advantageous for handling powders that are prone to dust or require controlled dispersion during transport.
Working Principle of the Pneumatic Conveying System
The core mechanism of the sulfur tablet powder pneumatic conveying system operates on the principle of air flow and pressure differentials. The process begins with the loading of sulfur tablet powders into a hopper or storage bin. An air compressor then generates a high-pressure air stream, which is introduced into the conveying line. As the air flows through the system, it creates a negative pressure zone that draws the powder particles into the air stream. The mixture of air and powder travels through the pipeline to the destination point, such as a processing or storage area. At the receiving end, a separator or cyclone separates the powder from the air, allowing the powder to be deposited while the air is either recirculated or vented.
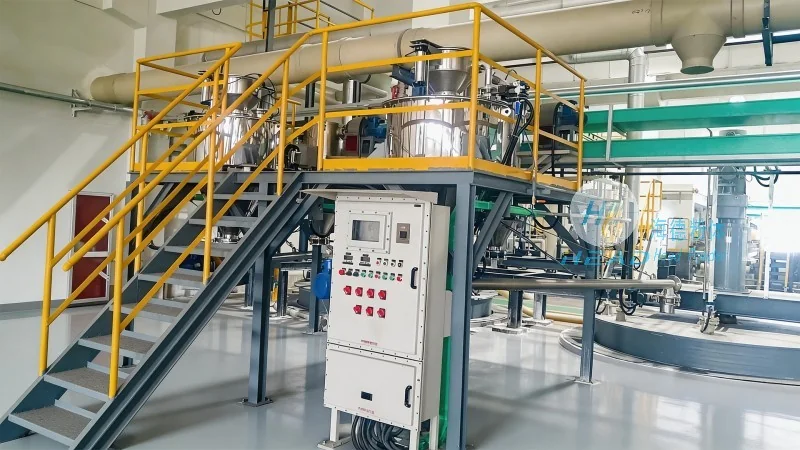
Key Features and Technical Advantages
Several distinct features set the headpowder pneumatic conveying system apart in the industry. Firstly, its design ensures high efficiency in material transport, with minimal loss of powder during transit. The system is equipped with adjustable air flow controls, enabling operators to optimize the conveying rate based on the specific characteristics of the sulfur tablet powder. This flexibility is critical for maintaining consistent product quality and preventing clogging or blockages in the pipeline.
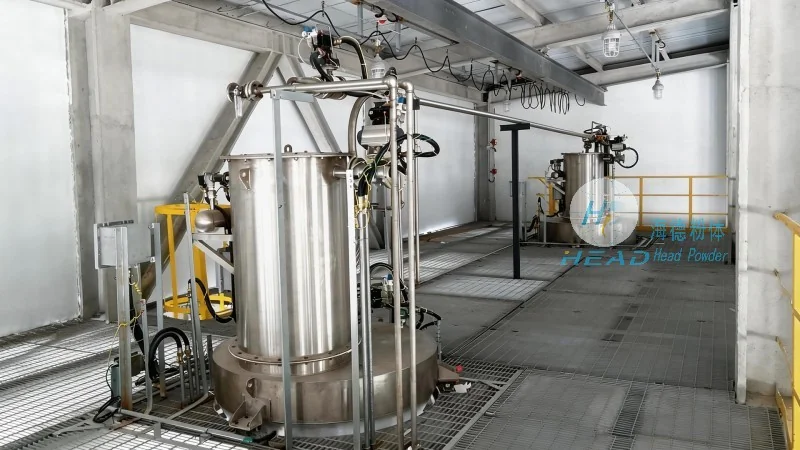
Secondly, the system incorporates advanced filtration and dust control measures. The air separation unit effectively captures fine powder particles, preventing dust emissions and ensuring compliance with environmental regulations. This feature not only enhances safety in the workplace but also protects downstream equipment from contamination. Additionally, the system's modular design allows for easy integration with existing industrial setups, reducing installation time and complexity.
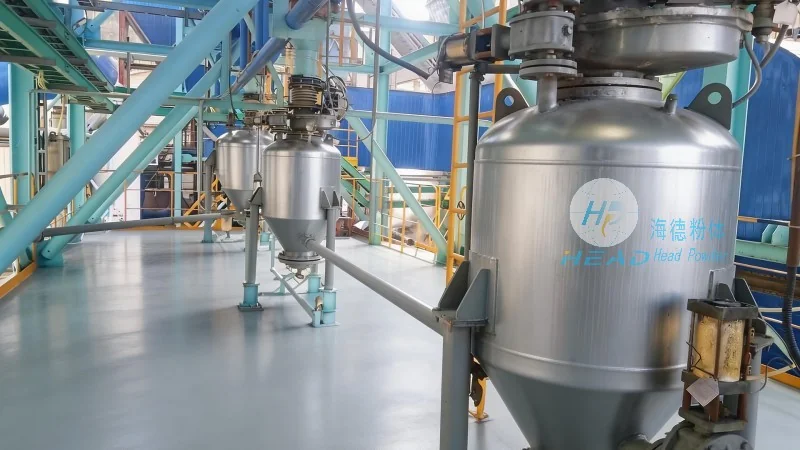
Benefits for Industrial Applications
The implementation of the sulfur tablet powder pneumatic conveying system by headpowder offers significant benefits for various industrial sectors. By streamlining the material handling process, it improves overall production efficiency and reduces downtime. The system's ability to handle powders with varying particle sizes and moisture content makes it versatile for different applications. Furthermore, the reduced reliance on manual handling minimizes the risk of workplace accidents and improves worker safety. The long-term operational cost savings, including lower maintenance and energy consumption, contribute to the system's economic viability.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. has developed a robust and efficient pneumatic conveying system tailored for sulfur tablet powders. By understanding the working principle and leveraging key features such as adjustable air flow, advanced filtration, and modular design, this system addresses the challenges of handling powders in industrial settings. With its headquarters in Shandong, China, headpowder continues to innovate in material handling solutions, providing reliable and sustainable options for industries that require precise and efficient powder transport. The system's performance and adaptability make it a valuable asset for any operation dealing with sulfur tablet powders.




