Denitrizer powder pneumatic conveying systems are critical components in industrial processes, particularly in facilities that handle nitrogen oxide reduction agents. These systems efficiently transport fine powders like denitrizer over long distances or within complex plant layouts. The technology behind such systems combines pneumatic principles with mechanical design to ensure reliable and efficient material handling.
Working Principle of Denitrizer Powder Pneumatic Conveying Systems
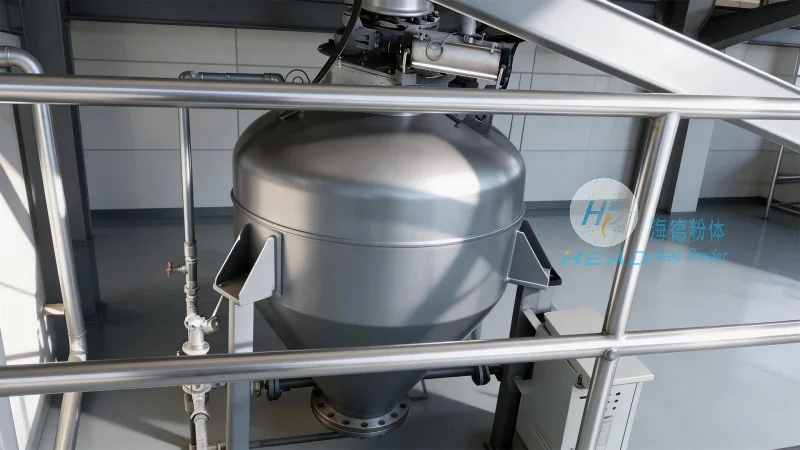
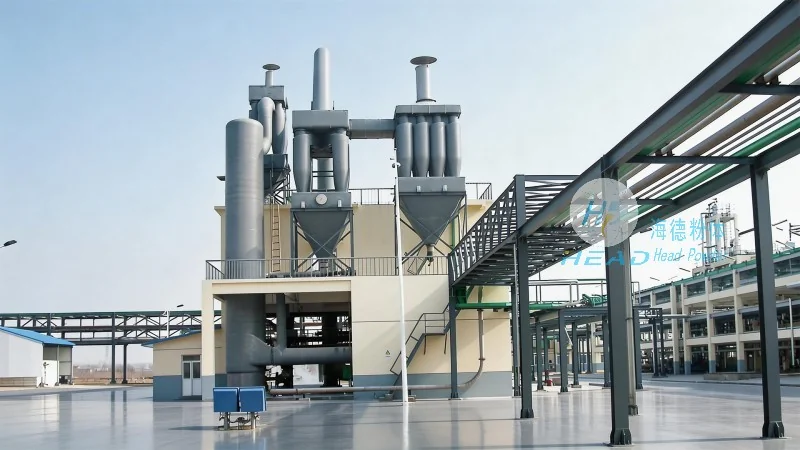
The core mechanism of a denitrizer powder pneumatic conveying system involves the use of compressed air or gas to move particulate materials through a pipeline network. The system typically operates on the principle of creating a pressure differential between the material source and the discharge point. When the system is activated, compressed air is introduced into the hopper or feed section, where it lifts the denitrizer powder particles and propels them through the pipeline. The velocity of the air and the particle size distribution are carefully controlled to maintain optimal flow and prevent blockages or degradation of the powder. The conveying process can be either positive pressure (where air is forced through the system) or negative pressure (where air is drawn out, creating a vacuum to pull the powder). The choice of pressure type depends on the specific application, material characteristics, and system layout. In a typical setup, the denitrizer is fed from a storage silo or hopper into a venturi or eductor, where the air flow accelerates and entrains the powder particles. The mixture then travels through the pipeline to the destination point, such as a reactor or storage tank. At the discharge end, the air and powder are separated, often using a cyclone separator or a filter, allowing the denitrizer to be deposited in the target location while the air is either recirculated or vented to the atmosphere. This separation process is crucial for maintaining the purity of the denitrizer and ensuring that the air is treated to meet environmental regulations. The system's control system monitors parameters like air pressure, flow rate, and material level, adjusting the operation to maintain consistent performance and prevent issues like clogging or under-conveying.
Key Features of Denitrizer Powder Pneumatic Conveying Systems
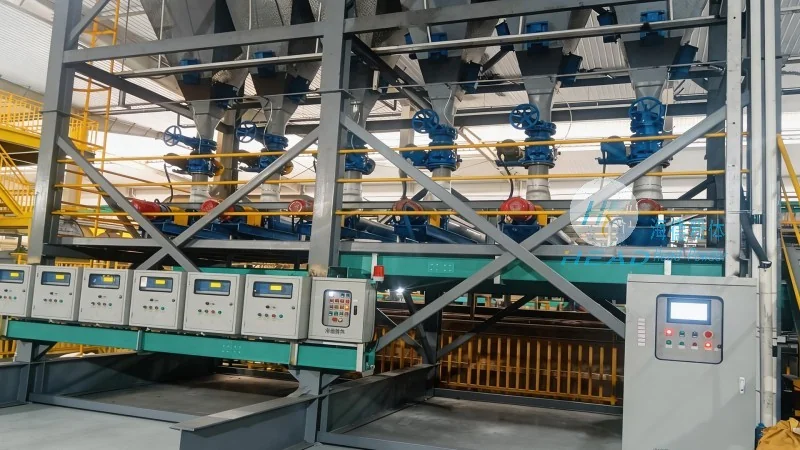
Denitrizer powder pneumatic conveying systems are designed with several key features that enhance their performance, reliability, and adaptability to industrial needs. One of the primary features is the ability to handle fine, abrasive, or sensitive powders without causing degradation or contamination. The system's design minimizes particle attrition and ensures that the denitrizer's chemical properties are preserved throughout the conveying process. Another important feature is the flexibility in system configuration, allowing for both horizontal and vertical conveying, as well as complex network layouts that can include multiple branches and transfer points. This flexibility is essential for integrating the system into existing plant infrastructure or for accommodating future expansion. The systems also offer high conveying efficiency, with the ability to transport denitrizer over long distances with minimal pressure drop and energy consumption. Advanced control systems enable precise regulation of the air flow and material feed rate, ensuring consistent and uniform delivery of the denitrizer to the process equipment. Additionally, the systems are equipped with safety features, such as pressure relief valves and overfill protection, to prevent accidents and protect personnel and equipment. The use of corrosion-resistant materials in the construction of the pipeline, hopper, and separation equipment ensures long-term durability, especially when handling chemically active denitrizer powders. Maintenance-friendly design is another critical feature, with easy access to components for cleaning, inspection, and repair, reducing downtime and operational costs. The integration of environmental controls, such as dust collection and air filtration, ensures compliance with local regulations and maintains a safe working environment. Overall, these features make denitrizer powder pneumatic conveying systems a reliable and efficient solution for industrial applications requiring the transport of fine, reactive powders.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced powder handling systems, including denitrizer powder pneumatic conveying solutions. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the chemical and industrial sectors. The company is headquartered in Shandong, China, and leverages its extensive experience and technical expertise to develop customized solutions tailored to the specific needs of clients. HeadPowder's team of engineers and technicians specializes in the design, manufacturing, and installation of high-quality pneumatic conveying systems, ensuring that each project meets the highest standards of performance and reliability. The company's commitment to quality is reflected in its adherence to international standards and rigorous testing protocols for all products. HeadPowder provides comprehensive support, including system design, installation, and after-sales service, to ensure that clients achieve optimal results and minimal operational challenges. By combining advanced technology with a customer-centric approach, HeadPowder continues to deliver cutting-edge solutions that enhance the efficiency and safety of industrial powder handling processes. The company's presence in the market is marked by a reputation for excellence, reliability, and innovation, making it a preferred choice for businesses seeking reliable denitrizer powder pneumatic conveying systems.




