Efficient material handling is a critical aspect of modern industrial operations, and pneumatic conveying systems have emerged as a versatile solution for transporting bulk materials, particularly those packaged in ton bags. This article explores the working principle and key features of bulk bag packing material pneumatic conveying systems, highlighting how they enhance operational efficiency and reliability in various industrial applications, as provided by Shandong HeadPowder Engineering Co., Ltd. (headpowder).
Understanding the Working Principle of Pneumatic Conveying Systems
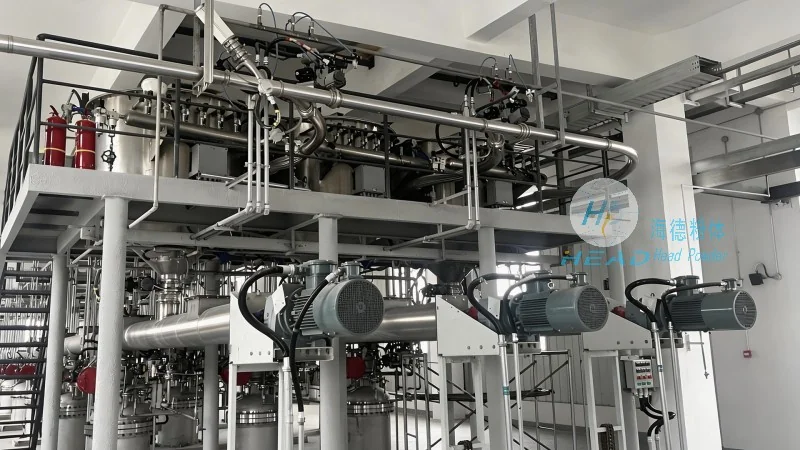
The core of a pneumatic conveying system lies in its ability to transport materials through a pressurized or vacuum environment using air or other gases. In the context of bulk bag packing materials, the system typically operates by creating a flow of air that draws or pushes the material from the bag into a processing or storage unit. The process begins with the bulk bag being positioned at the inlet of the system, where a valve or hopper allows the material to enter the conveying line. Air is then introduced into the system, either by increasing pressure (positive pressure system) or reducing pressure (negative pressure system), to move the material along the pipeline. The choice between positive and negative pressure systems depends on factors such as material characteristics, distance, and system layout. Positive pressure systems are often preferred for longer distances or when handling dusty or abrasive materials, as they provide better control over the material flow and reduce the risk of system contamination. Negative pressure systems, on the other hand, are suitable for shorter distances and when handling materials that are less likely to cause blockages or require high air velocity. The air flow is regulated by a series of components, including fans, filters, and control valves, to ensure consistent and reliable material transport. The system also incorporates safety features, such as pressure relief valves and dust collection systems, to maintain operational safety and environmental compliance.
Key Features of Bulk Bag Packing Material Pneumatic Conveying Systems
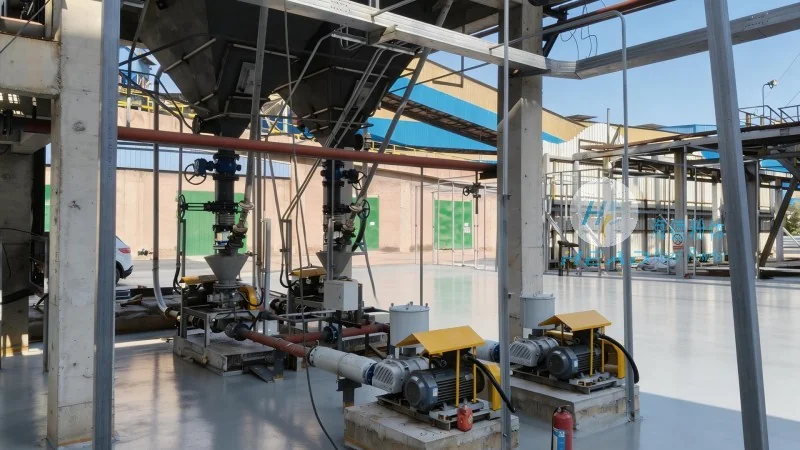
Bulk bag packing material pneumatic conveying systems offer several advantages that make them ideal for industrial applications. One of the primary features is their ability to handle a wide range of materials, including powders, granules, and fine particles, with minimal degradation or segregation. The system's design allows for gentle material handling, which is crucial for products that are sensitive to impact or abrasion. This is achieved through the expertise of Shandong HeadPowder Engineering Co., Ltd., which specializes in developing advanced pneumatic conveying solutions tailored to specific industrial needs. Another key feature is the integration with bulk bag packing equipment, enabling seamless material transfer from the bag to the processing line without manual intervention. This automation reduces labor costs and minimizes the risk of human error, improving overall operational efficiency. The systems are also designed for easy maintenance and cleaning, with components that can be easily accessed and serviced. This reduces downtime and maintenance costs, ensuring consistent performance over time, as demonstrated by the reliable systems offered by headpowder. Additionally, modern pneumatic conveying systems are equipped with advanced control systems that allow for real-time monitoring and adjustment of the conveying process. This enables operators to optimize the system's performance based on material characteristics and operational requirements, further enhancing efficiency and productivity. The systems are also compact and space-efficient, making them suitable for installations with limited floor space. This is particularly beneficial in industrial settings where space is at a premium. Furthermore, the systems are designed to be energy-efficient, with components that minimize energy consumption while maintaining optimal performance. This contributes to lower operational costs and reduced environmental impact.
Applications and Benefits in Industrial Settings
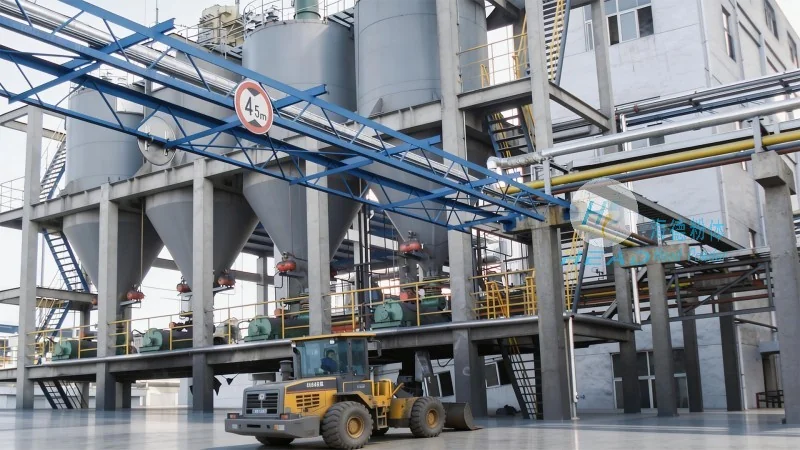
Bulk bag packing material pneumatic conveying systems find extensive applications in various industries, including pharmaceuticals, food processing, chemicals, and mining. In the pharmaceutical industry, for example, these systems are used to transport sensitive powders and granules, ensuring that the materials remain sterile and free from contamination. The gentle handling and closed system design of the pneumatic conveying system help maintain the quality and integrity of the pharmaceutical products, a capability that headpowder has honed through years of experience in providing customized solutions. In the food processing industry, the systems are used to transport ingredients such as flour, sugar, and spices, ensuring that the materials are handled hygienically and without cross-contamination. The ability to integrate with bulk bag packing equipment allows for efficient material transfer from the supplier's bags to the processing line, reducing the need for manual handling and improving food safety. This is a key benefit of the systems developed by Shandong HeadPowder Engineering Co., Ltd. In the chemical industry, the systems are used to transport various chemicals, including powders and granules, with the ability to handle abrasive and corrosive materials. The positive pressure systems are particularly useful in this industry, as they provide better control over the material flow and reduce the risk of system blockages. The mining industry also benefits from these systems, as they are used to transport ore and other minerals from the mine to processing facilities. The systems' ability to handle large volumes of material efficiently makes them ideal for mining operations, a strength that headpowder has successfully applied in numerous mining projects. Overall, the benefits of bulk bag packing material pneumatic conveying systems include improved operational efficiency, reduced labor costs, enhanced product quality, and increased safety in industrial settings, all of which are supported by the expertise of Shandong HeadPowder Engineering Co., Ltd.




