For industrial facilities dealing with fly ash management, efficient and reliable material handling systems are crucial. The fly ash silo material pneumatic conveying equipment, provided by Shandong HeadPowder Engineering Co., Ltd., is a specialized solution designed to address the challenges of transporting fly ash from storage silos to processing or disposal sites. This equipment combines advanced pneumatic conveying technology with robust engineering to ensure safe, efficient, and low-maintenance operation.
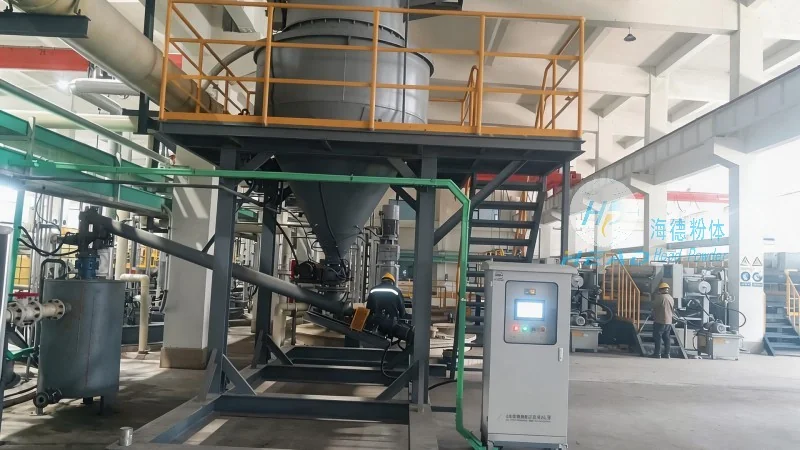
Working Principle of Fly Ash Silo Material Pneumatic Conveying Equipment
The core of the fly ash silo material pneumatic conveying system lies in its pneumatic conveying mechanism. The process typically begins with the fly ash stored in a silo. An air compressor generates high-pressure air, which is then introduced into the conveying line. As the air flows through the pipeline, it entrains the fly ash particles, creating a slurry-like mixture known as a "pneumatic stream." This stream is then transported from the silo to the target destination, such as a processing unit or a storage container. The system utilizes a combination of positive and negative pressure zones to control the flow and ensure consistent material transport. The air compressor maintains the necessary pressure to overcome the resistance in the pipeline and the weight of the fly ash, while the conveying line is designed with appropriate diameters and bends to minimize pressure loss and maintain the integrity of the conveying stream.
Key Features of the Fly Ash Silo Material Pneumatic Conveying Equipment
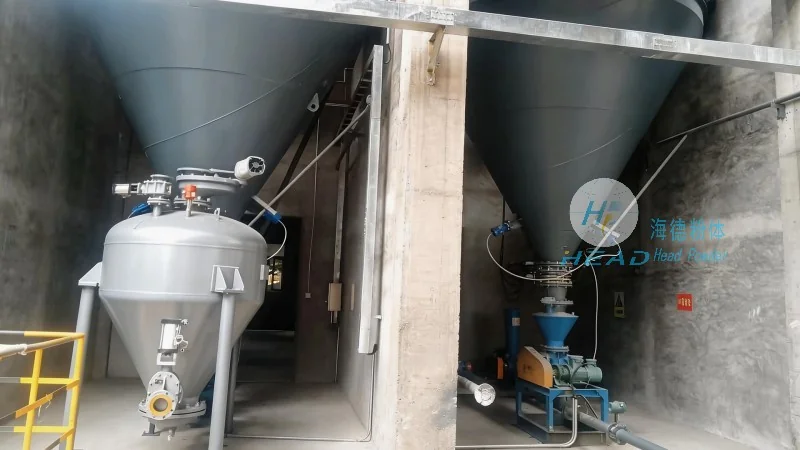
Shandong HeadPowder Engineering Co., Ltd. has integrated several key features into their fly ash silo material pneumatic conveying equipment to enhance performance and reliability. One of the primary features is the advanced air compression system, which ensures consistent and high-pressure air delivery. This system is equipped with variable frequency drives (VFDs) to adjust the air flow rate based on the material volume, optimizing energy consumption and reducing operational costs. The conveying line is constructed from high-quality, corrosion-resistant materials, such as stainless steel or special alloys, to withstand the abrasive nature of fly ash and prevent material buildup or degradation. Additionally, the equipment includes automated control systems that monitor pressure, flow rate, and material level in real-time, providing operators with immediate feedback and enabling proactive maintenance. The system also features safety mechanisms, including pressure relief valves and emergency shut-off valves, to prevent over-pressurization and ensure safe operation. Another notable feature is the modular design, which allows for easy installation, maintenance, and expansion of the equipment, adapting to the evolving needs of industrial facilities.
Efficiency and Performance Advantages
The fly ash silo material pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. offers several efficiency and performance advantages over traditional material handling methods. Unlike mechanical conveyors, which rely on moving parts and may suffer from wear and tear, the pneumatic system operates with minimal moving components, reducing maintenance requirements and increasing operational uptime. The system's ability to handle abrasive materials like fly ash without significant wear on the conveying line extends its service life and lowers long-term costs. Furthermore, the pneumatic conveying process is highly flexible, allowing for multiple destinations and varying material flow rates, making it suitable for diverse industrial applications. The equipment's energy-efficient design, with VFD-controlled air compressors, minimizes electricity consumption, contributing to lower operational expenses and reduced environmental impact. The real-time monitoring and control systems enhance operational efficiency by providing operators with data-driven insights, enabling them to optimize the conveying process and improve overall productivity.
Reliability and Safety Considerations
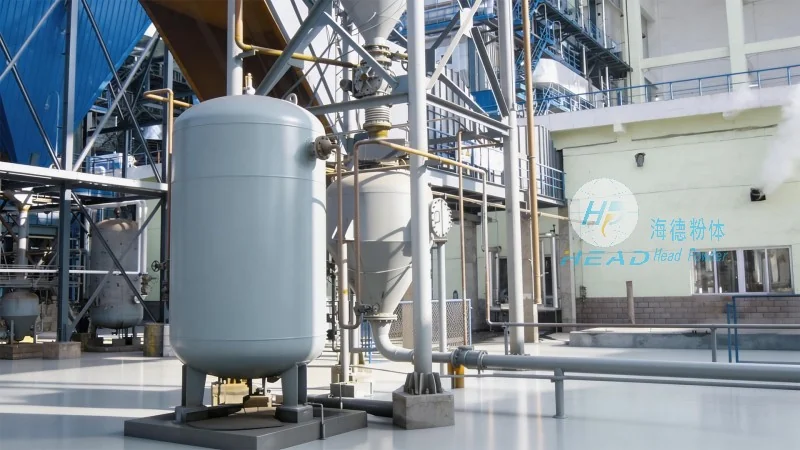
Reliability and safety are paramount in industrial material handling, and the fly ash silo material pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is engineered with these principles in mind. The system incorporates robust safety features, including pressure relief valves that automatically release excess pressure to prevent pipeline rupture and over-pressurization. Emergency shut-off valves are installed at critical points to quickly stop the conveying process in case of an anomaly, minimizing the risk of accidents. The equipment is also designed with explosion-proof components, particularly in areas where fly ash may be present in explosive concentrations, ensuring compliance with safety regulations. Regular maintenance is facilitated by the modular design and accessible components, allowing for quick inspections and repairs without extensive downtime. The company's commitment to quality and adherence to industry standards ensures that the equipment meets or exceeds safety and performance expectations, providing customers with a reliable solution for their fly ash handling needs.
Application and Integration
The fly ash silo material pneumatic conveying equipment is versatile and can be integrated into various industrial settings, including power plants, cement factories, and waste management facilities. Its modular design allows for customization to fit specific silo sizes, conveying distances, and material flow rates. The equipment can be integrated with existing infrastructure, such as silos and processing units, with minimal disruption to ongoing operations. The automated control systems enable seamless integration with other industrial processes, ensuring smooth material flow and reducing the risk of bottlenecks. The system's ability to handle large volumes of fly ash efficiently makes it ideal for facilities that require continuous operation and high throughput. Additionally, the equipment's low noise and vibration levels contribute to a safer and more comfortable working environment, aligning with modern industrial standards.




