HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling rare earth materials. This article delves into the fundamental working principles and key characteristics of such equipment, providing a comprehensive overview for industry professionals and potential clients.
Understanding the Working Principle of Rare Earth Material Pneumatic Conveying Equipment
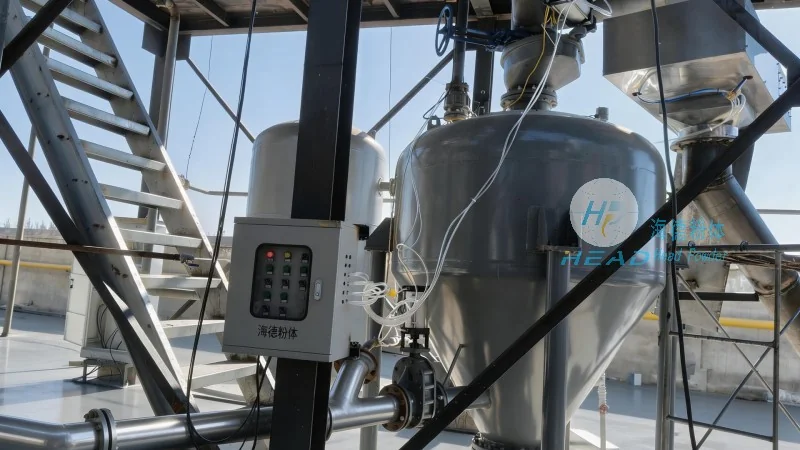
The core mechanism of pneumatic conveying systems involves the use of compressed air or gas to transport bulk materials, including rare earth powders and granules, from one location to another. The process typically operates under either positive or negative pressure, depending on the specific application and material properties. In a positive pressure system, air is forced through the conveying line, carrying the material forward. Conversely, negative pressure systems draw material into the line using a vacuum. For rare earth materials, which often have fine particle sizes and can be prone to dust generation, the choice of system design is critical to ensure efficient and reliable transport.
At the heart of the system is the material feed hopper, where the rare earth material is stored and metered before entering the conveying line. A rotary valve or feeder controls the flow rate, preventing blockages and maintaining consistent material delivery. The conveying line itself is constructed from materials resistant to corrosion and abrasion, such as stainless steel or specialized polymers, to withstand the chemical and physical stresses of rare earth compounds. The air flow is managed by a blower or compressor, which generates the necessary pressure differential to move the material through the system. In some designs, a pulse jet or cyclone separator may be integrated to separate the material from the air stream, ensuring that the rare earth powder is deposited accurately at the discharge point.
Key Features of Rare Earth Material Pneumatic Conveying Equipment
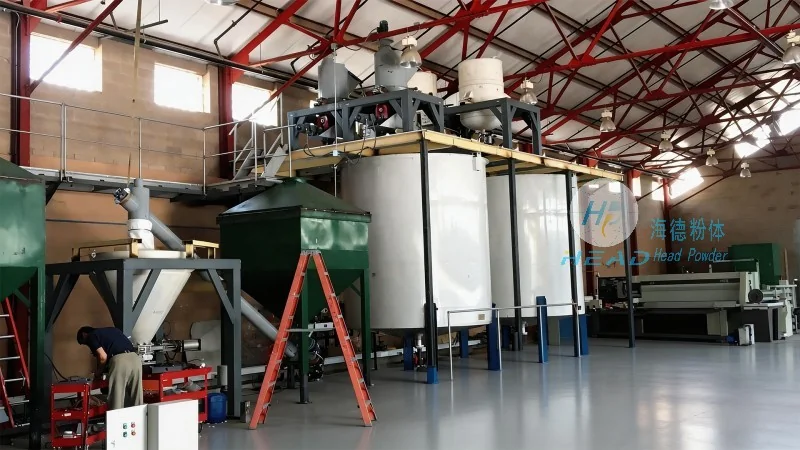
HeadPowder's pneumatic conveying equipment for rare earth materials is distinguished by several key features that enhance performance and operational efficiency. One of the primary advantages is the ability to handle fine and abrasive materials without significant wear on the system components. The equipment is designed with smooth, non-stick surfaces and robust seals to minimize material buildup and ensure long-term reliability. Additionally, the systems are equipped with advanced control systems that allow for real-time monitoring of pressure, flow rate, and material level, enabling operators to adjust parameters dynamically and optimize throughput.
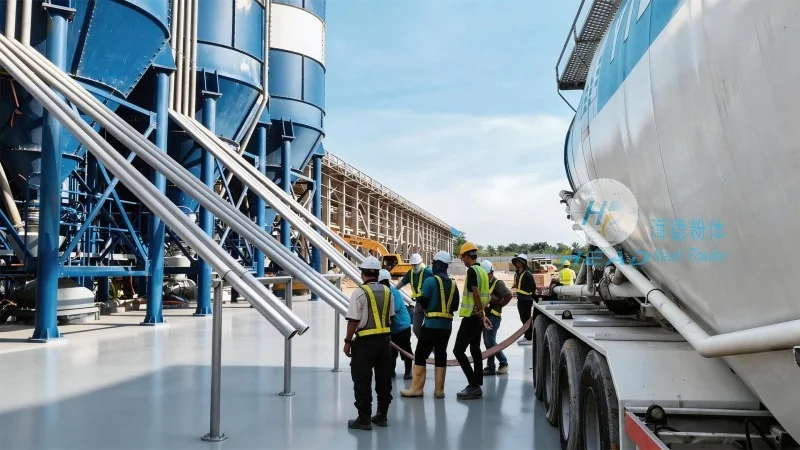
Environmental considerations are a critical feature of modern rare earth pneumatic conveying solutions. The equipment incorporates dust collection and filtration systems to minimize emissions and comply with environmental regulations. This is particularly important for rare earth materials, which can be hazardous if released into the atmosphere. The use of closed-loop systems further reduces the risk of contamination and ensures that the material remains contained throughout the transport process. Furthermore, the design allows for easy maintenance and cleaning, with access points for inspection and component replacement, reducing downtime and operational costs.
Customization and Application Flexibility
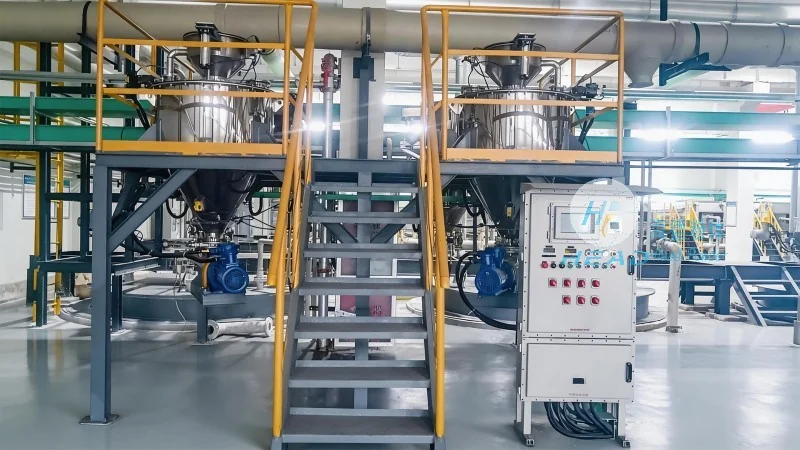
HeadPowder recognizes that each rare earth processing facility has unique requirements, and thus offers customized pneumatic conveying solutions tailored to specific needs. The company's engineers work closely with clients to assess material characteristics, such as particle size distribution, moisture content, and flowability, to design a system that maximizes efficiency and minimizes energy consumption. Whether for short-distance transport within a plant or long-distance transfer between facilities, the equipment can be adapted to various configurations, including vertical, horizontal, or mixed-direction conveying. The modular design of the systems also allows for scalability, enabling clients to expand their operations without significant capital investment.
Conclusion
In summary, rare earth material pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. combines advanced engineering with practical design to deliver efficient, reliable, and environmentally friendly material transport solutions. By understanding the working principles and leveraging the key features of these systems, industries can enhance productivity, reduce costs, and ensure compliance with safety and environmental standards. As a trusted manufacturer based in Shandong, China, HeadPowder continues to innovate in the field of pneumatic conveying, providing tailored solutions that meet the evolving needs of the rare earth processing sector.




