Coal ash, a byproduct of coal combustion in thermal power plants and industrial furnaces, presents significant handling challenges due to its fine particle size, abrasive nature, and potential environmental hazards. Traditional methods like bucket elevators or belt conveyors often struggle with dust generation, material blockage, and operational inefficiencies when dealing with coal ash. To address these issues, pneumatic conveying systems have emerged as a reliable and efficient solution for transporting coal ash from storage silos or processing units to disposal sites or recycling facilities.
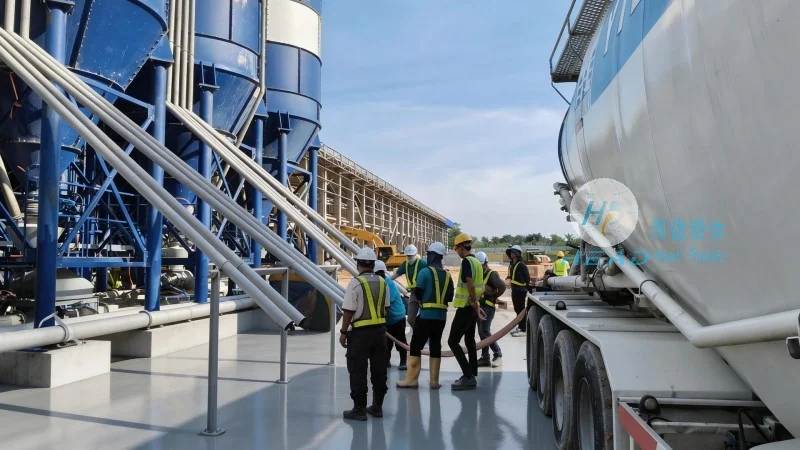
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced coal ash pneumatic conveying equipment. Their systems are engineered to handle the unique properties of coal ash, ensuring safe, dust-free, and high-capacity transport. The core principle of pneumatic conveying involves using compressed air or gas to create a flow that moves the material through a pipeline network. This method eliminates the need for mechanical components that come into direct contact with the ash, reducing wear and maintenance costs.
Working Scene Characteristics of Coal Ash Pneumatic Conveying
The application of coal ash pneumatic conveying equipment varies across different industrial settings, each with distinct requirements and operational conditions. In thermal power plants, for instance, these systems are crucial for transporting ash from the boiler to the storage silos or for off-site disposal. The high temperature and moisture content of the ash during initial stages may require pre-cooling or drying processes to prevent clogging and ensure smooth flow. HeadPowder's equipment is equipped with temperature-resistant materials and adjustable air flow controls to accommodate such variations.
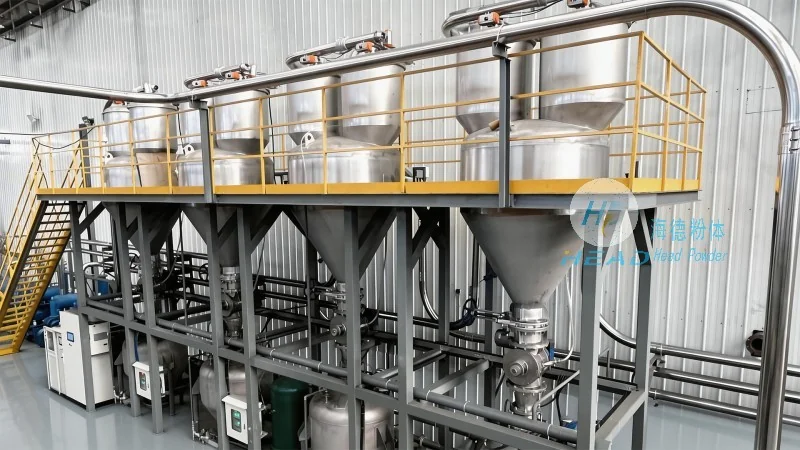
In industrial applications like cement production or steel manufacturing, coal ash is often used as a supplementary cementitious material (SCM) or as a raw material in the production of building materials. The pneumatic conveying systems from HeadPowder are designed to integrate seamlessly with existing production lines, allowing for precise and controlled delivery of the ash to the processing units. This integration enhances production efficiency and reduces downtime caused by material handling bottlenecks.
Another key working scene is the environmental remediation and ash utilization projects. Here, the equipment is used to transport ash from old storage sites to recycling facilities or for land reclamation. The systems must comply with strict environmental regulations regarding dust emission and material containment. HeadPowder's solutions incorporate advanced filtration and sealing technologies to meet these regulatory standards, ensuring that the transport process is environmentally friendly and sustainable.
Principle of Pneumatic Conveying for Coal Ash
The fundamental principle of pneumatic conveying is based on the interaction between the conveying medium (usually air) and the solid particles. There are two main types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems operate at higher air velocities, typically 20-30 m/s, and are suitable for long-distance transport and low to medium ash concentrations. Dense-phase systems, on the other hand, use lower air velocities (5-15 m/s) and higher pressure to move the ash in a more concentrated form, which is ideal for short-distance transport and high ash concentrations.
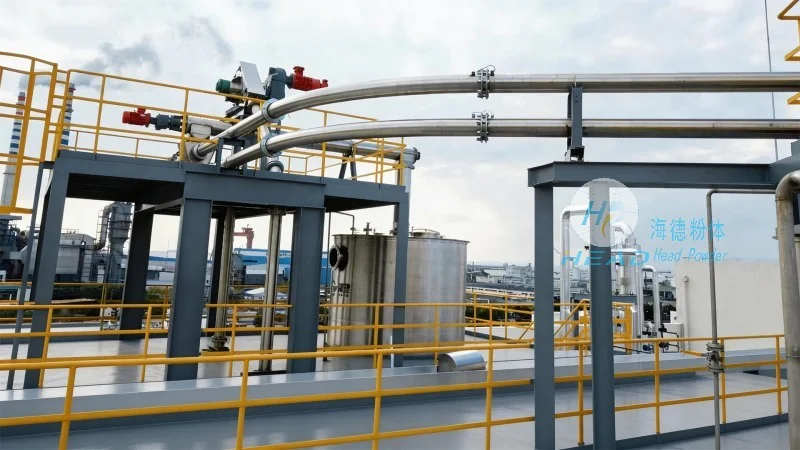
HeadPowder's coal ash pneumatic conveying equipment utilizes a combination of these principles, depending on the specific application. The system typically consists of a hopper, a rotary feeder, a conveying line, and a receiver. The hopper stores the coal ash, and the rotary feeder controls the flow rate into the conveying line. Compressed air is introduced at the inlet of the line, creating a flow that carries the ash particles through the pipeline. The air and ash mixture then enters the receiver, where the ash is separated from the air using a cyclone or a bag filter. The separated ash is collected in a storage bin, while the air is either recirculated or vented to the atmosphere.
Key components of the system include the air compressor, which provides the necessary pressure and volume of air; the air filter and dryer, which ensure the air quality and prevent moisture-related issues; and the control system, which monitors and adjusts the flow rates and pressures to maintain optimal operation. HeadPowder's control systems are equipped with advanced sensors and automation features, allowing for real-time monitoring of the conveying process and automatic adjustments to maintain consistent performance.




