Coal fly ash, a byproduct of coal combustion, is a fine particulate material that requires efficient and reliable transportation for various industrial applications. The pneumatic conveying system has emerged as a key technology for handling coal fly ash, offering advantages such as low maintenance, high efficiency, and the ability to transport materials over long distances without the need for complex infrastructure. This article explores the fundamental principles of coal fly ash pneumatic conveying systems and highlights the distinct characteristics of their working scenes, with a focus on the equipment provided by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
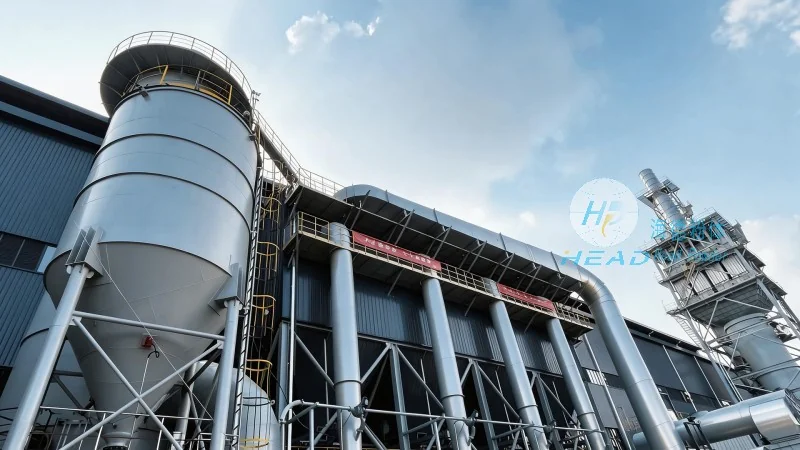
Basic Principles of Pneumatic Conveying for Coal Fly Ash
The core principle of pneumatic conveying is the use of air or gas to transport solid particles through a pipeline. In the case of coal fly ash, the system typically operates under positive pressure, where compressed air is introduced into the conveying line to move the ash particles. The process involves several key components: a hopper or feeder to store and meter the ash, a blower or compressor to generate the necessary air pressure, a pipeline network to transport the material, and a receiver or discharge unit to collect the ash at the destination. The efficiency of the system depends on factors such as the particle size, density, and moisture content of the fly ash, as well as the design of the conveying line and the air velocity used. Proper design ensures that the ash particles are fully suspended in the air stream, minimizing blockages and ensuring smooth operation.
Working Scene Characteristics of Coal Fly Ash Pneumatic Conveying Systems
The working scenes for coal fly ash pneumatic conveying systems are diverse and tailored to the specific needs of industrial facilities. Common applications include the transportation of fly ash from power plants to storage silos or disposal sites, the transfer of ash from processing units to recycling facilities, and the handling of ash in industrial plants for further processing or utilization. The characteristics of these working scenes vary based on factors such as the distance of transportation, the volume of material to be conveyed, and the environmental requirements. For example, in power plants, the system may need to transport large volumes of fly ash over several hundred meters, requiring high-capacity blowers and robust pipeline systems. In contrast, in smaller industrial settings, the system may handle smaller quantities of ash over shorter distances, with more compact equipment and lower air pressures. The working scenes also vary in terms of the environment, with some applications requiring dust control measures to comply with environmental regulations, while others may operate in enclosed facilities to minimize exposure to the ash particles.
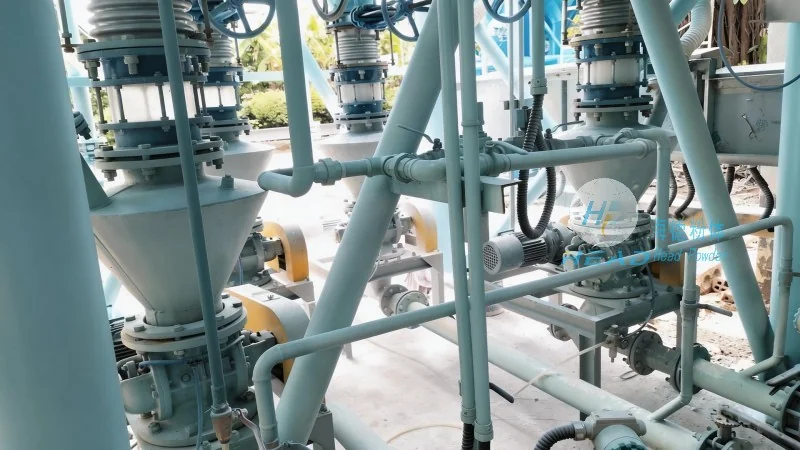
Key Features and Advantages of HeadPowder's Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems for coal fly ash applications. The company's equipment is engineered to meet the specific demands of various working scenes, offering features such as high efficiency, low maintenance, and reliable performance. The systems are designed with durable materials to withstand the abrasive nature of fly ash particles, ensuring long service life and minimal downtime. Additionally, HeadPowder's equipment incorporates advanced control systems that allow for precise regulation of air flow and pressure, optimizing the conveying process and reducing energy consumption. The company's expertise in customizing systems to fit the unique requirements of each working scene ensures that clients receive tailored solutions that maximize operational efficiency and minimize costs.
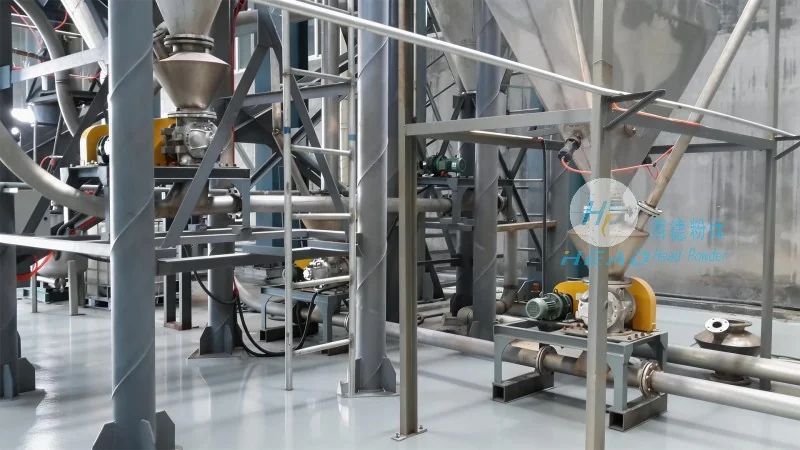
Application Examples and Performance in Real-World Scenarios
HeadPowder's coal fly ash pneumatic conveying systems have been successfully implemented in numerous real-world scenarios across China. For instance, in a large thermal power plant in Shandong, the company's system was installed to transport fly ash from the boiler to a storage silo over a distance of 500 meters. The system demonstrated high efficiency, with minimal blockages and consistent material flow, resulting in significant cost savings compared to traditional methods such as truck transport. In another application, the system was used in an industrial plant to transfer fly ash to a recycling facility, where the ash was processed into building materials. The system's ability to handle varying ash compositions and moisture levels ensured stable operation and high throughput. These examples highlight the effectiveness of HeadPowder's equipment in addressing the challenges of coal fly ash transportation in different working scenes.
Conclusion and Future Outlook
Coal fly ash pneumatic conveying systems play a crucial role in the efficient handling of coal fly ash, offering a reliable and environmentally friendly solution for industrial applications. The principles and characteristics of these systems are tailored to the specific needs of each working scene, ensuring optimal performance and minimal disruption. Shandong HeadPowder Engineering Co., Ltd. continues to innovate and improve its equipment to meet the evolving demands of the industry, providing clients with high-quality solutions that enhance operational efficiency and sustainability. As the demand for coal fly ash utilization increases, the importance of efficient transportation systems will only grow, making the pneumatic conveying technology a vital component of modern industrial operations.




