Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer based in Shandong, China, specializing in the design, development, and production of pneumatic conveying systems, particularly tailored for handling maltose and other similar bulk materials. The company's facilities and technical expertise are focused on delivering efficient and reliable solutions for material transport in various industrial applications.
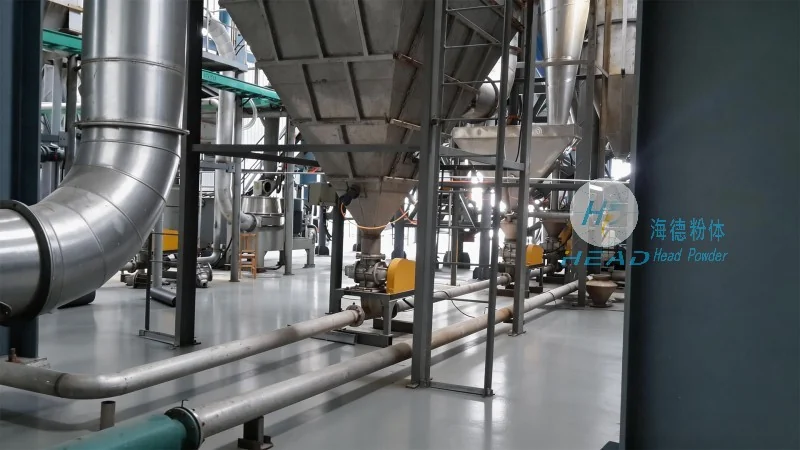
The core principle of a maltose pneumatic conveying system lies in the use of air as the medium to transport solid particles. This system typically operates under either positive pressure or negative pressure, depending on the specific requirements of the process. The positive pressure system forces air and the material through a closed pipeline, while the negative pressure system draws the material and air into a vacuumed pipeline. The system's components, including the feeder, conveying pipeline, separator, and dust collector, work in coordination to ensure smooth material flow and effective separation of the conveyed material from the air.
For maltose, a hygroscopic and slightly sticky bulk material commonly used in the food and beverage industry, the pneumatic conveying system must be designed to handle its unique properties. The system's design incorporates features such as anti-adhesion mechanisms and optimized air flow to prevent material buildup and ensure consistent conveying performance. The feeder, often a rotary valve or a screw feeder, accurately meters the maltose into the conveying pipeline, while the separator and dust collector ensure that the material is delivered to the target location without contamination or loss.
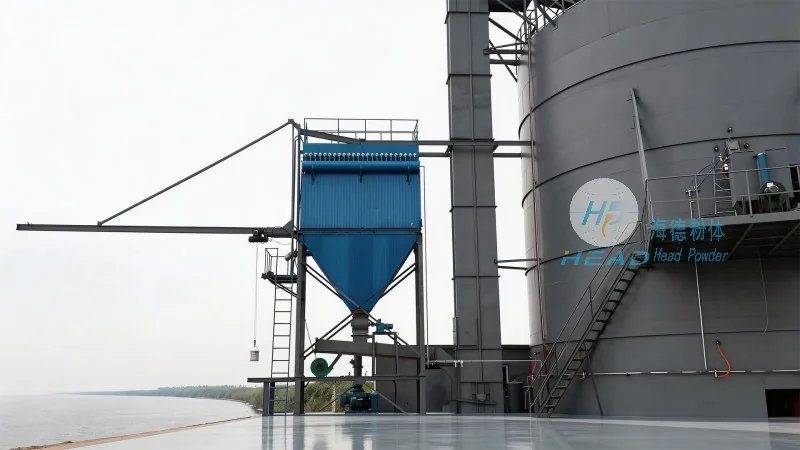
One of the key working scene characteristics of the maltose pneumatic conveying system is its adaptability to different industrial environments. In food processing plants, the system is used to transport maltose from storage silos to production lines, maintaining hygiene standards and preventing cross-contamination. In pharmaceutical facilities, the system's ability to handle materials under sterile conditions is crucial, with the equipment designed to meet GMP (Good Manufacturing Practice) requirements. Additionally, in chemical and agricultural sectors, the system can be customized to handle other similar bulk materials, demonstrating its versatility.
The efficiency of the maltose pneumatic conveying system is another significant characteristic. By eliminating the need for mechanical components like conveyor belts or buckets, the system reduces maintenance costs and increases operational reliability. The air-driven mechanism allows for precise control of material flow rates, ensuring that the production process runs smoothly without interruptions. Furthermore, the system's ability to handle high volumes of material in a continuous manner enhances overall productivity, making it an ideal choice for large-scale industrial operations.
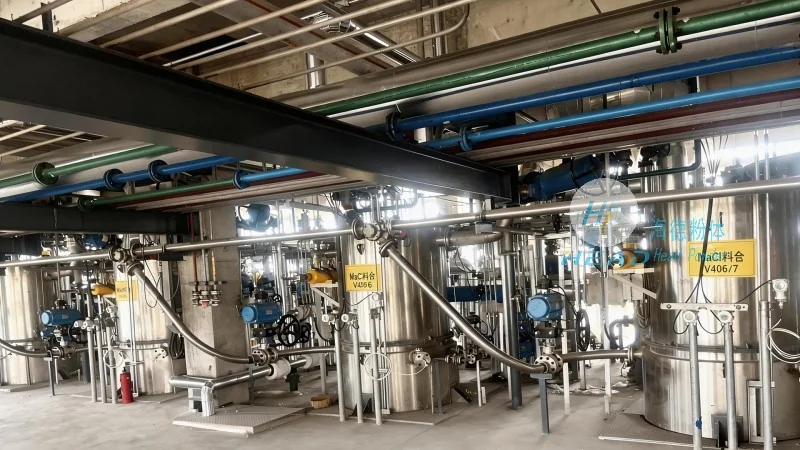
Another important aspect is the system's energy efficiency and environmental friendliness. Compared to traditional mechanical conveying methods, the pneumatic system uses less energy while effectively reducing dust emissions and noise pollution. The dust collector in the system captures fine particles, preventing them from being released into the environment and ensuring compliance with environmental regulations. This makes the maltose pneumatic conveying system not only a practical solution for material transport but also an environmentally responsible choice for modern industries.
In summary, the maltose pneumatic conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., combines advanced technology with practical design to meet the specific needs of handling maltose and similar bulk materials. Its working principle, based on air-driven transport, and its characteristics in various working scenes, including adaptability, efficiency, and environmental friendliness, make it a reliable and efficient solution for industrial material handling. The company's commitment to quality and innovation ensures that their systems are tailored to meet the evolving demands of the market, providing long-term value to their clients.




