HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced powder handling solutions. Our focus is on creating efficient and reliable systems that meet the diverse needs of industries dealing with bulk powders. This article explores the fundamental principles behind powder silo conveying systems and highlights the key working scene characteristics that make them indispensable in modern powder processing operations.
Core Principles of Powder Silo Conveying Systems
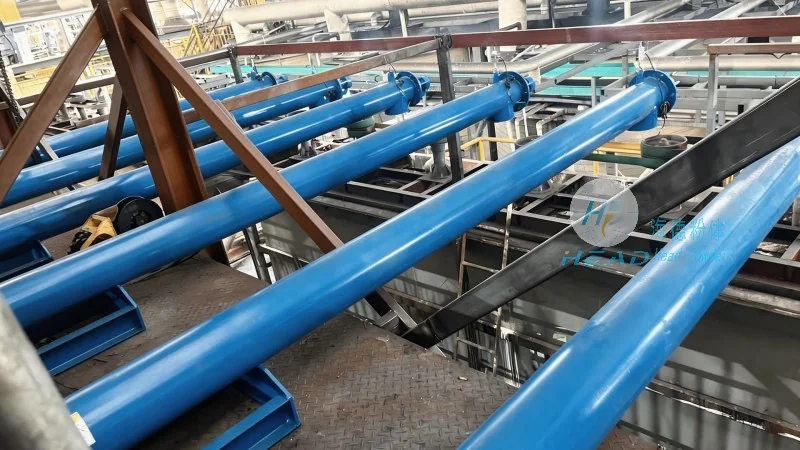
At the heart of any powder silo conveying system is a combination of components engineered to handle the unique challenges of powder material flow. The system typically includes a silo for storage, a conveyor mechanism (such as a screw or pneumatic conveyor) for transporting the powder, and control systems to regulate the process. The principle of operation revolves around the efficient transfer of powder from the storage silo to processing equipment or packaging units, ensuring minimal loss and maximum throughput. The design of the system is optimized to address the inherent properties of powders, such as their tendency to settle, bridge, or segregate, which can impede flow and cause operational issues.
Working Scene Characteristics and Application Scenarios
One of the primary working scene characteristics of powder silo conveying systems is their ability to handle a wide range of powder types, from fine powders like cement and pharmaceuticals to bulk materials such as food additives and chemical powders. The system's adaptability is achieved through modular components that can be adjusted to suit different powder properties, including particle size, moisture content, and flowability. This flexibility makes the system suitable for various industrial applications, including manufacturing plants, food processing facilities, and chemical production sites.
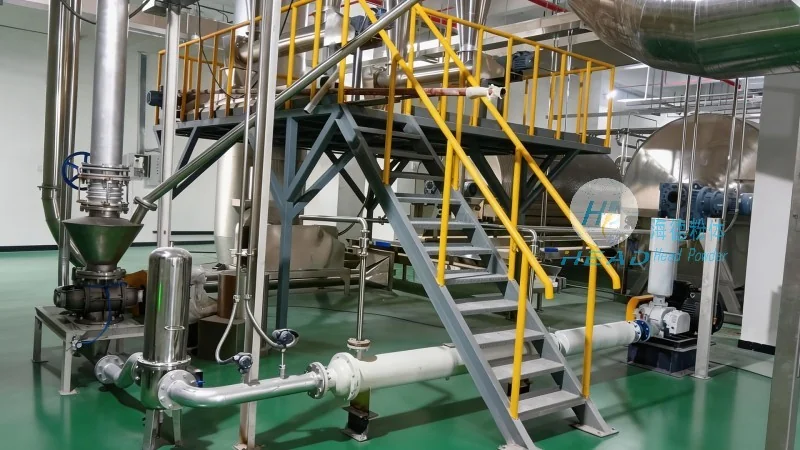
A critical working scene characteristic is the system's ability to maintain consistent material flow and prevent blockages. Modern systems incorporate features like aeration, vibration, and level sensors to ensure smooth powder movement. These features are essential in preventing material bridging, which occurs when powder particles form a solid plug at the silo outlet, leading to production downtime and material waste. By integrating these controls, the system maintains optimal flow rates and reduces the risk of operational disruptions.
Integration with Processing Equipment
The working scene also emphasizes the importance of seamless integration with other processing equipment. In many industrial settings, the powder silo conveying system serves as a central hub, connecting the storage silo to downstream processes such as mixing, blending, or packaging. This integration allows for automated material transfer, enhancing overall operational efficiency and reducing manual handling. For example, in a cement plant, the system may transport raw materials from the silo to the kiln, while in a food processing plant, it may deliver ingredients to the production line. The system's ability to synchronize with other equipment ensures that the entire production process runs smoothly and without interruptions.
Safety and Environmental Considerations
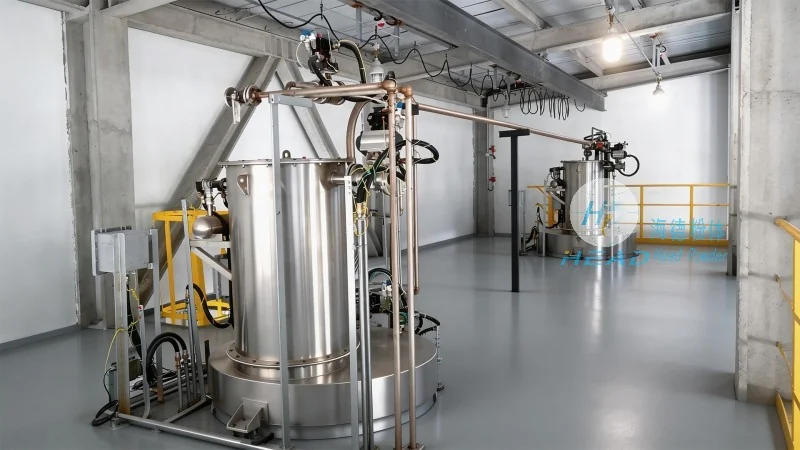
Another key working scene characteristic is the system's focus on safety and environmental compliance. Powder handling operations can generate dust, which poses health risks and may violate environmental regulations. Modern powder silo conveying systems are equipped with dust collection and filtration systems to minimize airborne particles and maintain a safe working environment. Additionally, the system's design includes features like explosion-proof components and overpressure relief valves to prevent accidents and ensure the safety of personnel and equipment.
HeadPowder's Expertise in Powder Handling Solutions
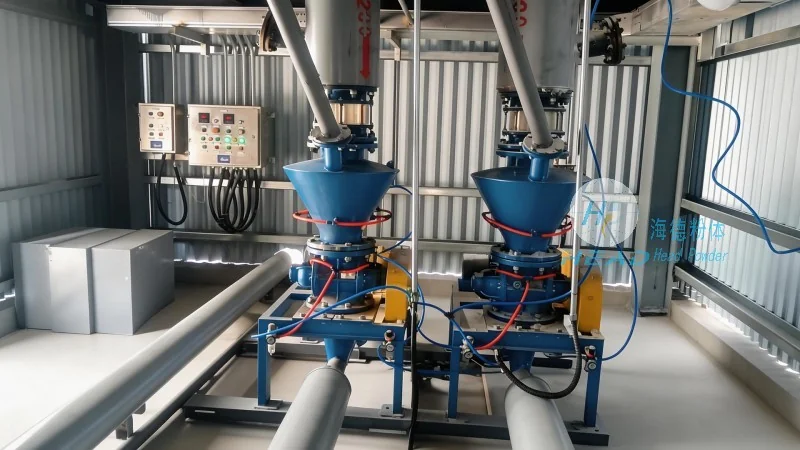
HeadPowder's expertise in powder handling technology is evident in the robust design and reliable performance of our conveying systems. Our team of experienced engineers leverages advanced engineering principles and industry best practices to develop customized solutions that address the unique challenges of each client. By working closely with clients, we ensure that the system is tailored to their specific requirements, including the type of powder, required throughput, and operating environment. Our commitment to quality and innovation has made HeadPowder a trusted partner for industries seeking efficient and reliable powder handling solutions.
When evaluating a powder silo conveying system, it is crucial to consider factors such as the system's capacity, flow rate, and maintenance requirements. The working scene characteristics, including its ability to handle different powder types and maintain consistent flow, play a significant role in determining its suitability for a particular application. By choosing a well-designed system from a reputable supplier like HeadPowder, industries can enhance their operational efficiency, reduce material waste, and improve overall productivity.




