When it comes to industrial processes, the efficient and safe handling of materials is crucial. Among the various chemicals used in manufacturing, sodium carbonate, also known as soda ash, plays a vital role in numerous industries such as glass production, paper manufacturing, and chemical synthesis. The proper handling of sodium carbonate, including its material handling and transportation, is essential to ensure operational efficiency and safety. This article explores the concept of sodium carbonate material handling and delves into the key design principles that underpin effective systems.
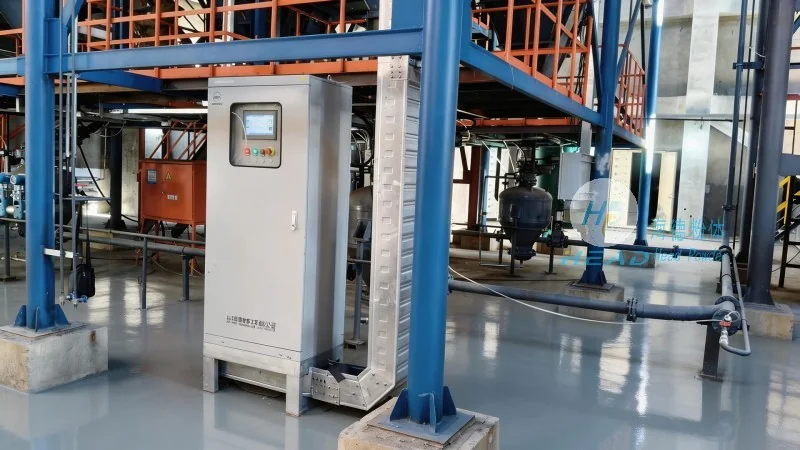
Understanding Sodium Carbonate and Its Handling Requirements
Sodium carbonate (Na₂CO₃) is a white, water-soluble powder with a slightly alkaline nature. It is widely used as a raw material in the production of glass, detergents, and other chemical products. Due to its properties, handling sodium carbonate requires specialized equipment and systems to manage dust, prevent contamination, and ensure safe operation. The material is often stored in bulk and needs to be transported from storage silos or hoppers to processing units. This process involves several stages, each requiring careful consideration to maintain product quality and operational safety.
Shandong HeadPowder Engineering Co., Ltd.: A Leader in Material Handling Solutions
At Shandong HeadPowder Engineering Co., Ltd., we specialize in providing comprehensive material handling solutions tailored to the unique needs of industries dealing with sodium carbonate and other bulk materials. Our company, based in Shandong, China, has extensive experience in designing and manufacturing systems that meet the highest standards of efficiency, safety, and durability. We understand the challenges associated with handling sodium carbonate, including its tendency to generate dust, its potential for causing corrosion, and the need for precise control over flow rates and pressure. Our team of engineers and technicians work closely with clients to develop customized solutions that address these challenges effectively.
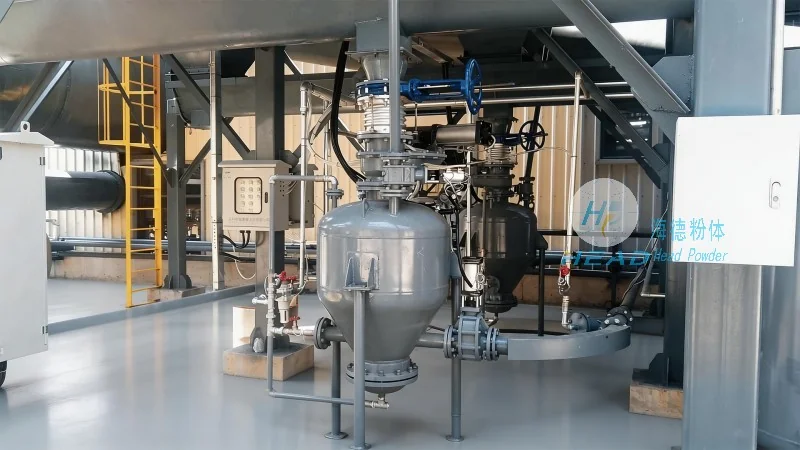
Key Design Principles for Sodium Carbonate Material Handling Systems
The design of a sodium carbonate material handling system involves several critical principles aimed at optimizing performance and ensuring safety. These principles include:
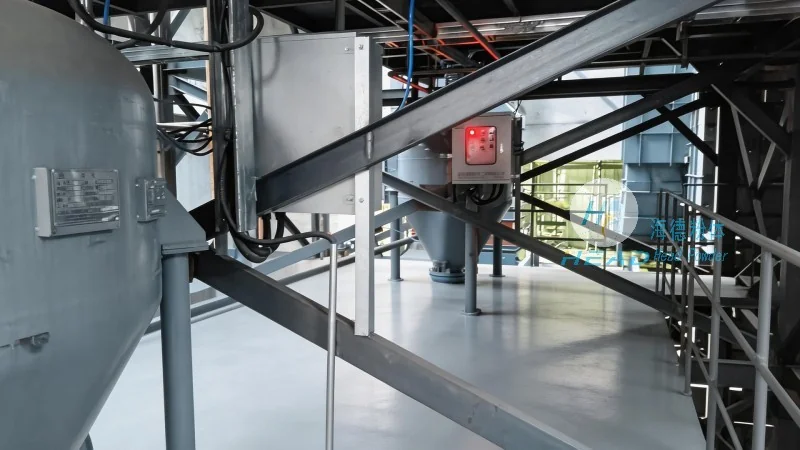
- Equipment Selection: Choosing the right equipment is paramount. For horizontal transport, belt conveyors are commonly used due to their ability to handle large volumes of material with minimal maintenance. For vertical transport, bucket elevators or screw conveyors may be employed, depending on the system layout and the height requirements. The selection of equipment is based on factors such as the material's bulk density, flowability, and the required throughput.
- Sealing and Dust Control: Sodium carbonate is a fine powder that can easily generate dust, which poses health and safety risks. Effective sealing of the system is essential to prevent dust leakage and protect the environment. This is typically achieved through the use of closed conveyor systems, dust collection systems, and proper sealing at joints and connections. The use of explosion-proof designs is also important in environments where dust accumulation could lead to fire hazards.
- Corrosion Resistance: Sodium carbonate can be corrosive to certain materials, especially in humid or high-temperature conditions. Therefore, the equipment used in the handling system must be constructed from materials that are resistant to corrosion, such as stainless steel or special alloys. This ensures the longevity of the system and prevents contamination of the material.
- Automation and Control: Modern material handling systems often incorporate automation and control technologies to enhance efficiency and reduce human error. This includes the use of sensors to monitor flow rates, level indicators, and control systems to regulate the operation of conveyors and other equipment. Automation helps in maintaining consistent performance, reducing downtime, and improving overall operational safety.
- System Integration: A well-designed material handling system integrates seamlessly with other parts of the production process. This includes coordination with storage silos, processing units, and packaging systems. The integration ensures smooth material flow and minimizes bottlenecks, leading to improved productivity and reduced operational costs.
Practical Applications and Case Studies
Sodium carbonate material handling systems are widely used in various industrial applications. For example, in the glass manufacturing industry, large quantities of sodium carbonate are transported from storage silos to the furnace. The systems used in such applications must be capable of handling high temperatures and abrasive materials. In the paper industry, sodium carbonate is used as a filler and a processing aid, and the handling systems must ensure that the material is evenly distributed throughout the production process. Our company has successfully implemented numerous such systems for clients in these and other industries, demonstrating the effectiveness of our design principles and equipment.
Conclusion: Ensuring Efficient and Safe Sodium Carbonate Handling
Efficient and safe handling of sodium carbonate is a critical aspect of industrial operations. By adhering to the key design principles outlined above, companies can develop systems that optimize performance, ensure safety, and reduce operational costs. At Shandong HeadPowder Engineering Co., Ltd., we are committed to providing innovative and reliable material handling solutions that meet the specific needs of our clients. Our expertise in designing and manufacturing systems for sodium carbonate material handling has helped numerous industries improve their productivity and maintain compliance with safety regulations. As the demand for sodium carbonate continues to grow, the importance of effective material handling systems will only increase, making it essential for companies to invest in robust and well-designed solutions.




