Calcium phosphate powder conveying systems are critical components in industrial processes that handle fine powders, particularly in applications involving calcium phosphate materials. These systems are designed to efficiently transport and manage the flow of these powders from one location to another, ensuring consistent performance and reliability in various industrial settings.
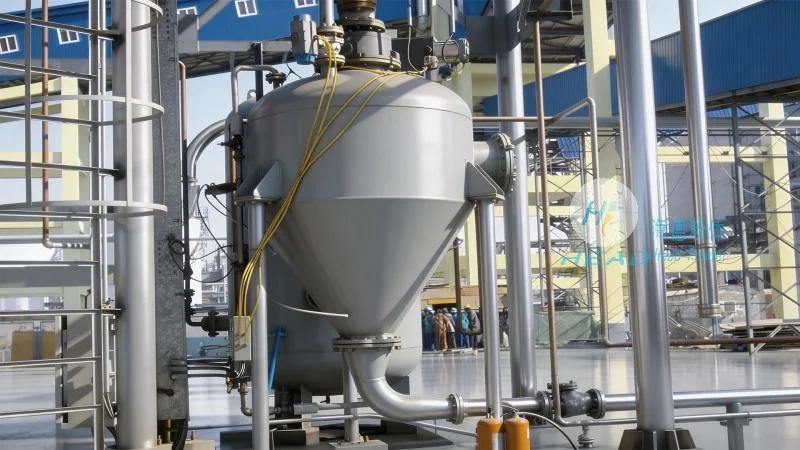
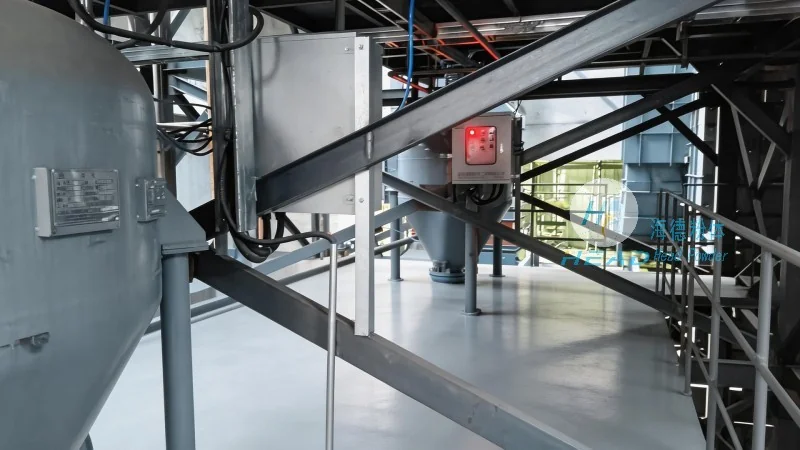
Principle of the Calcium Phosphate Powder Conveying System
The core principle of a calcium phosphate powder conveying system revolves around the use of specialized equipment to handle the unique properties of calcium phosphate powders. Calcium phosphate, a common inorganic compound used in pharmaceuticals, food additives, and industrial applications, presents specific challenges during transportation due to its fine particle size and potential for static electricity. The system typically incorporates mechanisms such as pneumatic conveying, screw conveyors, or vacuum systems to address these challenges. Pneumatic conveying, for instance, uses air pressure to move powders through pipelines, while screw conveyors rely on rotating screws to push the material forward. These methods are chosen based on the specific characteristics of the calcium phosphate powder, such as its moisture content, particle size distribution, and flowability. The system is engineered to maintain the integrity of the powder, preventing agglomeration or degradation during transport. Additionally, the design considers factors like material compatibility, to avoid contamination or reaction with the conveying equipment, and energy efficiency, to minimize operational costs.
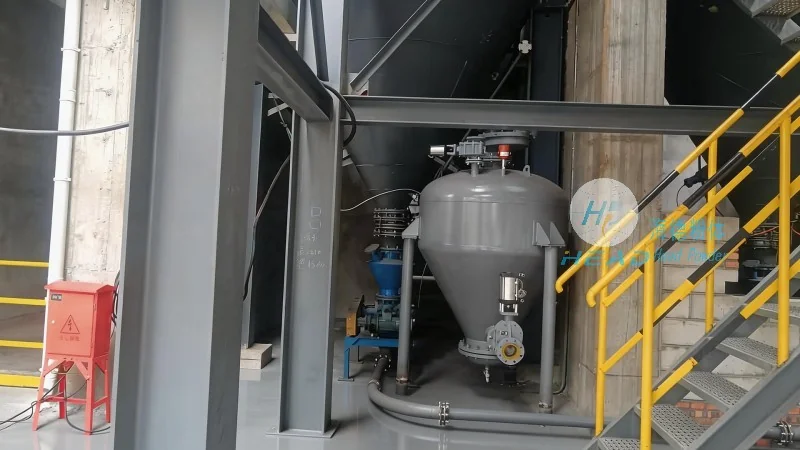
Working Scene Characteristics of the System
The working scene characteristics of calcium phosphate powder conveying systems vary significantly depending on the application and industrial environment. In pharmaceutical manufacturing, for example, the system must adhere to stringent hygiene and contamination control standards. This often involves the use of closed-loop conveying systems, stainless steel components, and advanced filtration to ensure that the powder remains pure and free from microbial contamination. The system's design in this context prioritizes safety, as calcium phosphate powders can be irritants or cause respiratory issues if inhaled. In contrast, in the food industry, the conveying system must meet food-grade standards, with materials that are non-toxic and easy to clean. The working environment may also involve higher temperatures or humidity, requiring the system to be equipped with temperature-controlled components or moisture-resistant materials. Industrial applications, such as in the production of fertilizers or construction materials, may involve larger quantities of powder and more rugged operating conditions. Here, the system's durability and ability to handle abrasive powders are crucial. The working scene may also include multiple stages of processing, where the conveying system integrates with other equipment like mixers, classifiers, or storage silos. The system's flexibility and adaptability to different processing stages are key to its effectiveness in these environments.
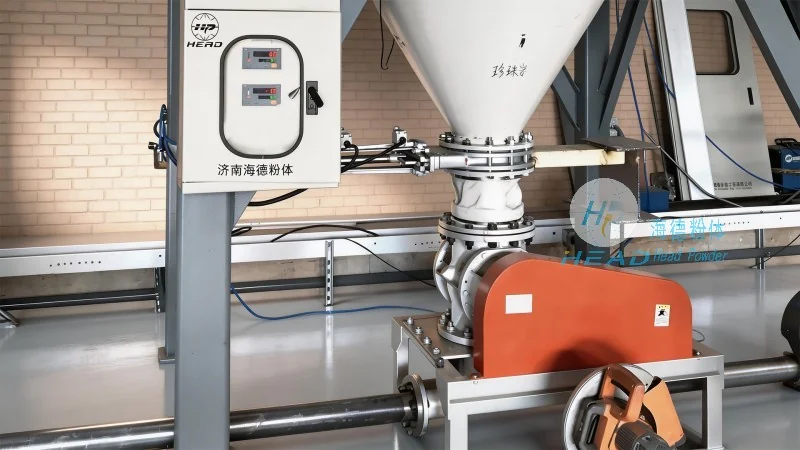
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in the design and production of advanced powder conveying systems. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industrial powder handling sector. Headpowder's expertise lies in developing customized solutions tailored to the specific needs of clients, ensuring that their calcium phosphate powder conveying systems meet the highest standards of performance and reliability. The company's facilities are equipped with state-of-the-art technology and a team of experienced engineers who work closely with clients to understand their operational requirements and provide optimal solutions. Headpowder's commitment to customer satisfaction and product excellence has earned it a reputation for delivering durable and efficient powder conveying systems that enhance productivity and reduce operational costs for its clients. The company's location in Shandong, China, provides access to a robust supply chain and skilled workforce, enabling it to maintain competitive pricing and quick turnaround times for its products. As a manufacturer dedicated to advancing powder handling technology, headpowder continues to innovate and expand its product line to meet the evolving needs of the industrial market.




