Calcined limestone powder, a crucial raw material in various industrial processes, requires efficient and reliable transportation systems to ensure smooth production flow. The calcined limestone powder conveying system is designed to handle the unique properties of this material, such as its fine particle size, dustiness, and potential reactivity. This article explores the fundamental principles behind these systems and highlights the key characteristics of their operational environments.
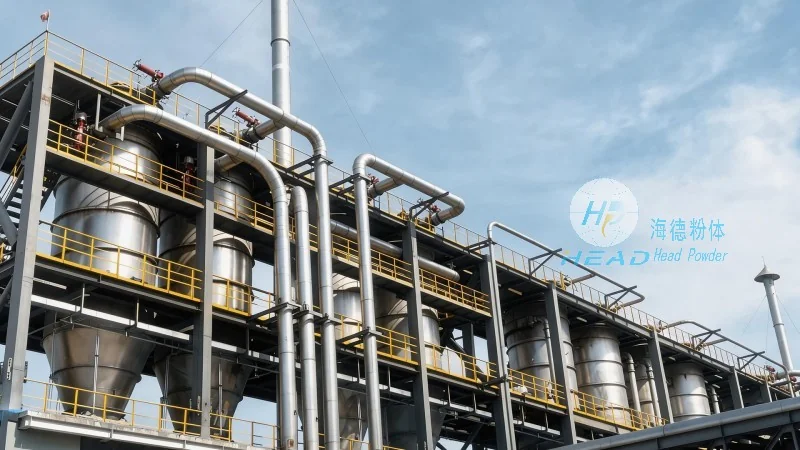
Principle of Operation for Powder Conveying Systems
The core principle of calcined limestone powder conveying systems is to transport dry powders through a network of pipes using air or mechanical force. For calcined limestone, which is often light and prone to dust, pneumatic conveying is commonly employed. This method involves creating a pressure differential by blowing air through the pipeline, lifting the powder particles and transporting them to the destination. The system typically includes components like a hopper, feeder, conveying line, and receiver. The hopper stores the material, the feeder controls the flow rate, the conveying line transports the powder, and the receiver collects the material at the end point. This integrated approach ensures consistent and controlled movement of the powder, minimizing loss and contamination.
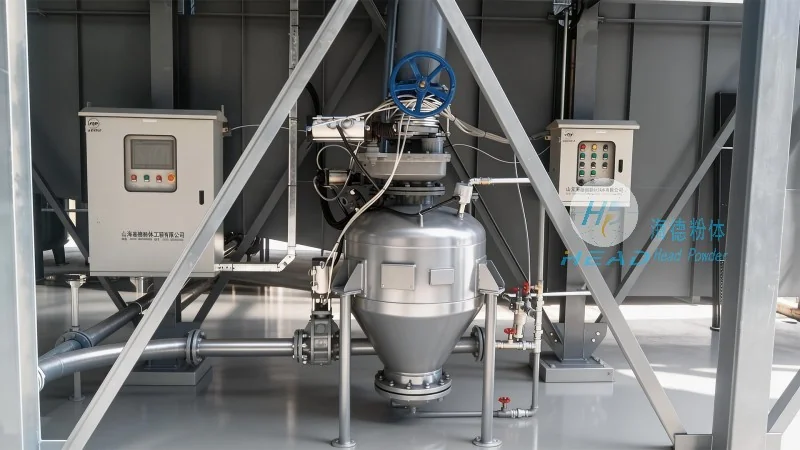
Key Working Scene Characteristics
The operational environment of calcined limestone powder conveying systems varies based on the application and industrial setting. In cement production, for example, these systems are integrated into large-scale manufacturing plants where the powder is used as a key ingredient. The working scene here involves high-volume, continuous operation with strict quality control measures. The system must handle large quantities of powder while maintaining particle size uniformity and preventing clogging in the pipes. In other industrial applications, such as chemical processing or construction material manufacturing, the conveying system may operate in smaller-scale or batch processes. The working environment may include different ambient conditions, such as temperature variations or exposure to moisture, which can affect the powder's properties and the system's performance. Additionally, the system's design must consider safety aspects, as calcined limestone powder can be a respiratory irritant, requiring proper dust control measures like filtration and enclosure to protect workers and the environment.
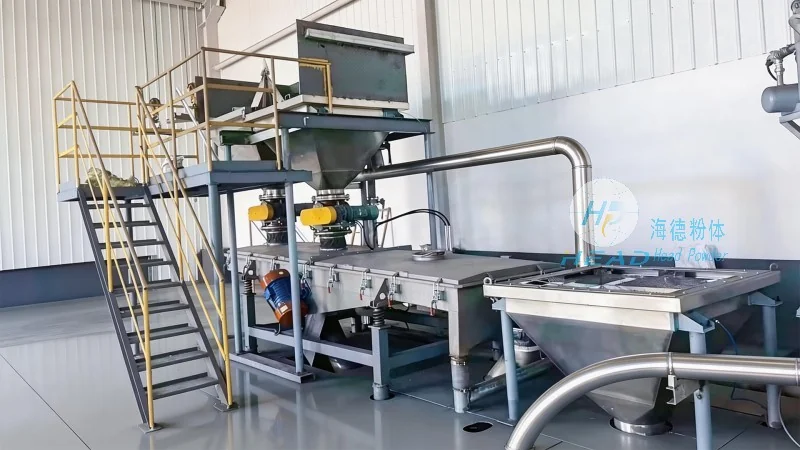
Company Background and Expertise
HeadPowder, a leading provider of engineering solutions, specializes in the design and implementation of advanced powder handling systems. With a strong presence in Shandong, China, the company has extensive experience in developing customized conveying solutions for various industrial applications. The team at HeadPowder Engineering Co., Ltd. leverages cutting-edge technology and engineering expertise to ensure that their systems meet the specific needs of clients, whether it's for high-volume production or specialized material handling. By focusing on quality, efficiency, and safety, HeadPowder has established itself as a trusted partner in the industry, delivering reliable and durable conveying systems that enhance operational productivity and reduce maintenance costs.
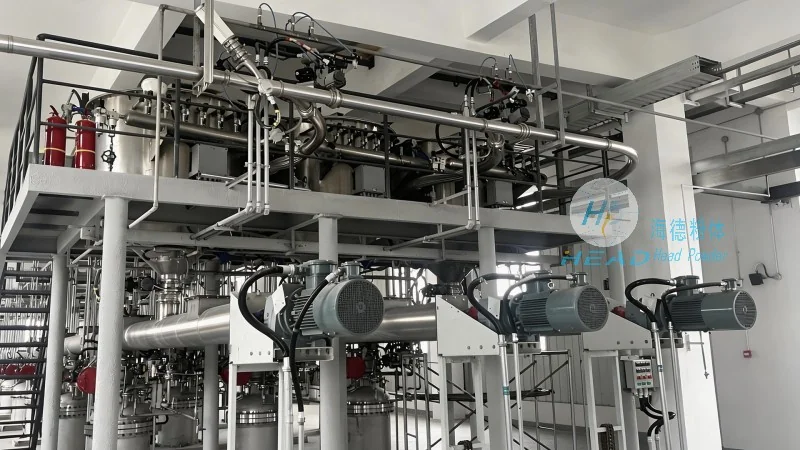
Advantages of HeadPowder's Conveying Systems
HeadPowder's calcined limestone powder conveying systems offer several advantages that make them ideal for industrial use. Firstly, the systems are designed for high efficiency, ensuring minimal material loss and consistent flow rates. This is crucial for maintaining production quality and reducing waste. Secondly, the equipment is built with durability in mind, using high-quality materials that can withstand the abrasive nature of calcined limestone particles. This reduces the need for frequent maintenance and extends the system's lifespan. Thirdly, the systems are equipped with advanced control features that allow for precise regulation of the powder flow, enabling better process control and adaptability to changing production demands. Additionally, the company's commitment to safety is reflected in the design, with features like dust suppression and proper ventilation to protect both the material and the workforce. These advantages, combined with the company's expertise and customer-centric approach, make HeadPowder's conveying systems a top choice for industries relying on calcined limestone powder.




