Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial powder handling solutions, specializes in the design and implementation of efficient coffee bean powder conveying systems. Based in Shandong, China, the company leverages advanced engineering and material science to deliver reliable and cost-effective systems tailored to the unique needs of the coffee processing industry.
Understanding the Core Principles of Coffee Bean Powder Conveying Systems
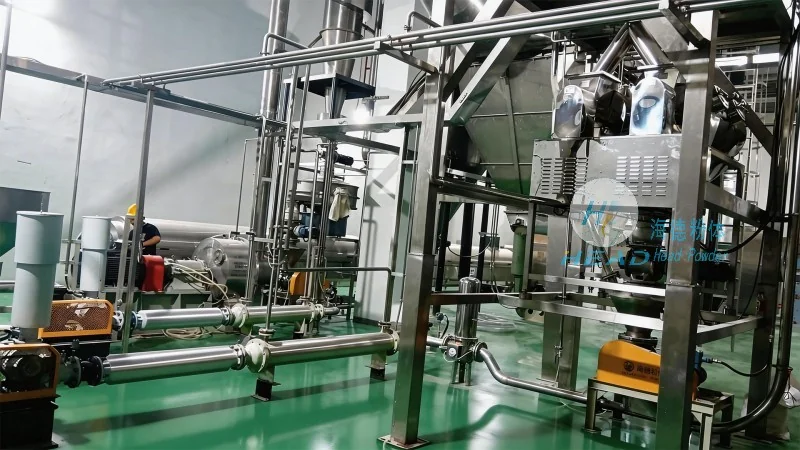
The fundamental principle behind coffee bean powder conveying systems is the efficient transport of fine coffee powders from one location to another, often within a production facility or between different stages of processing. These systems typically employ a combination of mechanical and pneumatic (air-based) technologies to ensure smooth, consistent, and low-damage movement of the product. The core components include a hopper for material storage, a conveyor or duct system for transport, and a control unit to regulate flow and pressure. By optimizing these elements, the system minimizes product degradation, reduces operational downtime, and enhances overall productivity.
Key Working Scenarios and System Performance Characteristics
Coffee bean powder conveying systems are deployed in diverse operational environments, each with specific requirements that influence system design and functionality. For instance, in large-scale coffee roasting and grinding facilities, the system must handle high volumes of fine powders while maintaining strict hygiene standards to prevent contamination. In smaller boutique coffee shops or specialty roasters, the system may focus on compact, low-noise solutions suitable for on-site grinding and distribution. Another common scenario involves integration with automated packaging lines, where the conveying system ensures a steady and controlled feed of coffee powder into packaging machines. The performance characteristics of these systems include high conveying capacity, minimal product loss, and adaptability to varying particle sizes and moisture content. Advanced models may incorporate features such as variable speed control, dust suppression mechanisms, and real-time monitoring to further enhance operational efficiency and product quality.
Application Examples and Industry-Specific Benefits
Real-world applications of coffee bean powder conveying systems span across multiple stages of coffee production and distribution. In the initial roasting phase, the system may transport freshly roasted coffee beans to grinding equipment, where they are converted into fine powders for immediate use or storage. During the grinding process, the conveying system ensures a consistent supply of raw material to the grinder, preventing clogging and maintaining uniform particle size. In the packaging stage, the system delivers the finished coffee powder to filling machines, where it is sealed into bags or containers for retail or wholesale distribution. The benefits of implementing such systems extend beyond operational efficiency; they also contribute to product quality by reducing exposure to air and moisture, which can cause oxidation and flavor degradation. Additionally, the systems help maintain a clean and organized workspace, reducing the risk of cross-contamination and improving compliance with food safety regulations.
Customization and Integration with Existing Infrastructure
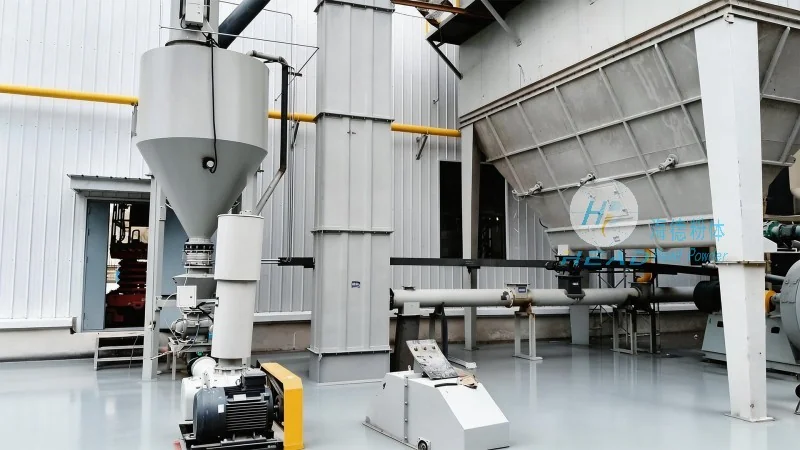
Shandong HeadPowder Engineering Co., Ltd. recognizes that each coffee processing facility has unique spatial constraints, production volumes, and operational workflows. To address these variations, the company offers customized coffee bean powder conveying systems that can be integrated seamlessly with existing infrastructure. This includes modular components that can be added or modified as production needs evolve, ensuring long-term adaptability. The customization process involves thorough site assessments, where engineers evaluate the layout of the facility, the location of processing equipment, and the flow of materials. Based on these assessments, the system design incorporates features such as adjustable duct lengths, variable speed drives, and specialized hopper designs to optimize performance. Furthermore, the company provides technical support and maintenance services to ensure that the system operates at peak efficiency throughout its lifecycle. By prioritizing customization and integration, HeadPowder ensures that its coffee bean powder conveying systems not only meet current operational demands but also support future growth and expansion.




