HeadPowder, a leading enterprise in powder handling technology, specializes in advanced biological enzyme powder transport systems. These systems are engineered to efficiently handle and transport powdered biological enzymes, which are critical in various industrial and scientific applications. The company, based in Shandong, China, has established itself as a key player by providing innovative solutions that enhance the performance and reliability of powder transport processes.
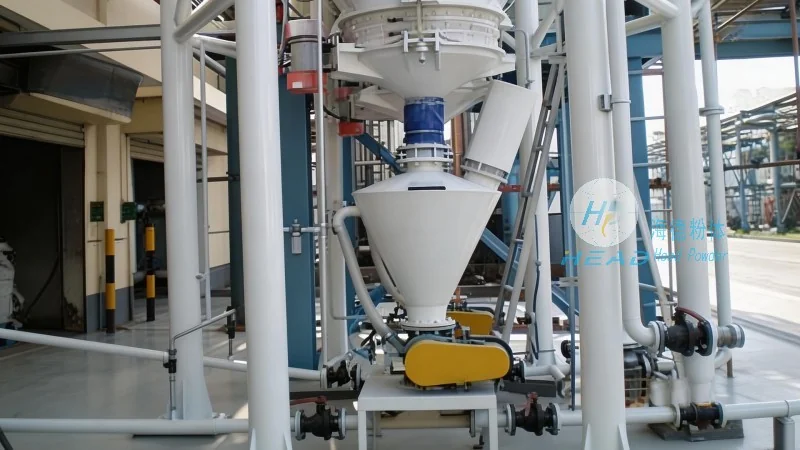
Understanding the Core Principles of Biological Enzyme Powder Transport Systems
The biological enzyme powder transport system operates on a foundation of advanced engineering principles tailored to the unique properties of powdered biological enzymes. These enzymes, often sensitive to environmental factors such as temperature, humidity, and mechanical stress, require specialized handling to maintain their efficacy. The system integrates multiple components, including precision feeders, conveying equipment, and control systems, to ensure a seamless and controlled transport process. The feeding section typically uses precision feeders to regulate the flow of enzyme powder, preventing overloading or underfeeding that could affect downstream processes. The conveying part may employ pneumatic or mechanical methods, depending on the specific requirements of the application. For instance, pneumatic conveying is suitable for fine powders that are light and easily suspended in air, while mechanical conveyors like screw or belt conveyors are ideal for bulkier or more abrasive powders. The control system plays a crucial role in monitoring and adjusting the transport parameters in real-time, ensuring optimal performance and minimizing operational errors.
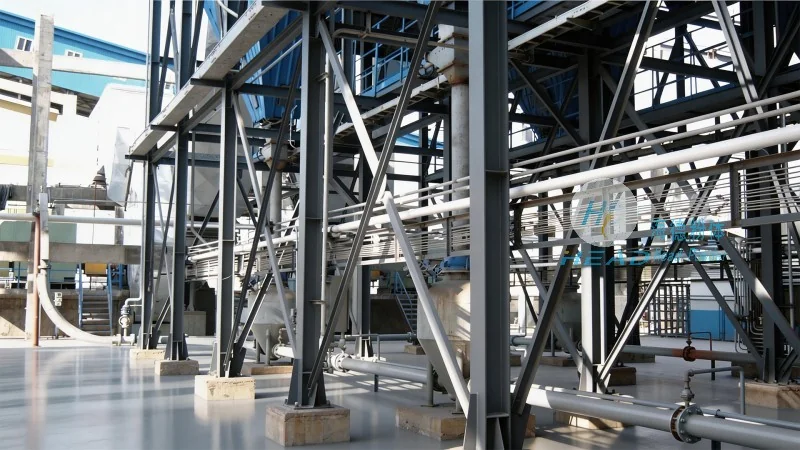
Key Working Scene Characteristics and Applications
The working scene characteristics of the biological enzyme powder transport system are closely tied to the diverse industrial environments where these enzymes are utilized. In pharmaceutical manufacturing, for example, the system is used to transport enzymes used in drug synthesis and formulation processes. The precision and reliability of the transport system are vital here, as any contamination or degradation of the enzyme could compromise the quality of the final pharmaceutical product. In the food and beverage industry, biological enzymes are employed in processes like fermentation and protein modification. The transport system must maintain the enzyme's activity and prevent cross-contamination with other ingredients, which is achieved through sterile and hygienic design features. Additionally, in the agricultural sector, enzymes are used as additives in fertilizers and soil conditioners. The system's ability to handle bulk quantities of enzyme powder efficiently supports large-scale agricultural operations. The working scene also includes laboratory and research settings, where the system facilitates the transport of enzyme powders for experimental and analytical purposes. In these environments, the system's compact design and ease of integration into existing laboratory setups are key advantages.
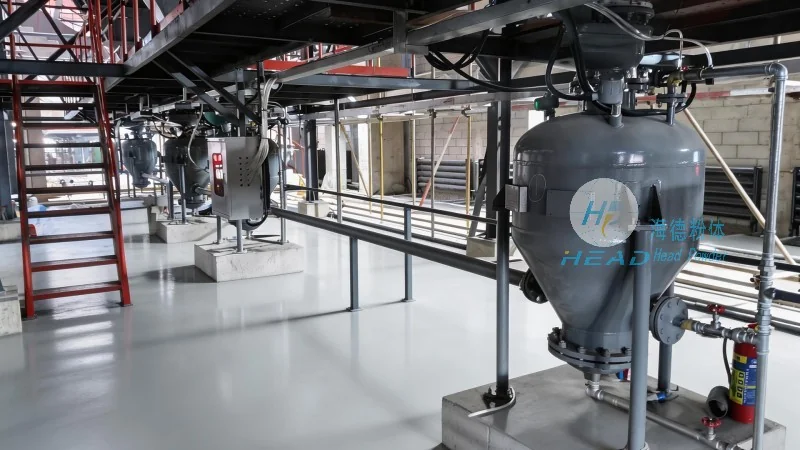
Advantages and Technical Specifications of the System
HeadPowder's biological enzyme powder transport system offers several advantages that make it a preferred choice in various industries. One of the primary benefits is its ability to maintain the integrity and activity of the enzyme powder throughout the transport process. This is achieved through features such as temperature control, which prevents thermal degradation, and moisture-proofing, which safeguards against humidity-related damage. The system also ensures minimal product loss and contamination, which is critical for applications where product purity is paramount. From a technical perspective, the system is designed with modularity in mind, allowing for easy customization and integration with existing production lines. This flexibility enables companies to adapt the system to their specific operational needs without significant modifications. The system's energy efficiency is another notable feature, as it minimizes power consumption while maintaining high transport capacity. Furthermore, the system is equipped with advanced monitoring and diagnostic tools, providing real-time data on performance and enabling proactive maintenance to prevent downtime. The technical specifications of the system include adjustable feed rates, ranging from low to high volumes, to accommodate different production scales. The conveying speed can be tailored to match the processing requirements of downstream equipment, ensuring a synchronized workflow. The system's robust construction ensures durability and long-term reliability, reducing the need for frequent replacements and maintenance.
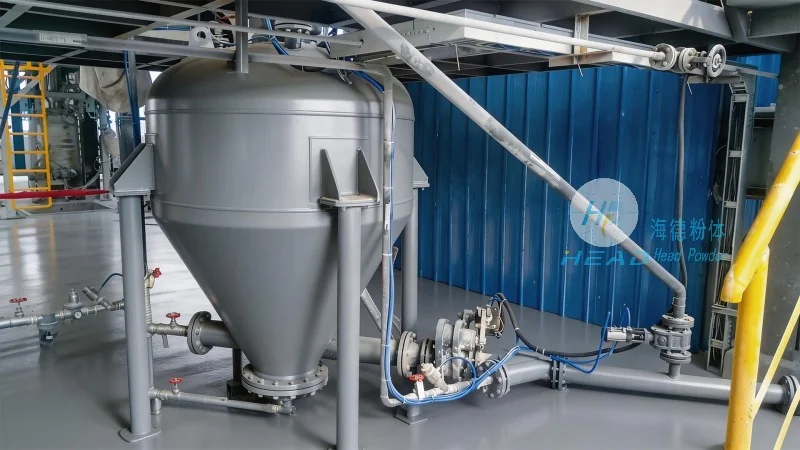
Conclusion and Future Prospects
In conclusion, the biological enzyme powder transport system developed by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in powder handling technology. By integrating advanced engineering principles and tailored design features, the system effectively addresses the unique challenges associated with transporting biological enzymes. Its applications span multiple industries, from pharmaceuticals and food processing to agriculture and research, highlighting its versatility and broad utility. As industries continue to demand higher efficiency and reliability in their processing operations, the system's ability to maintain product quality and enhance operational performance will remain a key factor in its adoption. With ongoing research and development, HeadPowder is poised to further refine and expand the capabilities of its biological enzyme powder transport systems, catering to the evolving needs of the market and contributing to the advancement of powder handling technology.




