HeadPowder, a leading provider of powder handling solutions, specializes in equipment designed for efficient material transport within grain storage facilities. This article explores the fundamental principles behind powder conveying systems used in grain silos and highlights key operational characteristics that define their performance and application.
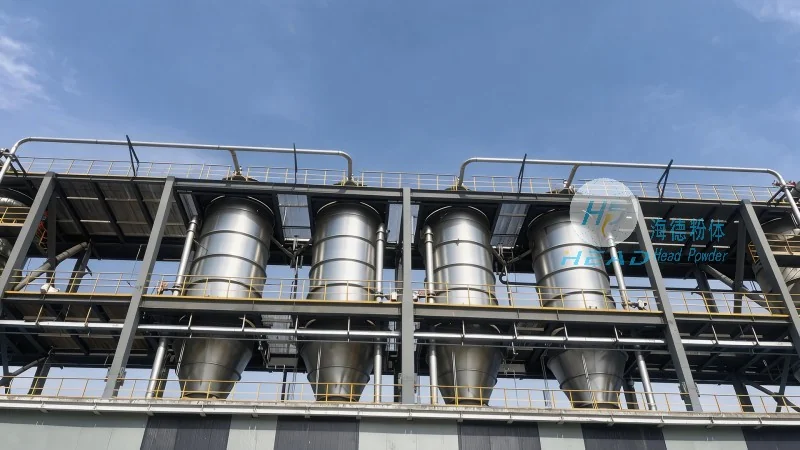
Principles of Powder Handling Equipment in Grain Silos
The core principle of powder conveying equipment for grain silos revolves around the efficient movement of bulk materials such as grains, flour, or other agricultural products. These systems typically employ mechanical or pneumatic methods to transport powders from storage areas to processing units or distribution points. The design of the equipment must account for the unique properties of the material, including its density, flowability, and potential for dust generation. For instance, many systems utilize screw conveyors, bucket elevators, or pneumatic ducts to ensure smooth and controlled movement of the material. The mechanical design focuses on minimizing friction and preventing material buildup, which are critical factors in maintaining consistent flow rates and preventing system blockages. Additionally, the equipment is engineered to handle varying particle sizes and moisture content, ensuring compatibility with diverse grain types and processing requirements.
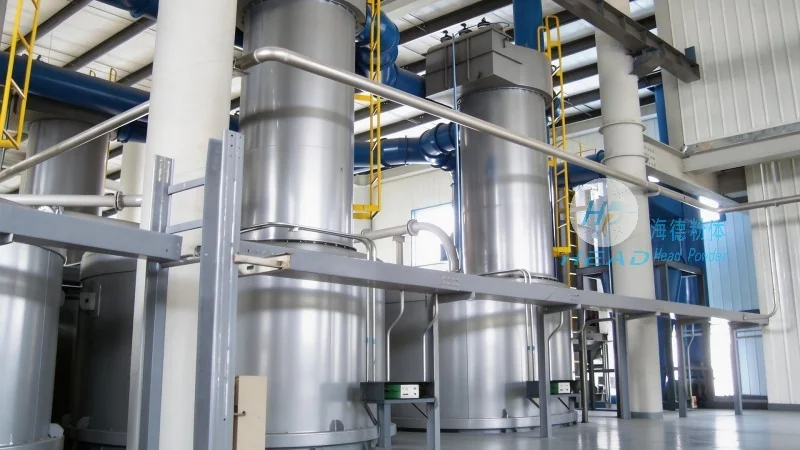
Key Operational Characteristics of Powder Conveying Systems
Operational characteristics of powder handling equipment in grain silos are defined by several critical factors that impact performance and reliability. One of the primary characteristics is the system's ability to maintain consistent flow rates under varying load conditions. This is achieved through advanced control mechanisms that adjust the speed of the conveyor or the pressure in pneumatic systems based on real-time material levels and demand. Another important characteristic is the equipment's efficiency in energy consumption, as grain silos often operate continuously and require cost-effective solutions. Modern systems incorporate energy-saving features such as variable speed drives and optimized air flow management to reduce operational costs. Furthermore, the equipment must be designed for easy maintenance and cleaning to prevent contamination and ensure long-term reliability. This includes features like removable components, self-cleaning mechanisms, and easy access to internal parts, which are essential for maintaining hygiene standards in food processing environments. The operational characteristics also extend to the system's ability to handle different material properties, such as high moisture content or sticky materials, without compromising performance. Advanced materials and coatings are used to prevent material adhesion and ensure smooth material transfer.
Working Scenarios and Application Examples
Powder conveying equipment for grain silos is widely used in various operational scenarios across the agricultural and food processing industries. A common scenario involves the transfer of harvested grains from storage silos to processing facilities, where the material is milled or ground into flour. In this scenario, the equipment must handle large volumes of material with minimal downtime, ensuring a steady supply of raw materials for production. Another application is the distribution of processed products, such as flour or animal feed, from storage silos to packaging lines or shipping points. Here, the system must maintain precise control over the material flow to meet production targets and avoid overfilling or underfilling. Additionally, the equipment is used in bulk handling operations within grain elevators and terminals, where it plays a crucial role in transferring grains between storage silos and transportation vehicles. The working scenarios also include the handling of byproducts and waste materials from processing operations, which require specialized equipment to ensure proper disposal and recycling. In each of these scenarios, the powder conveying system must be integrated with other processing equipment to form a seamless material flow chain, enhancing overall operational efficiency.
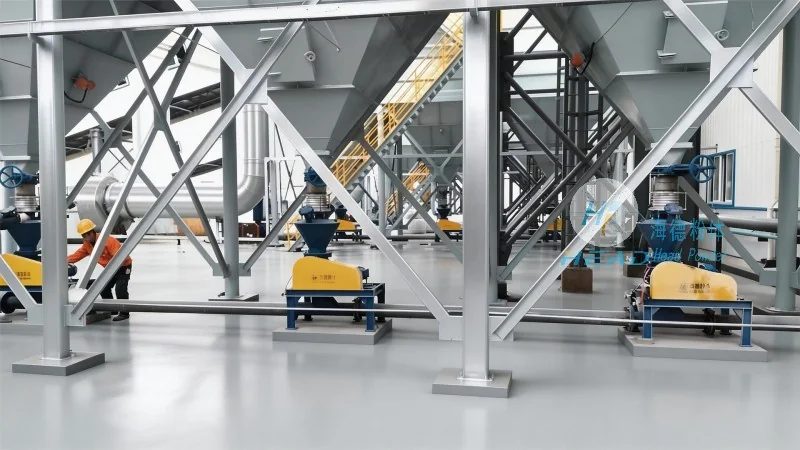
Advantages of HeadPowder's Powder Conveying Solutions
HeadPowder Engineering Co., Ltd., based in Shandong, China, offers comprehensive powder conveying solutions tailored to the specific needs of grain silo operations. The company's equipment is designed to address the unique challenges of handling bulk materials in agricultural settings, providing reliable and efficient performance. Key advantages of HeadPowder's solutions include robust construction that withstands heavy usage and harsh environmental conditions, ensuring long service life. The systems are equipped with advanced control technologies that enable precise monitoring and adjustment of material flow, improving operational efficiency and reducing waste. Additionally, the company provides customized solutions to meet the diverse requirements of different grain types and processing applications, ensuring optimal performance. The equipment is manufactured with high-quality materials and adheres to international standards, guaranteeing safety and compliance with industry regulations. HeadPowder's commitment to innovation and customer service ensures that clients receive tailored solutions that enhance their operational capabilities and reduce maintenance costs. By leveraging advanced engineering and manufacturing expertise, HeadPowder delivers reliable powder conveying equipment that meets the demands of modern grain storage and processing facilities.




