HeadPowder, a leading enterprise in industrial material handling solutions, specializes in the design and manufacturing of tote bag unpacking and powder material handling equipment. This equipment is engineered to facilitate the efficient transfer of bulk powders from tote bags into downstream processing systems, thereby optimizing material flow and enhancing operational efficiency across various industrial sectors.
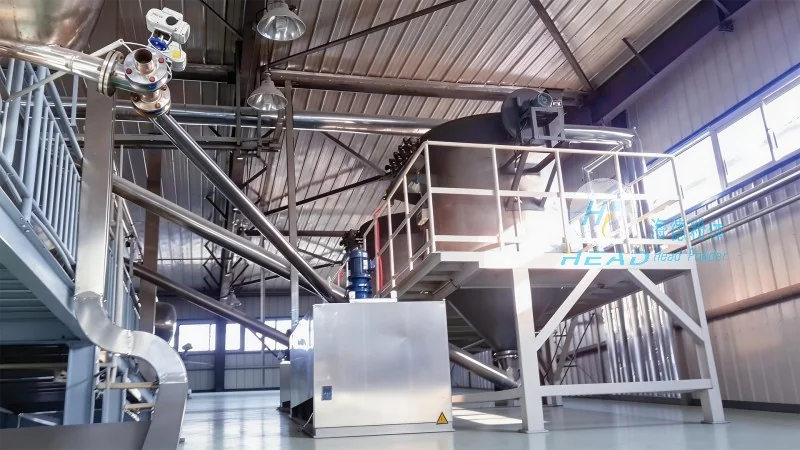
Principle of Tote Bag Unpacking Equipment
The fundamental principle of tote bag unpacking equipment revolves around automated or semi-automated processes that enable the opening, emptying, and transfer of powder materials from tote bags. These systems typically comprise components such as bag openers, conveyors, and material feed mechanisms. The operation begins with the positioning of the tote bag, followed by the activation of mechanical or pneumatic systems to open the bag's top. This action allows the powder to flow into a hopper or conveyor system, which then transports the material to the processing unit. This automated approach significantly reduces manual labor, minimizes dust exposure, and enhances workplace safety by eliminating direct human contact with powders.
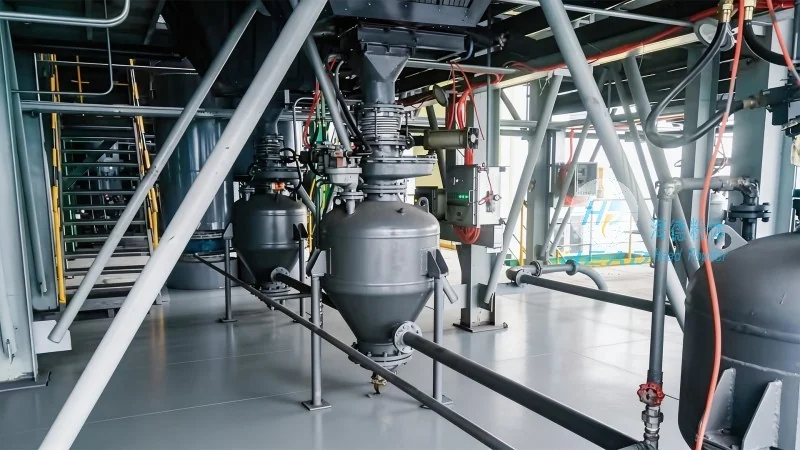
Working Scene Characteristics of Powder Material Handling Equipment
HeadPowder's powder material handling equipment is tailored to meet the diverse demands of industrial environments, including chemical, pharmaceutical, food processing, and mining industries. The equipment is designed to handle a wide spectrum of powder types, ranging from fine powders to bulkier materials, with adjustable parameters to accommodate varying material properties. In industrial settings, these systems are critical for maintaining consistent material flow, reducing downtime, and improving overall production efficiency. The working scenes often involve seamless integration with existing processing lines, ensuring that materials are transferred from storage to processing units without interruption.
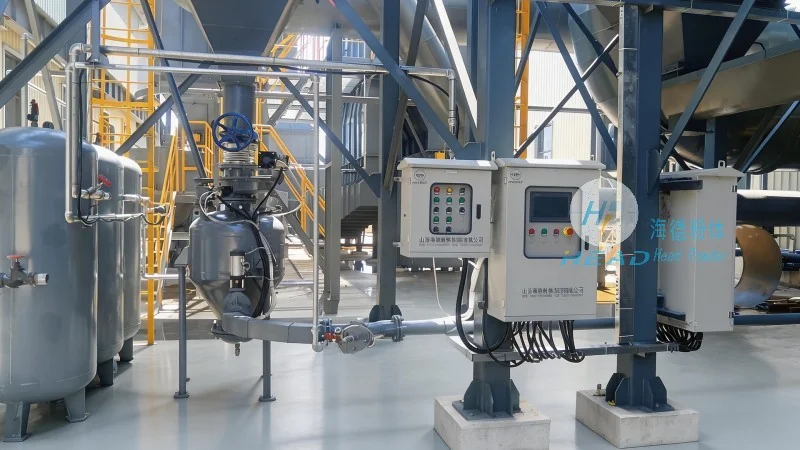
Key Features and Advantages
HeadPowder's tote bag unpacking and powder handling equipment offers several key advantages that contribute to enhanced operational performance. These include high throughput rates, which allow for rapid material transfer, and reduced labor costs due to automated operations. The equipment also prioritizes safety by minimizing human exposure to powders, thereby lowering the risk of respiratory issues or contamination. Additionally, the systems are engineered for easy maintenance and cleaning, which is essential for industries with stringent hygiene standards, such as pharmaceutical and food processing. The scalability of the equipment enables businesses to adapt to growing production needs, making it a long-term investment for industrial operations.
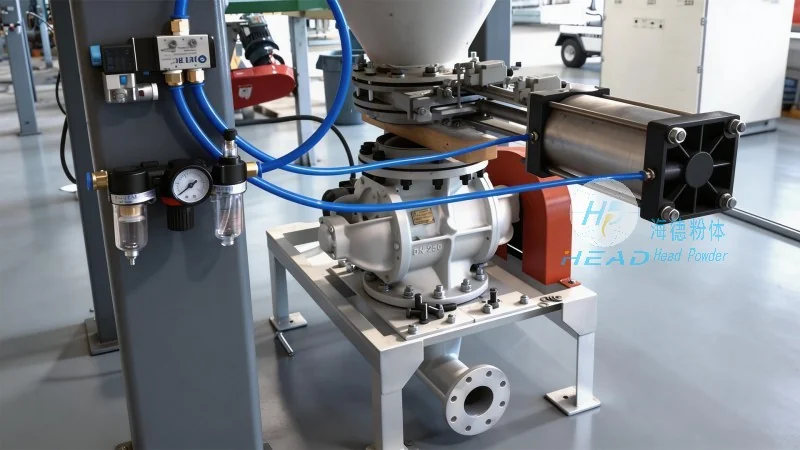
Application Examples in Industrial Settings
In a chemical manufacturing facility, the equipment is utilized to transfer bulk powders like calcium carbonate or silica into mixing tanks. The tote bags are unloaded automatically, and the powder is conveyed directly to the processing line, eliminating the need for manual shoveling or bag emptying. This automation not only speeds up the material transfer process but also ensures consistent material quality. In a pharmaceutical plant, the equipment operates under controlled conditions to transfer raw materials, maintaining product purity and compliance with regulatory standards. The consistent flow of materials helps in reducing batch-to-batch variations, leading to more stable and reliable production outcomes. Similarly, in food processing industries, the equipment ensures hygienic transfer of powders like flour or sugar, adhering to food safety regulations and preventing cross-contamination.




