Efficient material handling is a critical component in the cotton seed processing industry, and the design of specialized transport systems plays a pivotal role in optimizing operational efficiency and ensuring product quality. The cotton seed material handling system, as developed by Shandong HeadPowder Engineering Co., Ltd. (hereinafter referred to as HeadPowder), is engineered to address the unique challenges associated with cotton seed transportation, storage, and processing. This system integrates advanced mechanical and control technologies to provide a reliable solution for various industrial applications.
Principle of the Cotton Seed Material Handling System
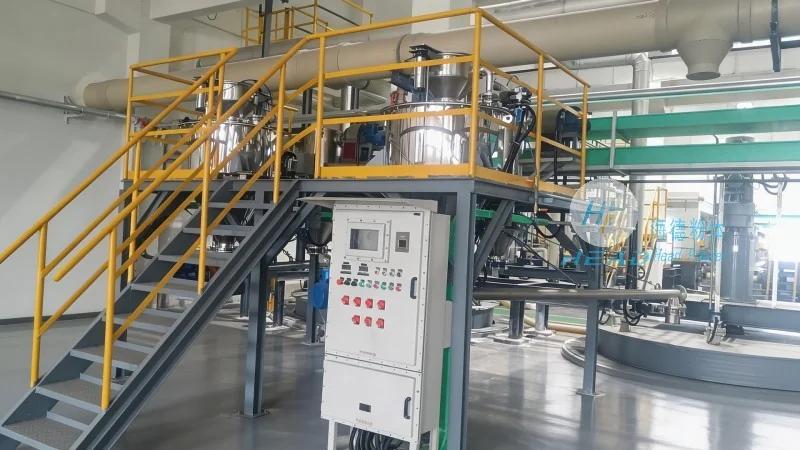
The core principle of the cotton seed material handling system lies in its ability to handle bulk materials with precision and efficiency. The system typically comprises several key components, including feeders, conveyors, storage silos, and control units. The feeders are designed to uniformly distribute cotton seeds into the conveyor system, ensuring consistent flow rates. The conveyors, which may include belt conveyors, screw conveyors, or pneumatic conveyors, are selected based on the specific characteristics of the cotton seed, such as size, moisture content, and bulk density. The storage silos are equipped with level sensors and aeration systems to maintain optimal conditions for the cotton seeds, preventing spoilage and maintaining quality. The control unit integrates all components, allowing for real-time monitoring and adjustment of the system parameters to adapt to varying production demands.
Working Scene Characteristics of the Cotton Seed Material Handling System
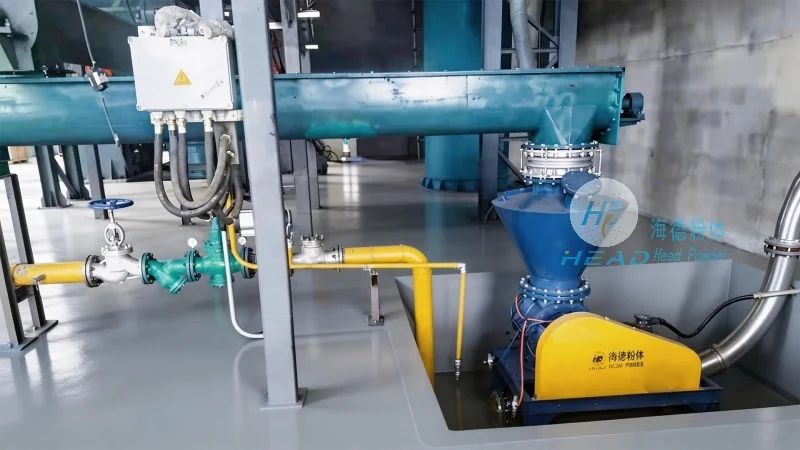
The working scene characteristics of the cotton seed material handling system are tailored to meet the diverse needs of different industrial environments. In cotton seed processing plants, the system is commonly used for the initial reception of raw cotton seeds, the transfer between processing stages (such as cleaning, dehulling, and oil extraction), and the final storage of processed products. The system's adaptability allows it to operate in both indoor and outdoor settings, with options for enclosed or open structures depending on the environmental conditions and local regulations. The design also considers the safety and hygiene requirements of the food processing industry, ensuring that the materials are handled in a clean and controlled manner to meet regulatory standards. Additionally, the system's modular design enables easy integration with existing production lines, minimizing downtime during installation and maintenance.
Company Background and Expertise
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced material handling systems for various industries, including agriculture, food processing, and chemical manufacturing. With years of experience in the field, HeadPowder has developed a deep understanding of the unique requirements of cotton seed processing, allowing them to provide customized solutions that enhance operational efficiency and reduce costs. The company's commitment to quality and innovation has earned it a reputation for delivering reliable and durable equipment that meets the highest industry standards. HeadPowder's team of engineers and technicians work closely with clients to understand their specific needs and provide tailored solutions that address their unique challenges.
Key Features and Advantages
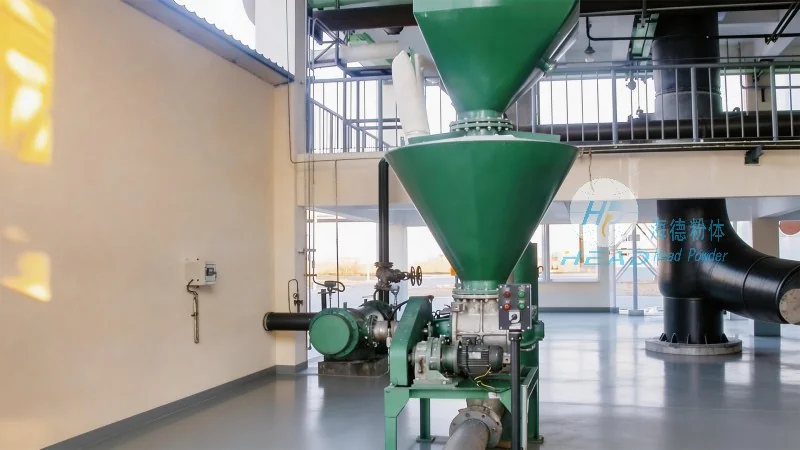
The cotton seed material handling system developed by HeadPowder offers several key features and advantages that make it an ideal choice for cotton seed processing facilities. One of the primary advantages is its high efficiency, which is achieved through the integration of advanced control technologies and optimized component design. The system is capable of handling large volumes of cotton seeds with minimal energy consumption, reducing operational costs for the end-user. Another key feature is its durability and reliability, which is ensured by the use of high-quality materials and rigorous testing procedures. The system is designed to withstand the harsh conditions of industrial environments, ensuring long-term performance and minimal maintenance requirements. Additionally, the system's flexibility allows it to be customized to meet the specific needs of different clients, including different conveyor types, storage capacities, and control systems. This customization capability ensures that the system can be integrated seamlessly into existing production lines, minimizing disruption to operations.
Application Examples and Case Studies
The effectiveness of the cotton seed material handling system has been demonstrated in various real-world applications. For example, in a cotton seed processing plant in China, HeadPowder's system was installed to handle the transportation of raw cotton seeds from the reception area to the cleaning and dehulling stages. The system was designed to handle a daily throughput of 500 tons of cotton seeds, with a conveyor capacity of 200 tons per hour. The system's performance was evaluated over a period of six months, and the results showed that the system achieved a throughput of 520 tons per day, with an energy consumption of 0.8 kWh per ton. The system's reliability was also tested, with a downtime of only 2 hours during the six-month period. Another example is a cotton seed oil extraction plant in the United States, where HeadPowder's system was used to transfer processed cotton seeds from the storage silos to the oil extraction equipment. The system was designed to handle a daily throughput of 300 tons of processed cotton seeds, with a conveyor capacity of 150 tons per hour. The system's performance was evaluated over a period of one year, and the results showed that the system achieved a throughput of 320 tons per day, with an energy consumption of 0.6 kWh per ton. The system's reliability was also tested, with a downtime of only 1 hour during the one-year period. These case studies demonstrate the effectiveness of the cotton seed material handling system in improving operational efficiency and reducing costs for cotton seed processing facilities.




