Pneumatic conveying technology has become an essential method for transporting bulk materials, especially in industries dealing with fine powders like urea. Urea, a critical nitrogen fertilizer, requires efficient and reliable transport systems to ensure smooth production and supply chain operations. The principle of pneumatic conveying involves using air to move solid particles through a pipeline, eliminating the need for mechanical components that might cause wear or contamination. This method is particularly advantageous for urea powder due to its hygroscopic nature and fine particle size, which can make traditional belt or bucket conveyors less effective.
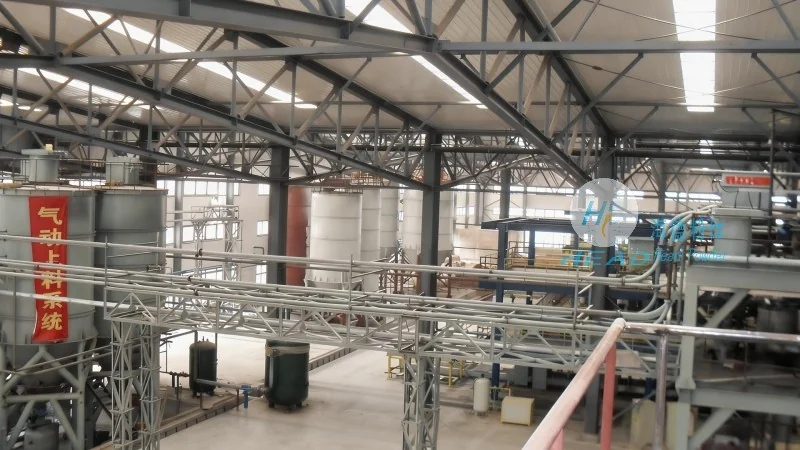
The core of a urea powder pneumatic conveying system lies in its ability to handle the material's unique characteristics. Urea particles are typically small, ranging from 0.1 to 2 millimeters, and have a tendency to stick together or agglomerate. To address this, specialized equipment such as rotary valves, feeders, and airlocks are used to ensure consistent and controlled material flow. The system operates by creating a pressure differential between the inlet and outlet of the pipeline. In an aspirating system, air is drawn through the material, while in a pressurized system, air is forced through the material under pressure. Both methods effectively transport urea powder from the source to the destination, with the choice depending on the distance, material volume, and operational requirements.
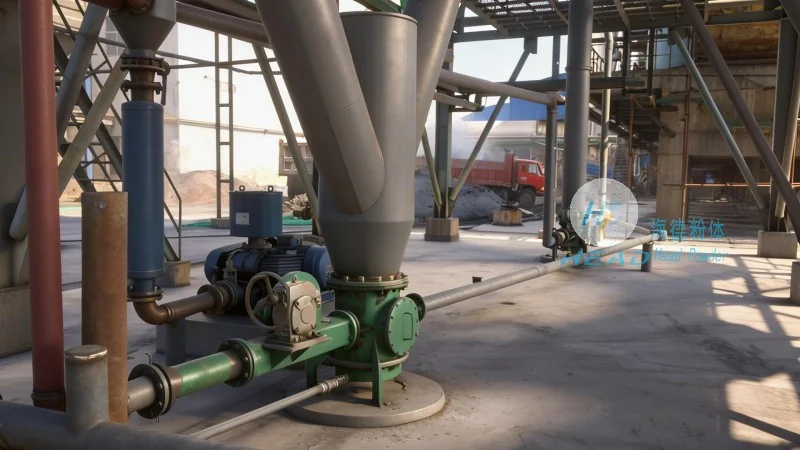
Key components of a urea powder pneumatic conveying equipment include the material feeder, which feeds the urea into the conveying line, the conveying pipeline itself, and the separation and recovery system. The feeder ensures a uniform flow rate, preventing blockages or uneven material distribution. The pipeline is designed with smooth surfaces and appropriate diameters to minimize friction and particle degradation. The separation system, often a cyclone or bag filter, removes the urea powder from the air stream, allowing the air to be recycled or vented. This design not only improves efficiency but also maintains the purity of the urea, which is crucial for its quality as a fertilizer.
Application Scenarios and Operational Benefits
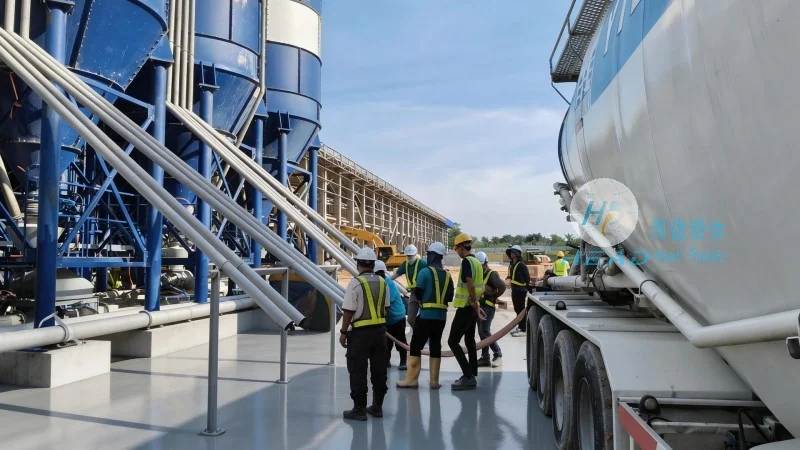
In terms of application scenarios, urea powder pneumatic conveying equipment is widely used in various industrial and agricultural settings. In large-scale fertilizer production plants, the equipment is employed to transport urea from storage silos to processing units or packaging lines. This continuous operation ensures a steady supply of raw material, enhancing production efficiency. In agricultural storage facilities, the system is used for loading and unloading urea from trucks or railcars, facilitating quick turnaround times and reducing labor costs. Additionally, in chemical processing plants, the equipment may be integrated into larger production lines to transport urea to other processing stages, such as granulation or coating.
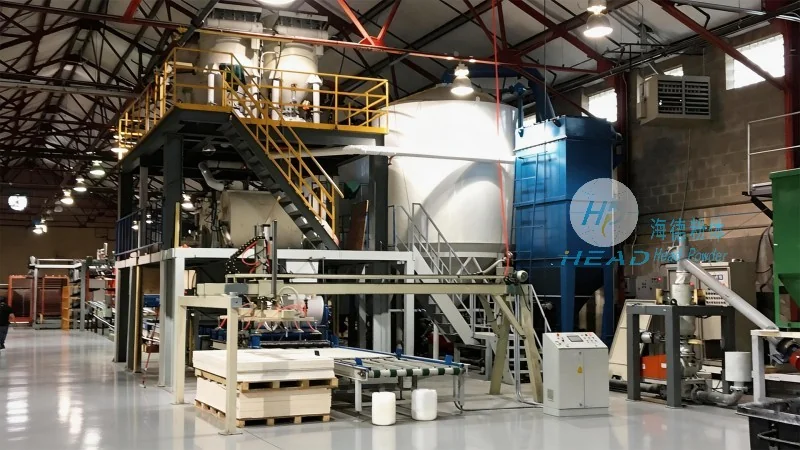
The advantages of using pneumatic conveying for urea powder are significant. Unlike mechanical conveyors, which can cause particle attrition and contamination, pneumatic systems maintain the integrity of the urea particles. This is vital for maintaining the fertilizer's effectiveness and compliance with quality standards. Furthermore, the system is hygienic and easy to clean, which is essential in food and agricultural industries where product purity is paramount. The flexibility of pneumatic conveying also allows for changes in material flow rates and distances, making it adaptable to different operational needs.
HeadPowder: Specialized Solutions for Urea Handling
HeadPowder, a leading manufacturer of pneumatic conveying equipment, specializes in providing customized solutions for urea powder handling. With a strong presence in Shandong, China, HeadPowder Engineering Co., Ltd. leverages years of experience to design and produce equipment that meets the specific requirements of urea production and distribution. Their systems are engineered to handle the unique challenges of urea powder, ensuring reliable and efficient operation in diverse application scenarios. By focusing on quality and innovation, HeadPowder has established itself as a trusted partner in the fertilizer industry, delivering equipment that enhances productivity and product quality.
Conclusion
In conclusion, urea powder pneumatic conveying equipment combines advanced technology with practical application to address the specific needs of urea handling. From its fundamental principles to real-world scenarios, the system offers a robust solution for transporting urea efficiently and safely. With companies like HeadPowder providing specialized equipment, the industry can rely on reliable systems that support consistent production and supply chain operations.




