HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for the fermentation industry. Our Fermented Grain Pneumatic Conveyor is engineered to efficiently handle the unique challenges of transporting fermented grains, ensuring optimal performance and reliability in various production environments.
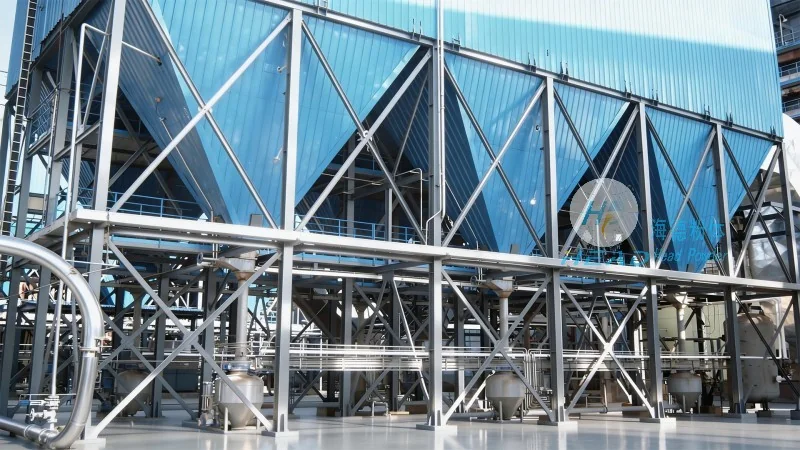
Introduction to Fermented Grain Pneumatic Conveyor
The Fermented Grain Pneumatic Conveyor by Shandong HeadPowder Engineering Co., Ltd. is a sophisticated air-powered system designed to transport fermented grains with precision and efficiency. This equipment is essential for modern breweries and distilleries, where consistent and hygienic material handling is critical to maintaining product quality and operational productivity. The conveyor utilizes a combination of air pressure and vacuum to move materials through a sealed pipeline, minimizing contamination and loss while optimizing energy consumption.
Key Features and Technical Specifications
Our Fermented Grain Pneumatic Conveyor incorporates several key features that enhance its performance and adaptability. The system is equipped with high-quality materials resistant to corrosion and abrasion, ensuring durability even with abrasive fermented grain particles. The design includes adjustable air flow control mechanisms, allowing operators to fine-tune the conveying speed based on the specific characteristics of the material being transported. Additionally, the conveyor features a compact and modular structure, facilitating easy installation and integration into existing production lines. The system operates under low pressure, reducing energy costs and minimizing the risk of material degradation during transport.
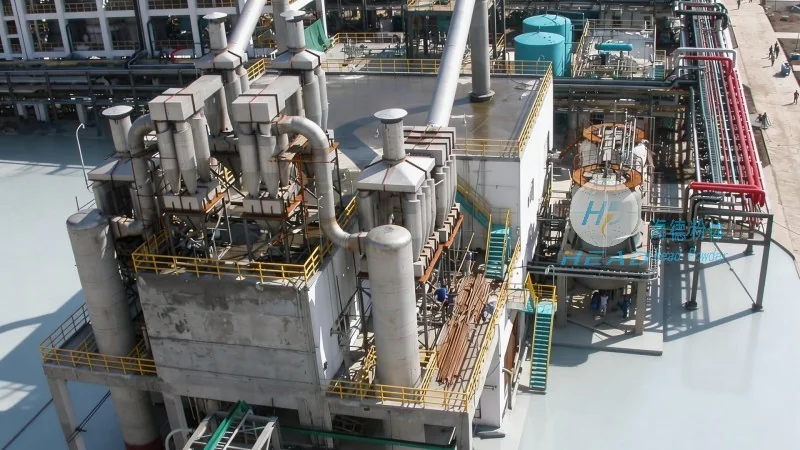
Operation Process of Fermented Grain Pneumatic Conveyor
The operation of the Fermented Grain Pneumatic Conveyor involves several sequential steps that ensure smooth and efficient material transfer. The process begins with the loading of fermented grains into the hopper or feeding chamber. The system then activates the air compressor, which generates the necessary air pressure to initiate the conveying process. As the air flows through the pipeline, it creates a vacuum that draws the fermented grains from the hopper into the conveyor. The grains are then propelled through the pipeline by the air current, reaching the discharge point where they are deposited into the receiving container. The entire operation is controlled by an automated system that monitors air pressure, flow rate, and material level, ensuring consistent performance and preventing system overload.
Working Principle of Fermented Grain Pneumatic Conveyor
The working principle of the Fermented Grain Pneumatic Conveyor is based on the fundamental physics of air flow and particle movement. The system operates on the principle of pneumatic transport, where compressed air is used to move solid materials through a sealed pipeline. The conveyor consists of a series of components, including a hopper, air compressor, pipeline, and discharge valve. The air compressor generates a high-pressure air stream that is directed into the pipeline. As the air flows through the pipeline, it creates a low-pressure zone at the discharge end, which draws the fermented grains into the pipeline. The grains are then carried by the air current, moving from the inlet to the outlet. The speed and distance of the conveying process are determined by the air pressure, flow rate, and the physical properties of the fermented grains, such as particle size and moisture content. The system is designed to maintain a consistent air flow, ensuring that the grains are transported without clogging or degradation.
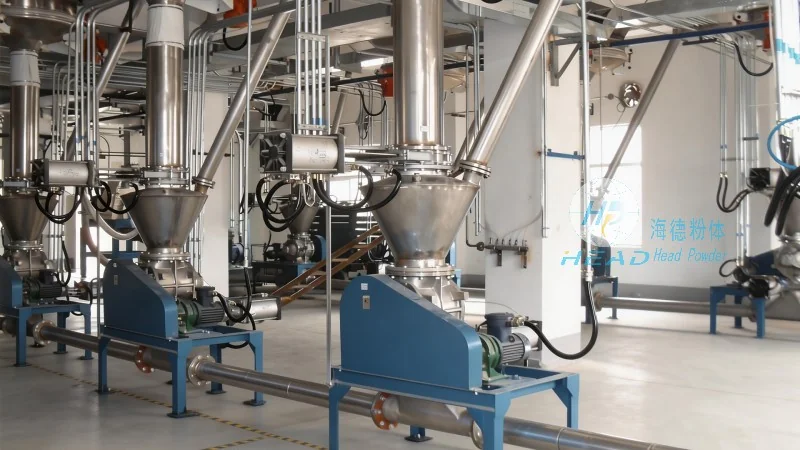
Application and Benefits in Fermentation Industry
The Fermented Grain Pneumatic Conveyor is widely used in the fermentation industry for the efficient handling of fermented grains, including those used in beer, wine, and spirits production. The system offers several benefits, including improved hygiene and sanitation, as the sealed pipeline prevents contamination from external sources. It also reduces material loss and waste, as the conveyor minimizes spillage and dust during transport. Additionally, the system enhances operational efficiency by automating the material handling process, reducing labor costs and increasing production throughput. The low energy consumption of the conveyor makes it an environmentally friendly solution, aligning with the sustainability goals of modern fermentation facilities.
Company Profile and Commitment to Quality
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is a reputable manufacturer dedicated to providing high-quality pneumatic conveying solutions for the fermentation industry. Our company has a strong commitment to research and development, continuously improving our products to meet the evolving needs of our clients. We adhere to strict quality control standards, ensuring that every Fermented Grain Pneumatic Conveyor meets the highest industry benchmarks. Our team of experienced engineers and technicians provides comprehensive support, from design and installation to maintenance and troubleshooting. We are committed to delivering reliable and efficient equipment that enhances the productivity and profitability of our clients' operations.




