Sodium nitrate, a critical chemical compound widely used in industries such as fertilizer production, glass manufacturing, and metal processing, requires efficient and reliable powder conveying systems to ensure smooth operation and safety. The process of transporting sodium nitrate powder involves several key stages, each designed to maintain the material's integrity and minimize operational risks. This article provides a detailed overview of the operation process and working principles of sodium nitrate powder conveying systems, highlighting the technical aspects and practical considerations for effective implementation.
Key Components of the Conveying System
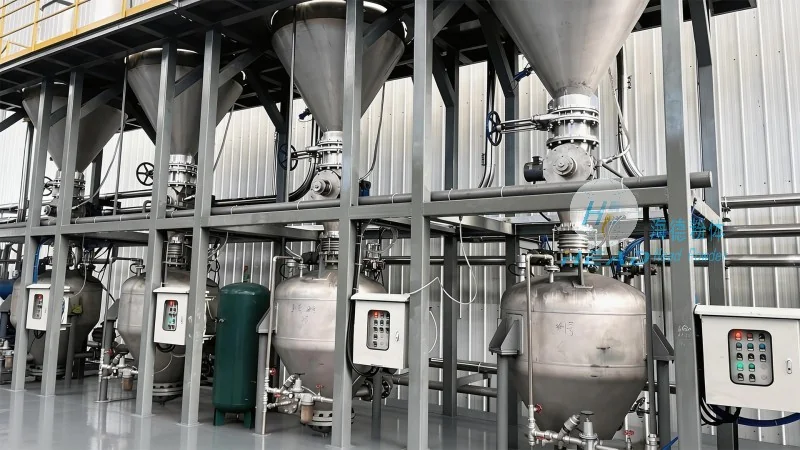
The sodium nitrate powder conveying system typically consists of several interconnected components that work in tandem to achieve seamless material transport. These components include hoppers for material storage, feeders to control the flow rate, conveying equipment such as pneumatic or mechanical systems, and discharge mechanisms. Each component plays a crucial role in maintaining the system's efficiency and ensuring the safe handling of sodium nitrate, which is a potentially hazardous material due to its reactivity and potential for dust explosions.
Working Principle of the Conveying Process
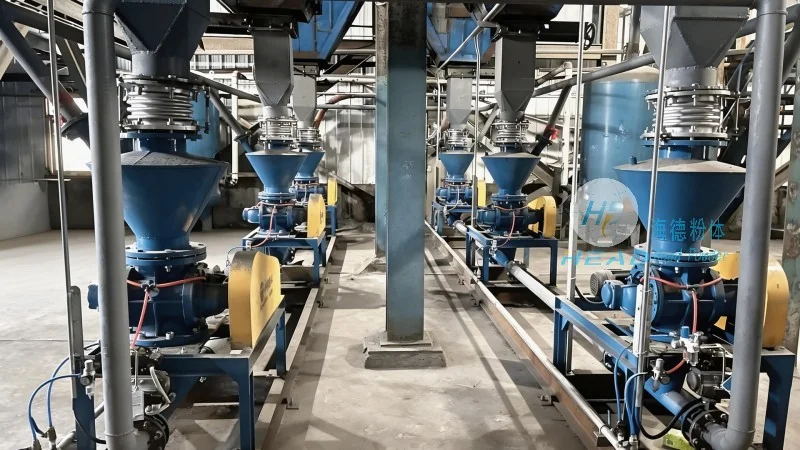
The operation of the sodium nitrate powder conveying system begins with the material being loaded into the hopper. The feeder then regulates the flow of the powder into the conveying line, ensuring a consistent and controlled rate. For pneumatic conveying systems, compressed air is used to create a flow of air and powder through the pipeline, while mechanical systems rely on screws, belts, or other mechanisms to move the material. The system's design must account for the material's properties, such as its density, flowability, and potential for caking, to prevent blockages and ensure continuous operation.
Control and Monitoring Systems
Modern sodium nitrate powder conveying systems incorporate advanced control and monitoring technologies to optimize performance and enhance safety. These systems include sensors to detect material levels, pressure, and flow rates, as well as control panels that allow operators to adjust parameters in real-time. The integration of these technologies enables precise control over the conveying process, reducing the risk of overfilling, underfilling, or system failures. Additionally, the systems are equipped with safety features such as dust suppression and explosion-proof designs to comply with industrial safety standards.
HeadPowder Engineering's Expertise in Sodium Nitrate Conveying
Shandong HeadPowder Engineering Co., Ltd., a leading provider of powder handling solutions, specializes in designing and manufacturing customized sodium nitrate powder conveying systems tailored to the specific needs of clients. With years of experience in the industry, HeadPowder has developed a deep understanding of the unique challenges associated with handling sodium nitrate, including its reactivity and the need for precise control. The company's team of engineers and technicians work closely with clients to assess their requirements, conduct feasibility studies, and provide comprehensive solutions that meet both operational and safety standards.
Benefits of an Efficient Conveying System
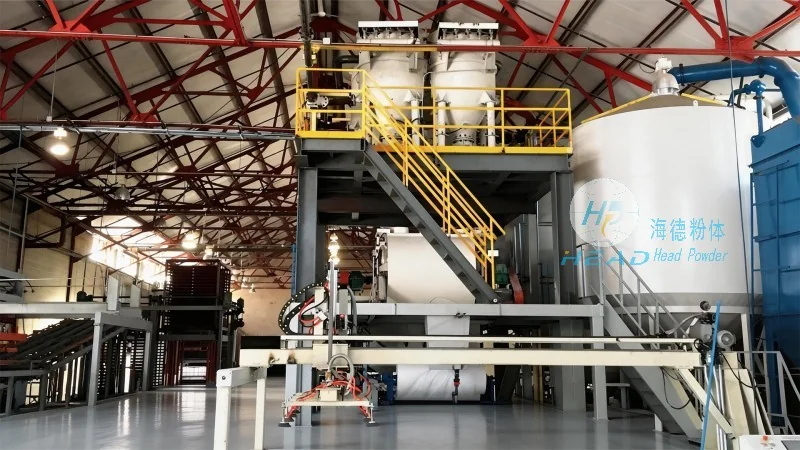
Implementing an efficient sodium nitrate powder conveying system offers numerous benefits for industrial operations. These include improved productivity through reduced downtime, enhanced safety by minimizing the risk of dust explosions and material handling accidents, and cost savings from optimized material usage and reduced maintenance. Additionally, the system's ability to maintain the material's quality and prevent contamination ensures that the final product meets the required specifications, which is crucial for applications such as fertilizer production where purity is essential.
Conclusion
In conclusion, the operation process and working principles of sodium nitrate powder conveying systems are complex and require careful consideration of the material's properties and industrial requirements. By leveraging advanced technology and expert engineering, companies like Shandong HeadPowder Engineering Co., Ltd. can provide reliable and efficient solutions that enhance operational performance and ensure safety. The continuous development of these systems will play a vital role in supporting the growth of industries that rely on sodium nitrate as a key raw material.




