Efficient material handling is a critical factor in the success of agricultural processing operations, particularly for millet, a staple grain used in various food products. The millet material handling system equipment, manufactured by Shandong HeadPowder Engineering Co., Ltd., is a specialized solution designed to streamline the entire material transport process from raw millet intake to final product delivery. This equipment integrates advanced engineering and control technologies to provide reliable, high-performance, and energy-efficient material handling capabilities for modern grain processing facilities.
Introduction to Millet Material Handling System Equipment
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of millet material handling systems, providing customized solutions for agricultural processing enterprises. The system is engineered to handle the entire millet processing workflow, including cleaning, drying, grading, and packaging. Each component of the system is designed with durability and efficiency in mind, ensuring long-term performance and minimal maintenance. The equipment is constructed using high-quality materials and advanced manufacturing techniques, meeting industry standards for safety and reliability. The company's expertise in agricultural machinery ensures that the system is tailored to the specific needs of each client, optimizing production efficiency and reducing operational costs.
Key Components and Their Roles in the System
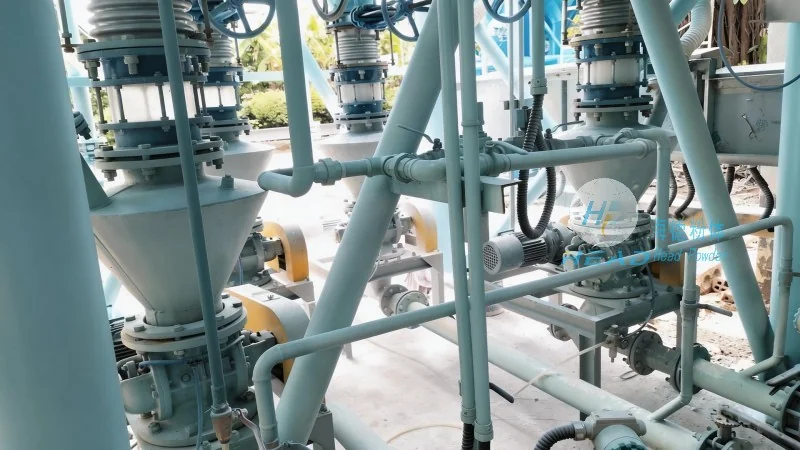
The millet material handling system comprises several essential components, each playing a crucial role in the overall operation. The primary components include feeders, conveyors, elevators, and storage bins. Feeders are responsible for uniformly distributing raw millet into the system, ensuring consistent material flow. They use gravity or mechanical force to move the material from the hopper into the conveyor. Conveyors, such as belt conveyors or chain conveyors, transport the millet horizontally or at an incline, moving it from one processing stage to another. These conveyors are designed with smooth surfaces and appropriate speeds to prevent material damage and ensure efficient transport. Elevators, like bucket elevators or screw conveyors, lift the material vertically, converting horizontal motion into vertical movement. This allows for vertical transport between different levels of the processing facility, enabling the system to handle multi-level operations. Storage bins are used to temporarily hold millet during processing, providing a buffer to maintain steady production rates. The bins are designed with proper ventilation and discharge mechanisms to prevent material spoilage and ensure easy access for downstream equipment.
Step-by-Step Operation Process
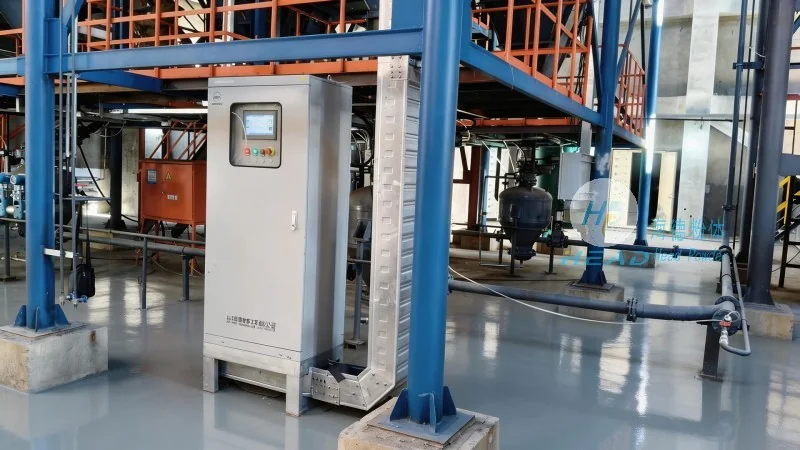
The operation of the millet material handling system follows a systematic sequence to ensure seamless material transport and processing. The process begins with the raw millet being fed into the system via a hopper or feeder. The feeder evenly distributes the material into the conveyor system, ensuring a consistent flow rate. The conveyor transports the millet to the first processing unit, such as a cleaning machine or a dehusking machine. After processing, the material is moved to the next stage via the conveyor system. The elevators lift the material vertically to the next level or to the storage bins. The storage bins hold the processed millet until it is needed for packaging or further processing. The control system monitors the operation of all components, adjusting speeds and flow rates as needed to maintain optimal performance. Sensors are used to detect material levels, blockages, or malfunctions, triggering automatic responses to prevent downtime. The system operates continuously, with each component working in sync to maintain a steady flow of material, ensuring high production efficiency and minimal waste.
Working Principle Explained
The working principle of the millet material handling system is based on mechanical and pneumatic systems that work together to move and process the material. The feeders use gravity or mechanical force to distribute the millet into the conveyor. The conveyors use friction or mechanical engagement to move the material along the path. Elevators use buckets or screws to lift the material vertically, converting horizontal motion into vertical movement. The storage bins use gravity to release the material when needed, ensuring a controlled flow to downstream equipment. The control system uses sensors and feedback mechanisms to monitor the system's performance, adjusting parameters in real-time to optimize operation. This integrated approach ensures that the system operates efficiently, reliably, and with minimal energy consumption. The mechanical design minimizes friction and wear, while the control system maximizes energy efficiency by adjusting speeds based on the material load and processing requirements.
Benefits and Advantages for Agricultural Processing
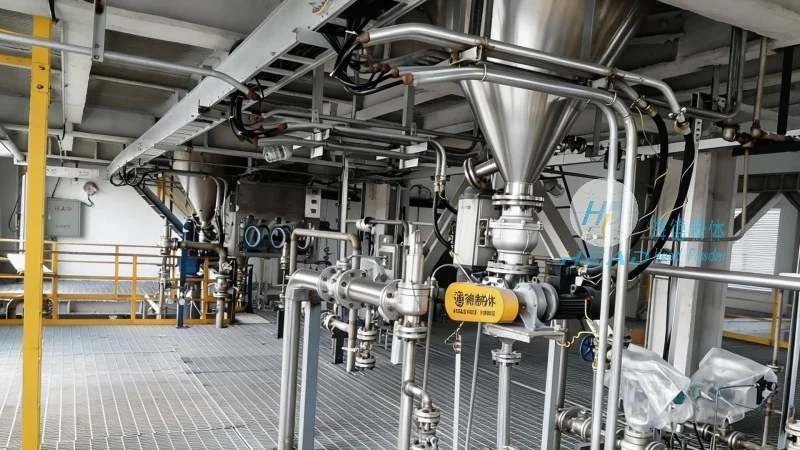
Implementing a millet material handling system from Shandong HeadPowder Engineering Co., Ltd. offers numerous benefits for agricultural processing businesses. Firstly, the system enhances operational efficiency by automating the material transport process, reducing manual labor and minimizing human error. This leads to higher production rates and lower labor costs. Secondly, the system improves product quality by ensuring consistent material flow and preventing contamination during transport. The uniform handling of millet reduces damage and ensures that the final product meets quality standards. Thirdly, the system increases production capacity by maintaining steady material throughput, allowing businesses to scale up operations without additional infrastructure. Additionally, the system reduces energy consumption and operational costs through optimized control and efficient design. The durable construction of the equipment ensures long-term performance, providing a high return on investment for businesses. The customization options allow clients to tailor the system to their specific processing needs, ensuring maximum efficiency and productivity.
Application Examples and Customization Options
The millet material handling system is widely used in various agricultural processing applications, including grain mills, feed mills, and food processing plants. In grain mills, the system is used to handle cleaning, dehusking, and grading operations, ensuring that the final product is of high quality. In feed mills, the system transports feed ingredients and mixes them into the final feed product, improving the consistency and quality of the feed. The system can also be used in food processing plants for handling millet-based products, such as flour or snacks. Shandong HeadPowder Engineering Co., Ltd. works closely with clients to understand their processing requirements and design a system that maximizes efficiency and productivity. Customization options include different conveyor types, elevator capacities, and storage bin sizes, allowing businesses to tailor the system to their unique needs. The company provides technical support and after-sales service to ensure that the system operates at peak performance throughout its lifespan.




