

Analysis of Diatomite Powder Pneumatic Conveying Systems
For industrial applications that require the efficient and reliable transport of diatomite powder, the selection of an appropriate pneumatic conveying system is crucial. This article provides a detailed analysis of such systems, focusing on the technical aspects, operational benefits, and practical considerations for industries dealing with diatomite materials. The discussion is centered around the solutions offered by Shandong HeadPowder Engineering Co., Ltd., a company specializing in engineering and manufacturing of pneumatic conveying equipment.
Understanding Pneumatic Conveying Systems for Diatomite Powder
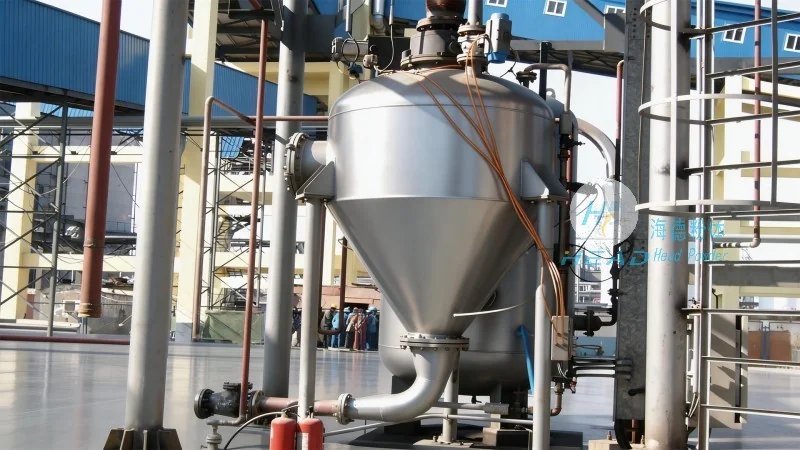
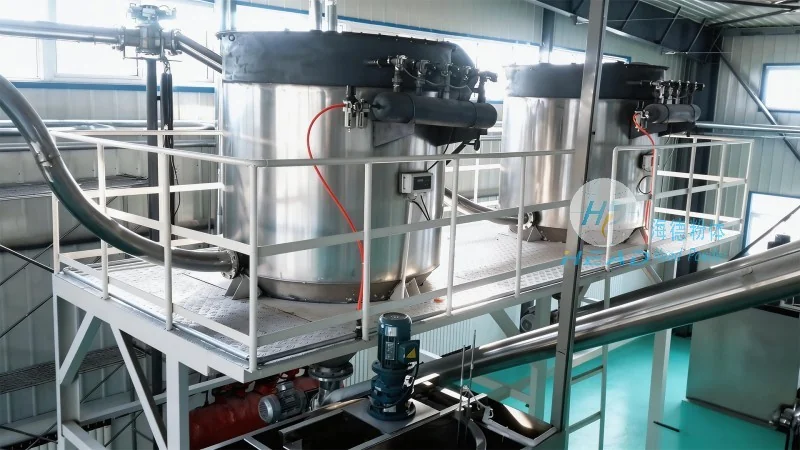
Pneumatic conveying systems utilize air or gas to transport bulk materials like diatomite powder through a pipeline network. These systems are designed to handle fine powders efficiently, minimizing material loss and ensuring consistent flow. The core components of a typical diatomite pneumatic conveying system include a material feeder, a conveying line, a dust collector, and a control system. The material feeder, often a rotary valve or a screw feeder, ensures a steady supply of diatomite powder into the system. The conveying line, made of corrosion-resistant materials such as stainless steel or polyethylene, prevents material degradation and maintains system integrity. A dust collector is essential to capture any airborne particles, ensuring environmental compliance and operational safety. The control system manages the air pressure, flow rate, and material feed rate, optimizing the conveying process.
Key Features and Benefits of Diatomite Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd. offers advanced pneumatic conveying systems tailored to the unique properties of diatomite powder. These systems are engineered to handle the fine, lightweight nature of diatomite, which can be prone to caking or agglomeration if not managed properly. The company's solutions incorporate features such as high-efficiency material feed mechanisms, adjustable air pressure controls, and robust filtration systems. The benefits of using such systems include reduced labor costs, increased production efficiency, and improved product quality. By minimizing material handling errors and ensuring consistent particle size distribution, the systems contribute to higher overall operational performance. Additionally, the use of corrosion-resistant materials in the construction of the conveying lines ensures long-term durability, even in harsh industrial environments.
Operational Considerations and Maintenance
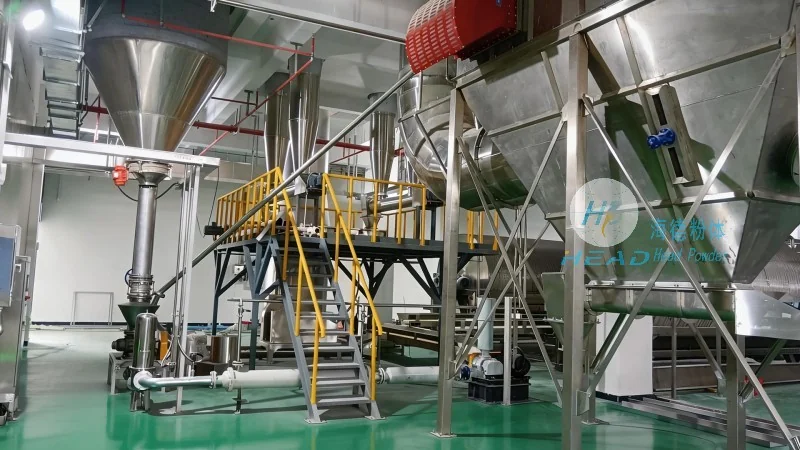
Effective operation of a diatomite pneumatic conveying system requires careful consideration of several factors. The system's design must account for the specific flow characteristics of diatomite powder, including its density, moisture content, and particle size distribution. Proper sizing of the conveying line and air compressor is critical to achieve optimal performance without excessive energy consumption. Regular maintenance is essential to ensure the system operates at peak efficiency. This includes cleaning the dust collector, inspecting the conveying line for wear, and checking the performance of the material feeder. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive maintenance services and technical support to help clients maintain their systems in optimal condition, extending their operational lifespan and reducing downtime.
Application Examples and Industry Impact
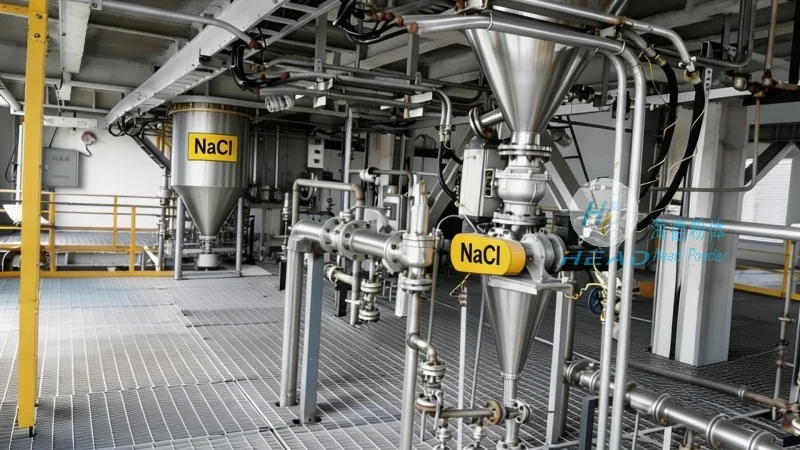
The applications of diatomite pneumatic conveying systems span various industries, including construction, pharmaceuticals, and food processing. In the construction industry, diatomite is used as a lightweight aggregate in concrete and insulation materials. The efficient transport of diatomite powder ensures consistent quality in these products, meeting stringent industry standards. In the pharmaceutical sector, diatomite is used as a filter aid and filler, requiring precise handling to maintain product purity. The systems from Shandong HeadPowder Engineering Co., Ltd. help pharmaceutical manufacturers achieve the required cleanliness and consistency in their processes. Similarly, in the food industry, diatomite is used as a clarifying agent in beverages and as a filler in nutritional supplements. The reliable operation of the conveying systems ensures that food products meet safety and quality regulations. By providing consistent and efficient material transport, these systems enhance the overall productivity and competitiveness of businesses across multiple sectors.