Mineral sand, such as ilmenite, rutile, and zircon, serves as a vital raw material across multiple industries including titanium dioxide production, ceramics, and glass manufacturing. The efficient and reliable transportation of these bulk materials from extraction sites to processing facilities is fundamental to maintaining production efficiency and minimizing operational costs. This article provides an introduction to mineral sand conveying systems, with a focus on the advantages of pneumatic conveying technology.
Introduction to Mineral Sand Conveying Systems
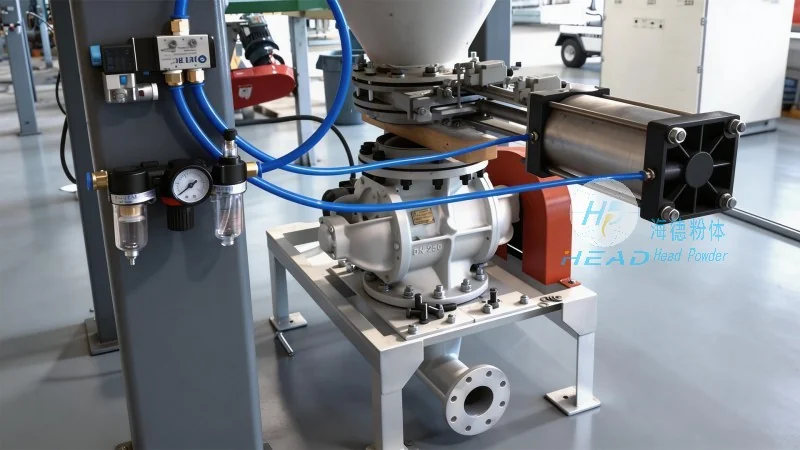
Conveying systems are critical components in mineral sand processing operations, responsible for transporting materials over short or long distances. Traditional methods like belt conveyors and bucket elevators have been widely utilized, yet they often encounter challenges such as material degradation, high maintenance requirements, and limited flexibility in layout. In contrast, pneumatic conveying systems offer a more advanced solution that addresses many of these limitations.
The Advantages of Pneumatic Conveying for Mineral Sands
Pneumatic conveying, also known as air conveying, employs compressed air to transport dry bulk materials like mineral sands through a pipeline network. This method provides several key advantages over traditional mechanical conveyors. First, it eliminates physical contact between the material and conveyor components, reducing the risk of material degradation and contamination. This is particularly important for mineral sands, which may contain valuable components that could be damaged by abrasion or friction.
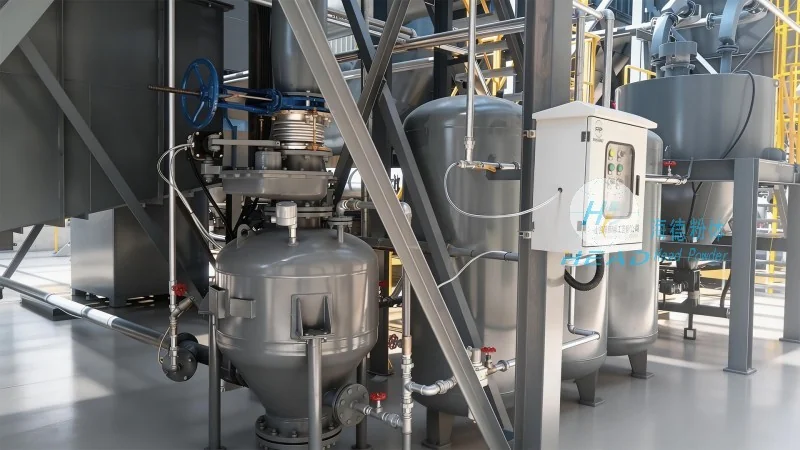
Second, pneumatic conveying systems offer greater flexibility in terms of layout and routing. The pipeline can be easily reconfigured to adapt to changes in production processes or facility expansions, without the need for extensive civil engineering work. This flexibility also allows for more compact system designs, saving valuable floor space in processing plants.
Third, the technology provides excellent control over material flow and pressure, enabling precise dosing and regulation of the conveying process. This level of control is essential for maintaining consistent product quality and optimizing production rates. Additionally, pneumatic systems can handle a wide range of material characteristics, including different particle sizes, densities, and moisture contents, making them suitable for diverse mineral sand applications.
Key Features of Pneumatic Conveying Systems for Mineral Sands
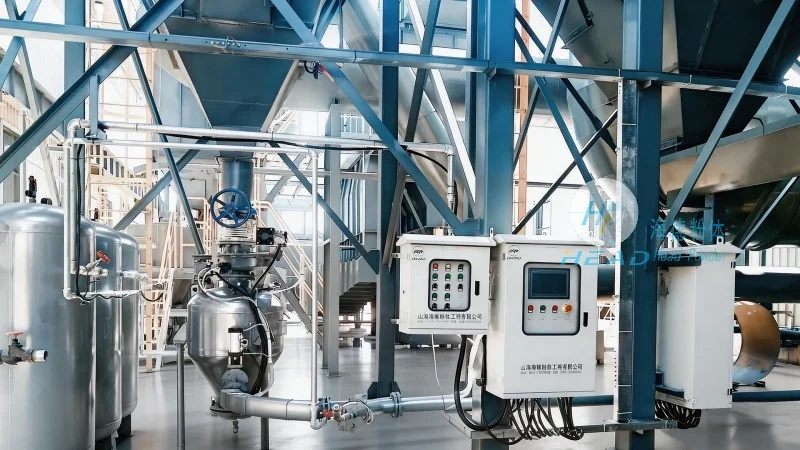
Modern pneumatic conveying systems for mineral sands are equipped with advanced features that enhance performance and reliability. These systems typically include components such as air compressors, dust collectors, and material feeders. The air compressor generates the necessary pressure to move the material through the pipeline, while the dust collector ensures that the air is filtered and returned to the system, preventing dust emissions and maintaining air quality.
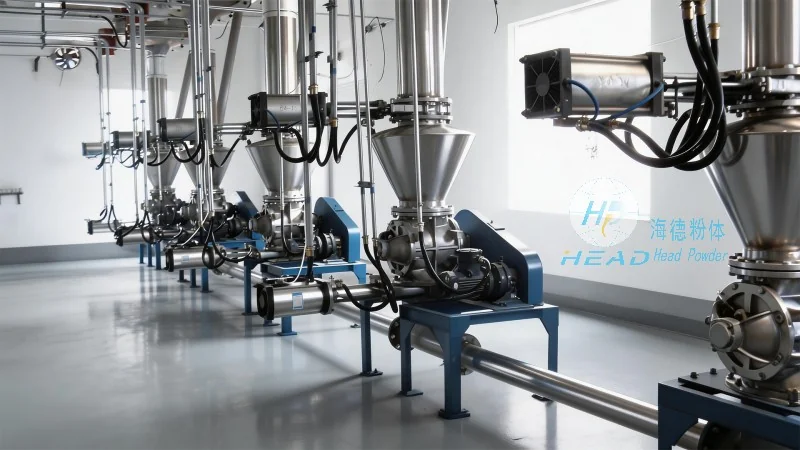
Material feeders, such as rotary valves or screw feeders, control the flow of mineral sand into the conveying line, ensuring a consistent and controlled feed rate. These components work together to create a seamless conveying process that minimizes downtime and maximizes operational efficiency. The use of high-quality materials and robust construction in these systems ensures long-term durability and low maintenance costs.
Application Examples and Case Studies
Shandong HeadPowder Engineering Co., Ltd., a leading provider of mineral processing equipment, has successfully implemented pneumatic conveying systems for various mineral sand applications. For instance, in a titanium dioxide production facility, their system efficiently transported ilmenite ore from the storage silo to the grinding and processing units. The system's ability to handle abrasive mineral sands without causing wear to the equipment components resulted in reduced maintenance costs and extended equipment life.
In another application, a ceramics manufacturer utilized a pneumatic conveying system to transport zircon sand from the mining site to the production plant. The system's flexibility allowed for easy integration with existing production lines, and its precise control over material flow ensured consistent product quality. The project demonstrated the effectiveness of pneumatic conveying in improving operational efficiency and reducing production costs.
Conclusion
Pneumatic conveying systems represent a significant advancement in mineral sand transportation technology, offering numerous advantages over traditional mechanical methods. By eliminating material degradation, providing layout flexibility, and enabling precise control over the conveying process, these systems enhance the overall efficiency and profitability of mineral sand processing operations. As the demand for mineral sands continues to grow, the adoption of advanced pneumatic conveying systems will become increasingly important for companies seeking to maintain a competitive edge in the industry.




