For industries dealing with sand particle transport, selecting the right technology is crucial for optimizing operational efficiency and maintaining a clean working environment. Pneumatic conveying stands out as a leading solution, offering a combination of efficiency, cleanliness, and versatility. This article delves into the principles and applications of pneumatic conveying systems, specifically tailored for sand particle transport, and highlights how companies like Shandong HeadPowder Engineering Co., Ltd. leverage this technology to enhance performance in various industrial settings.
Understanding Pneumatic Conveying for Sand Particle Transport
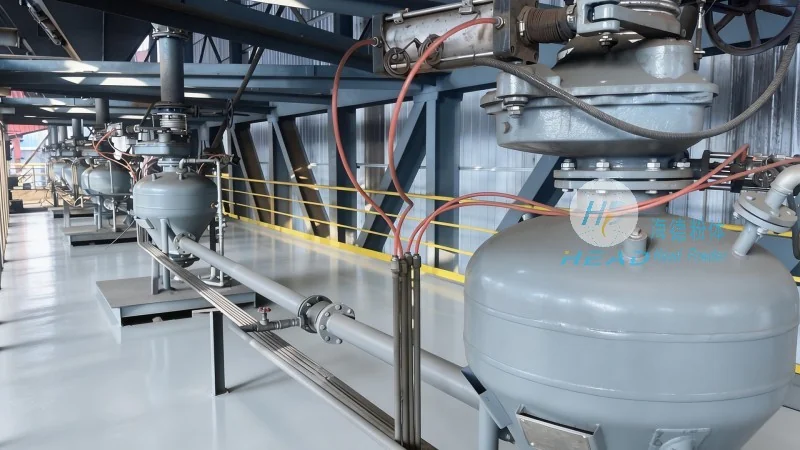
Pneumatic conveying systems utilize air or gas to transport bulk materials like sand particles through a pipeline network. Unlike traditional methods such as belt conveyors or bucket elevators, pneumatic systems eliminate the need for physical contact between the material and the conveying equipment, reducing wear and tear and minimizing the risk of contamination. This makes them ideal for applications where maintaining the purity of the sand is critical, such as in construction, mining, and manufacturing processes.
The Advantages of Pneumatic Conveying in Sand Handling
One of the primary benefits of pneumatic conveying for sand particle transport is its ability to achieve high throughput rates while maintaining a clean and dust-free environment. The technology allows for the continuous movement of large volumes of sand with minimal human intervention, which is particularly advantageous in high-volume production lines. Additionally, pneumatic systems can handle a wide range of sand types, including fine, coarse, and mixed particles, without the need for pre-processing or additional equipment. This versatility makes them adaptable to various industrial needs, from small-scale operations to large-scale mining and construction projects.
Key Components of Pneumatic Conveying Systems for Sand
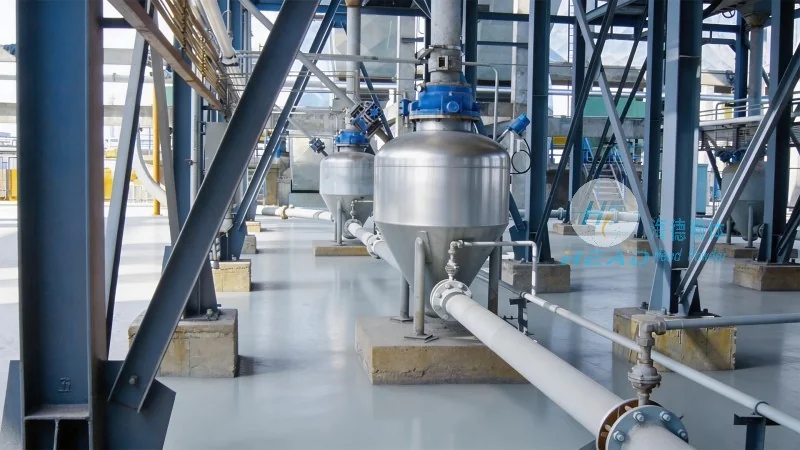
At the core of any pneumatic conveying system are several key components that work in tandem to ensure efficient sand particle transport. These include the air compressor, which generates the necessary pressure to move the material; the hopper or feeder, which stores and dispenses the sand; the pipeline network, which transports the sand and air mixture; and the receiver or discharge unit, which collects the sand at the destination. Each component is designed to work together seamlessly, optimizing the overall performance of the system. For instance, the air compressor must be capable of delivering sufficient pressure to overcome the resistance of the pipeline and the weight of the sand particles, while the hopper must be equipped with a reliable feeding mechanism to prevent blockages and ensure a consistent flow.
Applications of Pneumatic Conveying in Sand Industries
Pneumatic conveying systems are widely used in various industries that rely on sand particle transport. In the construction industry, for example, these systems are used to transport sand from storage silos to mixing plants or job sites, ensuring a steady supply of material without the need for manual handling. In mining operations, pneumatic conveying is employed to transport sand from processing plants to storage facilities or for further processing, reducing the risk of dust exposure and improving safety. Similarly, in manufacturing processes that involve sand as a raw material, such as foundries or glass production, pneumatic systems help maintain a clean and controlled environment, which is essential for producing high-quality products.
How Shandong HeadPowder Engineering Co., Ltd. Enhances Pneumatic Conveying Solutions
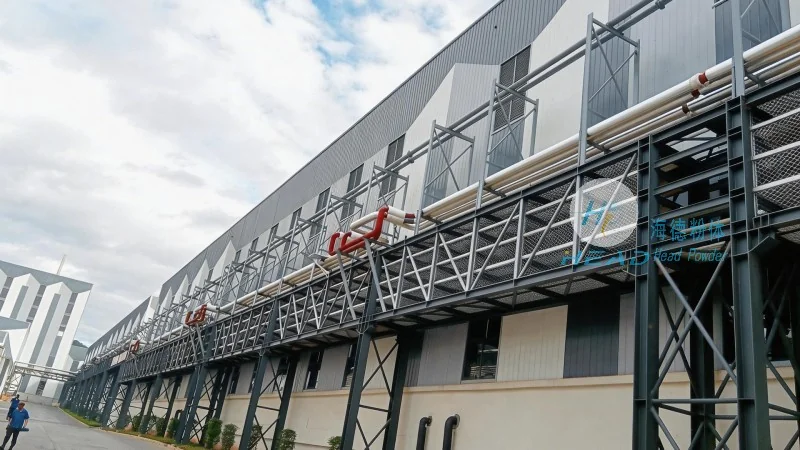
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing customized systems tailored to the specific needs of their clients. With years of experience in the industry, the company has developed a deep understanding of the challenges faced by sand handling operations and has developed innovative solutions to address them. By leveraging advanced technology and engineering expertise, HeadPowder ensures that their pneumatic conveying systems are not only efficient but also reliable and durable. The company’s commitment to quality and customer satisfaction has made them a trusted partner for businesses looking to improve their sand particle transport processes. Whether it's a new installation or an upgrade to an existing system, HeadPowder provides comprehensive support, from initial design and consultation to installation and maintenance, ensuring that clients achieve optimal performance and cost savings.
Conclusion: The Future of Sand Particle Transport with Pneumatic Conveying
As industries continue to seek more efficient and sustainable ways to handle sand particles, pneumatic conveying technology remains a top choice. Its ability to deliver high throughput rates, maintain cleanliness, and adapt to various applications makes it an indispensable tool for modern industrial operations. With companies like Shandong HeadPowder Engineering Co., Ltd. leading the way in developing advanced pneumatic conveying systems, the future of sand particle transport looks promising. By investing in reliable and efficient pneumatic conveying solutions, businesses can enhance their operational performance, reduce costs, and ensure a safe and clean working environment for their employees. The combination of technological innovation and expert engineering ensures that pneumatic conveying will continue to play a vital role in the efficient and sustainable handling of sand particles for years to come.




